
Blogs
Our ABS Vacuum Casting Services
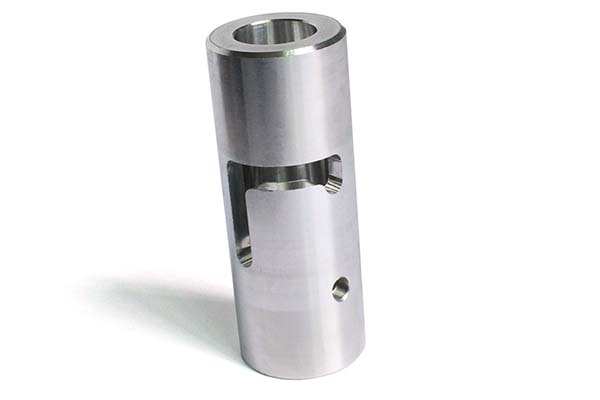
Our ABS Vacuum Casting Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- Unlock unparalleled precision in your manufacturing projects with ABS Vacuum Casting—a cutting-edge technology that combines the durability of ABS material with the flexibility of custom casting.
- At our shop we specialize in Custom Vacuum Casting solutions tailored to your unique project requirements.
- The ABS Vacuum Casting process is a streamlined, repeatable workflow designed to maximize efficiency and minimize defects.
- The success of ABS Vacuum Casting depends on selecting high-quality materials that align with your part’s performance needs.
Our ABS Vacuum Casting Services
Unlock unparalleled precision in your manufacturing projects with ABS Vacuum Casting—a cutting-edge technology that combines the durability of ABS material with the flexibility of custom casting.
Whether you need large-scale production runs or intricate, high-tolerance components, our expertise ensures cost-effectiveness, short lead times, and uncompromising quality. From automotive parts to medical devices, trust our shop to turn your designs into reality.

Our Capabilities: Delivering Customized Excellence
At our shop we specialize in Custom Vacuum Casting solutions tailored to your unique project requirements. Our team’s ABS casting expertise spans industries, from consumer electronics to aerospace, and we pride ourselves on three core strengths: precision, scalability, and quality.
Our Core Capabilities
- Precision casting: We achieve dimensional tolerances as tight as ±0.1mm, ensuring parts align with your exact specifications.
- Large-scale production: Our facilities can handle runs from 10 to 10,000 units, with consistent quality across every batch.
- Quality control: Every component undergoes rigorous testing—including dimensional measurement, impact resistance checks, and surface finish inspections—to meet ISO 9001 and ASTM standards.
| Capability | Specification |
| Custom Vacuum Casting | Tailored mold designs for unique part geometries (e.g., complex undercuts, thin walls). |
| Large-scale production | Monthly capacity of 50,000+ units, with lead times as short as 3–5 days. |
| Quality control | 100% inspection rate for critical components; 99.8% defect-free rate in 2024. |
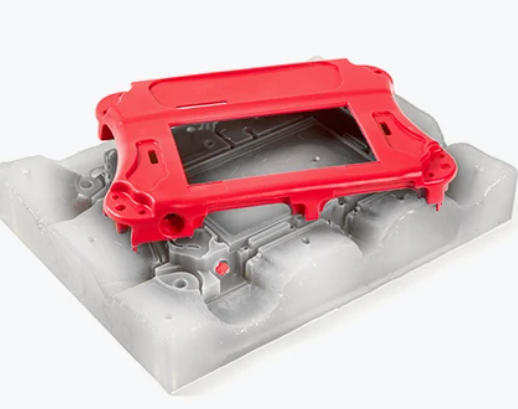
Process: Step-by-Step Workflow of ABS Vacuum Casting
The ABS Vacuum Casting process is a streamlined, repeatable workflow designed to maximize efficiency and minimize defects. Below is a detailed breakdown of each stage:
Step 1: Mold Preparation
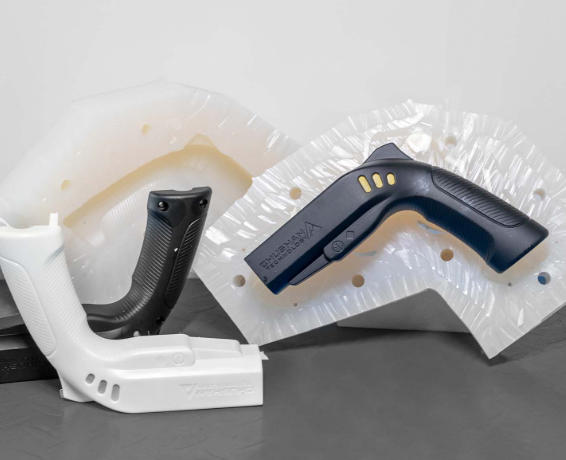
First, we create a master mold (typically from silicone or aluminum) using your 3D model or physical prototype. The mold is engineered to capture every detail—from surface textures to intricate features—and is treated to ensure easy demolding.
Step 2: Resin Mixing
We blend ABS resin with specialized additives (for enhanced flexibility or heat resistance) and catalysts (to control curing time). The mixture is stirred under vacuum to remove air bubbles, a critical step for preventing voids in the final part.
Step 3: Vacuum Chamber Infusion
The mixed resin is poured into the mold, which is then placed in a vacuum chamber. The chamber is sealed, and vacuum pressure (typically -0.95 bar) is applied to draw the resin into every corner of the mold, ensuring complete filling.
Step 4: Curing Process
The mold is heated to 60–80°C to accelerate resin curing. Cure time varies by part thickness (1–4 hours for most components) and is monitored to avoid over-hardening, which can cause brittleness.
Step 5: Demolding & Post-Processing
Once cured, the mold is opened, and the part is removed. Post-processing steps (e.g., trimming excess resin, polishing) are performed to achieve the desired finish.
Materials: Choosing the Right ABS Resin & Additives
The success of ABS Vacuum Casting depends on selecting high-quality materials that align with your part’s performance needs. We source premium ABS resin from trusted resin suppliers and offer a range of additives to enhance functionality.
| Material Type | Purpose |
| ABS resin | Base material providing durability, impact resistance, and machinability. |
| Additives | Improve UV resistance, flame retardancy, or flexibility (e.g., plasticizers). |
| Fillers | Reduce cost or enhance strength (e.g., glass fiber, talc). |
| Catalysts | Control curing speed to ensure uniform hardening. |
Our preferred resin suppliers include Sabic, LG Chem, and Chi Mei Corporation—brands known for consistent quality and compliance with global safety standards (e.g., RoHS, REACH).
Surface Treatment: Enhancing Aesthetics & Performance
After casting, parts can undergo surface treatment to improve appearance, durability, or functionality. We offer a range of finishing options to match your project’s needs:
- Painting: Custom color matching (using Pantone or RAL codes) for parts requiring brand alignment.
- Coating: Protective layers (e.g., clear coat for scratch resistance, anti-static coating for electronics).
- Polishing: Achieve glossy or matte finishes, with surface roughness (Ra) as low as 0.2μm.
- Texture application: Add tactile textures (e.g., leather grain, ribbing) for grip or aesthetic appeal.
| Surface Treatment | Benefit | Example Application |
| Painting | Brand consistency, UV protection | Automotive interior parts |
| Coating | Scratch resistance, chemical resistance | Medical device housings |
| Polishing | High-gloss finish, improved light reflection | Consumer electronics casings |
| Texture application | Enhanced grip, reduced fingerprint visibility | Tool handles, remote controls |
Tolerances: Ensuring Dimensional Accuracy
Dimensional accuracy is critical for parts that need to fit or function with other components. Our ABS Vacuum Casting process achieves industry-leading tolerance levels, supported by advanced measurement tools and strict quality control.
Key Tolerance Specifications
- Linear tolerance: ±0.1mm for parts up to 100mm; ±0.15mm for parts 100–300mm.
- Geometric tolerance: Flatness ≤0.05mm/m, parallelism ≤0.1mm/m.
- Precision measurement: We use coordinate measuring machines (CMMs) and laser scanners to verify dimensions, ensuring compliance with ISO 8015 (geometric tolerancing) and ASME Y14.5 standards.
| Part Size (Length) | Linear Tolerance | Measurement Tool |
| <100mm | ±0.1mm | CMM (accuracy: ±0.005mm) |
| 100–300mm | ±0.15mm | Laser scanner (resolution: 0.02mm) |
| >300mm | ±0.2mm | Optical comparator |
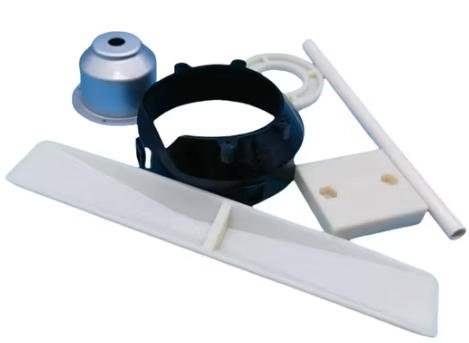
Advantages: Why Choose ABS Vacuum Casting?
ABS Vacuum Casting offers a unique blend of benefits that make it ideal for prototyping and low-to-medium volume production. Here’s how it outperforms other manufacturing methods:
- Cost-effectiveness: No expensive metal tooling—silicone molds cost 70–80% less than aluminum molds, making it ideal for small runs.
- High precision: Captures fine details (down to 0.1mm) and achieves tight tolerances, reducing the need for post-processing.
- Short lead times: Molds can be ready in 2–3 days, and production runs are completed in 3–7 days (vs. 4–6 weeks for injection molding).
- Customization: Easy to adjust resin properties (e.g., color, flexibility) or mold designs for iterative prototyping.
- Durability: ABS parts resist impact, heat, and chemicals, making them suitable for end-use applications (not just prototypes).
| Advantage | ABS Vacuum Casting | Traditional Injection Molding |
| Tooling cost | Low (500–5,000) | High (10,000–100,000+) |
| Lead time | 3–7 days | 4–6 weeks |
| Volume flexibility | 10–10,000 units | 10,000+ units |
| Customization ease | High (quick resin/mold adjustments) | Low (expensive tooling changes) |
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- A model and a drawing that agree
- Material by standard number
- Tolerance only where it mates
- Finish and the faces it applies to
- Quantity and required date
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- process choice
- material
- tolerance band
- finish
- volume
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- A drawing that contradicts the model
- A tolerance with no datum
- A cosmetic callout with no approved sample
- A quote compared against a different scope
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
What to send with the first order
The first order sets the pattern for every order after it. Send a complete package once and the shop files it, and the second order takes a fraction of the time.
- A STEP or native model plus a PDF drawing carrying the same revision letter.
- The material callout by standard number, not by trade name.
- The finish and the exact faces it applies to.
- Any test the part must pass: fit, seal, drop, salt spray, dielectric.
- A contact who can answer a question inside one working day.
Then write down what was agreed. An email that confirms the material, the finish and the date is worth more than a longer purchase order that leaves them open.
When this is the wrong choice
A good supplier tells you when the process does not fit. These are the cases where we say so.
- The volume is so low that setup costs more than the parts are worth.
- The tolerance is tighter than the process can hold without a second operation.
- The geometry cannot be made without a tool feature that will not pay back.
- The material you need is not available in the form the process requires.
- The schedule is shorter than the tooling or setup time, and nobody has said so yet.
None of these are refusals. They are reasons to look at a different route, and the earlier that conversation happens the cheaper it is. The most expensive mistake in manufacturing is a process chosen before the question was understood.
Planning the ramp from prototype to production
The gap between one good part and a thousand identical ones is a plan, not a machine. Three decisions close it.
First, freeze the design. Every change after tooling starts is a re-cut, and re-cuts are where schedules go. Second, decide the inspection level. A prototype is checked by eye; a production part is checked against a report. Third, agree the change process in writing, including who pays for it.
Write the ramp down as dates and owners, not as intentions. A ramp plan with three names and three dates is worth more than a page of good intentions.
What documentation to expect
Paperwork is not bureaucracy when a part fails at the customer. It is the only record of what was agreed. A normal shipment should carry four documents.
- A dimensional report covering every callout on the drawing.
- A material certificate traceable to the heat or lot number.
- A finish or coating certificate where the specification requires one.
- A packing list that matches the carton labels.
If a supplier cannot produce these on request, they are not running a controlled process. Ask for one sample set before you place the first order and you will know exactly what you are buying.
Applications Industry: Where ABS Vacuum Casting Shines
The versatility of ABS Vacuum Casting makes it a top choice across diverse industries. Below are key sectors and their common applications:
- Automotive industry: Interior components (e.g., dashboard trim, door handles), under-hood parts (e.g., sensor housings), and prototyping for new vehicle models.
- Consumer electronics: Phone cases, laptop bezels, speaker enclosures, and charging dock housings—all requiring high aesthetics and dimensional precision.
- Medical devices: Disposable tool housings, diagnostic equipment casings, and orthopedic prototypes—compliant with biocompatibility standards (e.g., ISO 10993).
- Aerospace: Prototypes for cabin interiors, satellite components, and drone parts—where lightweight and high precision are critical.
- Industrial components: Gear housings, pump parts, and conveyor system components—benefiting from ABS’s impact resistance and durability.
Our solution for Our ABS Vacuum Casting Services
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Our ABS Vacuum Casting Services
What is the minimum order quantity (MOQ) for ABS Vacuum Casting?
Our MOQ is just 10 units, making ABS Vacuum Casting ideal for prototyping, small-batch production, or bridge manufacturing (between prototyping and mass production). For orders of 1,000+ units, we offer volume discounts of up to 20%.
How long does it take to produce parts with ABS Vacuum Casting?
Lead times depend on order size and complexity:Mold preparation: 2–3 days (silicone molds) or 5–7 days (aluminum molds).Production: 3–5 days for 10–500 units; 7–10 days for 500–10,000 units.Rush orders (24–48 hour turnaround) are available for critical projects, subject to availability.
Is ABS Vacuum Casting suitable for food-contact or medical applications?
Yes—we offer FDA-compliant ABS resin and biocompatible additives that meet ISO 10993 standards for medical devices. For food-contact parts, we use materials certified to FDA 21 CFR 177.2470. All food/medical parts undergo additional testing to ensure safety and compliance.
What files do you need in order to quote?
A STEP file plus a PDF drawing that carries the same revision letter. The model carries the geometry and the drawing carries the intent. When the two disagree, the shop picks one, and it is never the one you meant.
Does the process work for prototypes as well as production?
Yes, and that is usually the point. Running the prototype on the production process removes a whole class of surprises, because the part you test is made the same way as the part you sell.
What is Our ABS Vacuum Casting Services used for?
Our ABS Vacuum Casting Services turns up wherever the part has to do a real job at a predictable cost: brackets, housings, fixtures, covers and the fittings that hold them together. The honest test is whether the properties match the load and the environment, not whether the material is fashionable.
The short version
Our ABS Vacuum Casting Services rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.