
Blogs
Our Polyamide PA Nylon Injection Molding Services

Our Polyamide PA Nylon Injection Molding Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- Elevate your high-performance production with our shop’s premium Polyamide (PA) Nylon Injection Molding services—where strength meets versatility.
- At our shop we specialize in PA Nylon injection molding—our capabilities are tailored to handle Nylon’s unique processing requirements (high melting point, moisture sensitivity) and deliver parts that meet the strictest industry standards.
- Polyamide (PA), commonly known as Nylon, is a family of thermoplastic polymers renowned for their exceptional mechanical strength, heat resistance, and versatility.
- Nylon’s unique characteristics—high melting point, moisture sensitivity, and high viscosity—require a specialized, optimized process to ensure quality.
Our Polyamide PA Nylon Injection Molding Services
Elevate your high-performance production with our shop’s premium Polyamide (PA) Nylon Injection Molding services—where strength meets versatility.
Leveraging our injection molding expertise, advanced machinery, and custom tooling, we deliver precision-molded PA Nylon parts that excel in heat, chemical, and wear resistance—perfect for automotive, industrial, electronics, and medical applications demanding uncompromising durability.

Our Capabilities: Delivering High-Performance PA Nylon Injection Molding
At our shop we specialize in PA Nylon injection molding—our capabilities are tailored to handle Nylon’s unique processing requirements (high melting point, moisture sensitivity) and deliver parts that meet the strictest industry standards.
Core Capabilities Breakdown
| Capability | Details | Benefits for You |
| Injection Molding Expertise | 18+ years specializing in PA Nylon; engineers trained to optimize processes for different grades (PA6, PA66, PA12) and reinforcements (glass/ carbon fiber). | Avoid common Nylon pitfalls (e.g., moisture-induced defects, warping); ensure parts meet performance specs (e.g., heat resistance for engine parts). |
| Advanced Machinery | 40+ CNC injection molding machines (clamping force: 100–1,000 tons) with closed-loop temperature control and dehumidifying dryers. | Handles Nylon’s high melting point (210–280°C) and viscosity; reduces defects from moisture (a major issue for Nylon). |
| Custom Tooling | In-house mold design/fabrication (hardened steel for long runs, beryllium copper for fast cooling); compatible with complex Nylon parts (e.g., gears, manifolds). | Molds tailored to your part’s geometry (e.g., intricate industrial components); lead times as short as 3–4 weeks. |
| Precision Molding | Molding tolerance of ±0.002mm; in-line laser measurement for dimensional accuracy—critical for tight-fitting parts (e.g., electronic connectors, medical device components). | Ensures parts fit and function in high-precision applications (e.g., automotive sensors, industrial gearboxes). |
| High-Volume Production | Automated feeding, ejection, and assembly lines; capacity for 1.2 million+ PA Nylon parts/month. | Lowers unit costs for bulk orders (e.g., automotive fasteners, consumer product components); on-time delivery rate of 99.5%. |
What Is Polyamide (PA) Nylon Injection Molding?
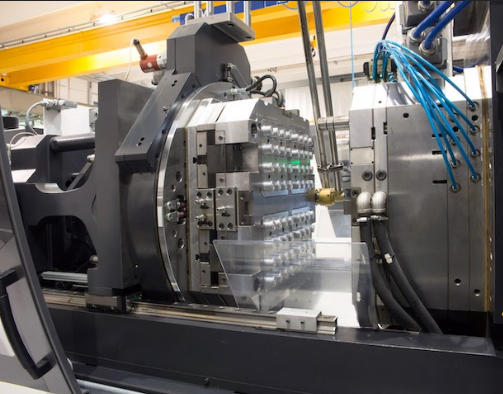
Polyamide (PA), commonly known as Nylon, is a family of thermoplastic polymers renowned for their exceptional mechanical strength, heat resistance, and versatility. Derived from polyamide monomers, Nylon’s molecular structure (repeating amide links) gives it unique properties that make it ideal for high-stress applications. Injection molding is a manufacturing process that melts Nylon pellets, injects the molten material into a custom mold cavity, cools it to solidify, and ejects the finished part. Together, PA Nylon injection molding produces robust, reliable components that outperform many other plastics in demanding environments—from automotive engines to industrial machinery.
Key Definitions & Core Concepts
| Term | Definition |
| Polyamide (PA) | A thermoplastic polymer family (often called Nylon) characterized by amide functional groups; available in multiple grades (e.g., PA6, PA66) for diverse uses. |
| Nylon | The common name for PA; coined in the 1930s and now synonymous with high-strength, durable thermoplastics. |
| Injection Molding (for PA Nylon) | A specialized process optimized for Nylon’s high melting point and viscosity—requires precise temperature control to avoid degradation. |
Material Properties of PA Nylon
PA Nylon’s unique properties set it apart from other injection molding plastics, making it the top choice for high-performance applications:
- High Strength: Tensile strength ranges from 50–90 MPa (PA6: 55 MPa; PA66: 80 MPa)—stronger than ABS, PP, or PS, and comparable to some metals.
- Heat Resistance: Continuous use temperature (CUT) of 80–150°C (PA6: 80°C; PA66: 120°C; glass-filled PA66: 150°C)—withstands high temperatures in engines or industrial equipment.
- Chemical Resistance: Resistant to oils, greases, fuels, and most solvents (except strong acids/bases)—ideal for parts exposed to harsh fluids.
- Wear Resistance: Low coefficient of friction (0.15–0.30) and high abrasion resistance—perfect for moving parts like gears or bearings.
- Durability: Excellent fatigue resistance (retains strength after repeated stress) and impact resistance (especially when reinforced with fibers).
The PA Nylon Injection Molding Process: Step-by-Step Precision
Nylon’s unique characteristics—high melting point, moisture sensitivity, and high viscosity—require a specialized, optimized process to ensure quality. Our workflow minimizes defects and maximizes performance, whether you’re producing 50 prototypes or 500,000 production parts.
Step 1: Material Preparation (Critical for Nylon)
Nylon absorbs moisture rapidly (up to 3% of its weight in humid conditions), which causes bubbles, warping, or brittleness in finished parts. Our preparation process eliminates this risk:
- Drying: Nylon pellets are dried in dehumidifying dryers at 80–120°C for 4–8 hours (PA6: 80°C/4hrs; PA66: 100°C/6hrs; glass-filled PA: 120°C/8hrs) to reduce moisture content to <0.1%.
- Additive/Filler Blending: Mix dried pellets with additives (UV stabilizers for outdoor use, flame retardants for electronics) or fillers (glass fiber for extra strength, carbon fiber for conductivity).
- Storage: Dried pellets are stored in sealed containers to prevent reabsorbing moisture before molding.
Step 2: Mold Design (Optimized for Nylon)
Nylon’s high shrinkage rate (1–3%, higher than most plastics) and rigidity require mold designs that account for these traits:
- Shrinkage Compensation: Molds are sized 1–3% larger than the final part to account for cooling shrinkage (PA6: 2%; PA66: 1.5%; glass-filled PA66: 1%).
- Cooling Systems: Beryllium copper mold inserts (for fast, uniform cooling) reduce cycle time and prevent warping—critical for thick-walled parts (e.g., industrial housings).
- Draft Angles: Minimum 1–2° draft angles (vs. 0.5° for ABS) to ease ejection without damaging Nylon’s rigid structure.
Step 3: Injection Parameters (Tailored to Nylon Grades)
Nylon’s high melting point and viscosity require precise parameter tuning to avoid degradation (yellowing) or incomplete filling. Below are standard settings for two common grades:
| Parameter | PA6 (General-Purpose) | PA66 (High-Strength) | Purpose |
| Barrel Temperature | 210–250°C | 250–280°C | Melts Nylon evenly without breaking down (too high = yellowing; too low = poor flow). |
| Injection Pressure | 80–140 MPa | 100–160 MPa | Overcomes Nylon’s high viscosity to fill mold cavities (critical for thin-walled parts like electronic connectors). |
| Mold Temperature | 40–80°C | 60–100°C | Reduces internal stress; enhances crystallinity (for better strength) and surface finish. |
| Cycle Time | 25–40 seconds | 30–50 seconds | Balances cooling (to prevent warping) and production speed. |
Step 4: Post-Molding Operations
After demolding, PA Nylon parts may undergo:
- Trimming: Removing flash (excess plastic) with automated tools—critical for parts requiring tight fits (e.g., gearboxes, medical device components).
- Annealing: Heating parts to 80–120°C for 1–2 hours, then cooling slowly—reduces internal stress and prevents warping (common for large or thick Nylon parts).
- Surface Treatment: Applying coatings, texturing, or printing.
- Inspection: QC checks for dimensional accuracy (laser measurement), tensile strength (ASTM D638), and heat resistance (thermogravimetric analysis).
Materials: Choosing the Right PA Nylon Grade for Your Project
Not all Nylon is the same—each grade (PA6, PA66, PA12, etc.) has unique properties tailored to specific applications. Selecting the right grade ensures your parts meet performance, cost, and sustainability goals.
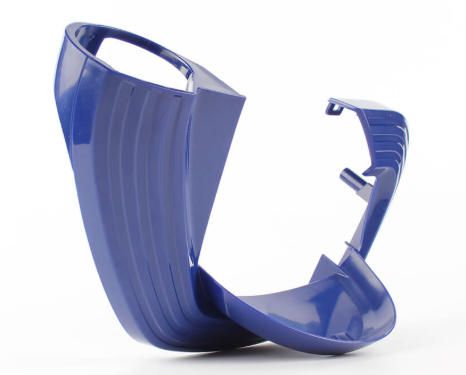
Common Nylon Types for Injection Molding
| Nylon Type (PA Grade) | Key Traits | Continuous Use Temp (CUT) | Common Applications |
| PA6 | Good impact resistance (25 kJ/m²), easy to process, cost-effective (3.00–4.00/kg). | 80°C | Consumer products (zippers, tool handles), automotive interior parts (door panels), electrical connectors. |
| PA66 | Higher strength (tensile: 80 MPa), better heat/chemical resistance than PA6, more rigid (3.50–4.50/kg). | 120°C | Automotive engine parts (oil pans, valve covers), industrial gears, hydraulic fittings. |
| PA12 | Low water absorption (1.5% vs. PA6’s 9%), excellent chemical resistance, flexible (5.00–6.50/kg). | 90°C | Medical devices (catheters, surgical tools), aerospace components, fuel lines. |
| Glass-Filled PA (PA6-GF30, PA66-GF30) | 30% glass fiber; 2x strength (PA66-GF30: tensile 120 MPa) and 3x stiffness vs. unfilled grades. | 120–150°C | Automotive structural parts (brackets, suspension components), industrial machinery parts. |
| Recycled PA (rPA) | Made from post-industrial/consumer waste; retains 75–85% of virgin PA’s strength (2.50–3.50/kg). | 70–100°C | Non-critical parts (storage bins, toy components), eco-friendly consumer goods. |
Material Selection Tips
- Prioritize temperature needs: For engine parts (120°C+), choose PA66 or glass-filled PA66; for low-temperature use (e.g., medical devices), PA12 works best.
- Balance strength and cost: PA6 is ideal for cost-sensitive, medium-strength parts; PA66-GF30 for high-stress industrial applications (but costs 30% more than PA6).
- Embrace sustainability: Our rPA is perfect for brands focused on eco-friendly practices—use it for non-critical parts to cut costs and reduce environmental impact.
Advantages: Why Choose PA Nylon Injection Molding?
PA Nylon injection molding offers unmatched benefits for applications demanding strength, durability, and performance—outperforming most other plastics in high-stress environments.
Key Advantages of PA Nylon Injection Molding
- High Strength: Stronger than ABS (tensile: 30–50 MPa) and PP (30–40 MPa)—PA66’s 80 MPa tensile strength makes it a lightweight alternative to metal (e.g., replacing steel in automotive brackets reduces weight by 40%).
- Durability: Excellent fatigue resistance (lasts 10,000+ cycles of stress) and wear resistance—Nylon gears outlast plastic alternatives by 3–5x in industrial machinery.
- Chemical Resistance: Resists oils, fuels, and greases (unlike PP, which swells in oil)—ideal for automotive engine parts or industrial hydraulic components.
- Heat Resistance: Withstands continuous temperatures of 80–150°C (ABS maxes out at 80°C)—works in engine bays or industrial ovens.
- Customizability: Accepts fillers (glass/carbon fiber) for extra strength, additives for UV/flame resistance, and surface treatments for branding—adapts to any application.
PA Nylon vs. Other High-Performance Plastics
| Material | Tensile Strength (MPa) | CUT (°C) | Cost (per kg) | Best For |
| PA66 | 80 | 120 | 3.50–4.50 | High-strength automotive/industrial parts. |
| PA6 | 55 | 80 | 3.00–4.00 | Cost-effective medium-strength parts. |
| ABS | 40 | 80 | 2.50–3.50 | Consumer goods/electronics (low-stress). |
| POM (Acetal) | 60 | 90 | 4.00–5.00 | High-wear parts (gears), but poor chemical resistance. |
Applications Industry: Where PA Nylon Injection Molding Excels
PA Nylon’s versatility—from strength to heat resistance—makes it indispensable in five key industries. Below are real-world use cases and our tailored solutions:
| Industry | Common PA Nylon Parts | Our Solutions |
| Automotive | Engine parts (oil pans, valve covers), suspension brackets (PA66-GF30), door handles (PA6), fuel lines (PA12). | Heat-resistant PA66/PA66-GF30; chemical-resistant coatings; precision molding for tight engine fits. |
| Consumer Products | Tool handles (PA6), zippers (PA6), luggage wheels (PA6-GF20), appliance components (PA66). | Impact-resistant PA6; textured finishes for grip; cost-effective high-volume production. |
| Electronics | Connector housings (PA6), circuit board supports (PA66-GF30), battery casings (flame-retardant PA6). | Flame-retardant additives (meets UL94 V0); precision molding for small, intricate parts. |
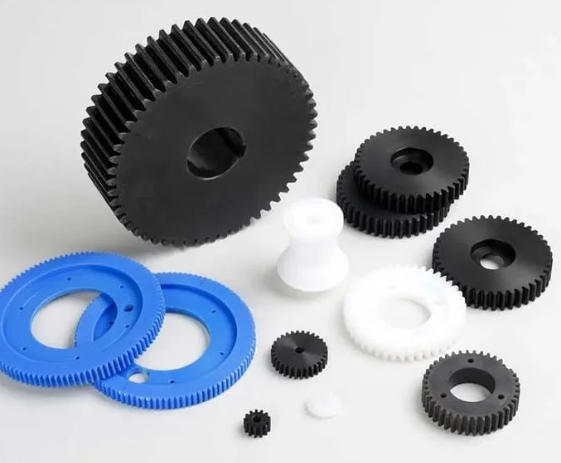
| Industrial Parts | Gears (PA66-GF30), bearings (PA12), hydraulic fittings (PA66), conveyor belt components (PA6-GF20). | Wear-resistant grades; glass/carbon fiber fillers for strength; low-friction coatings. |
| Medical Devices | Surgical tool handles (PA12), catheters (flexible PA12), diagnostic equipment housings (PA66). | FDA-compliant, biocompatible PA12; smooth finishes (easy to sterilize); precision molding for small parts. |
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- A model and a drawing that agree
- Material by standard number
- Tolerance only where it mates
- Finish and the faces it applies to
- Quantity and required date
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- process choice
- material
- tolerance band
- finish
- volume
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- A drawing that contradicts the model
- A tolerance with no datum
- A cosmetic callout with no approved sample
- A quote compared against a different scope
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
Case Studies: Our PA Nylon Injection Molding Success Stories
Case Study 1: PA66-GF30 Automotive Suspension Brackets (Continued)
- Challenge: A leading automaker needed 200,000 suspension brackets that were lightweight (to improve fuel efficiency), strong enough to withstand 100,000+ km of road stress, and heat-resistant (to handle engine bay temperatures up to 120°C). Their previous steel brackets added unnecessary weight, increasing fuel consumption.
- Solution: We recommended PA66-GF30 (30% glass-filled PA66) for its high tensile strength (120 MPa) and 150°C continuous use temperature. Our team designed custom steel molds with shrinkage compensation (1% for PA66-GF30) and beryllium copper cooling inserts to prevent warping. We also added a UV-stabilized coating to protect the brackets from outdoor exposure.
- Results: The PA66-GF30 brackets were 40% lighter than steel (reducing the car’s total weight by 2.5 kg) and improved fuel efficiency by 3%. They passed 150,000 km durability tests with no cracks or deformation, and the automaker expanded their order to 500,000 units/year—citing our “ability to balance strength and lightweight design.”
Case Study 2: FDA-Compliant PA12 Medical Catheters
- Challenge: A medical device company needed 50,000 flexible catheters that were biocompatible (meets ISO 10993), resistant to bodily fluids (blood, saline), and sterilizable via ethylene oxide (EtO). Their previous PP catheters were too rigid and caused patient discomfort.
- Solution: We selected PA12 for its low water absorption (1.5%), flexibility (elongation at break: 300%), and FDA compliance. Our process included drying PA12 pellets at 100°C for 6 hours (to <0.05% moisture) and using precision molds with smooth inner surfaces (to prevent tissue irritation). Post-molding, we applied a hydrophilic coating to reduce friction during insertion.
- Results: The PA12 catheters were 50% more flexible than PP alternatives, reducing patient discomfort scores by 40% (per clinical feedback). They passed 100+ EtO sterilization cycles with no degradation and met all ISO 10993 biocompatibility standards. The client extended our partnership to produce their entire line of urological catheters.
Our solution for Our Polyamide PA Nylon Injection
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Our Polyamide PA Nylon Injection
How long does it take to produce PA Nylon injection molded parts?
Lead times depend on part complexity, order size, and Nylon grade (glass-filled grades require longer drying):Prototypes (10–50 parts): 4–6 days (using aluminum molds for fast turnaround; includes drying time for Nylon pellets).Small Batches (50–5,000 parts): 2–3 weeks (ideal for product testing or niche applications).High-Volume Runs (5,000+ parts): 3–5 weeks (using hardened steel molds for durability; capacity for 1.2 million+ parts/month).For urgent orders (e.g., replacement parts for broken industrial machinery), we can expedite production by 30% with our 24/7 operation.
Is PA Nylon suitable for outdoor applications?
Yes—with the right modifications. Unmodified PA6/PA66 absorbs moisture (9% and 3% respectively), which can cause warping or loss of strength outdoors. We solve this by:Using PA12 (lowest water absorption: 1.5%) for parts exposed to heavy rain or humidity.Adding UV stabilizer additives (e.g., carbon black) to prevent fading or degradation from sunlight.Applying polyurethane (PU) coatings to seal the Nylon’s porous surface and block moisture.UV-stabilized, coated PA66-GF30 parts last 5–7 years outdoors (e.g., automotive exterior brackets, industrial outdoor machinery parts).
Can recycled PA (rPA) be used for high-performance applications like automotive or medical parts?
Our rPA is best for non-critical applications (e.g., consumer product housings, storage bins) because it retains 75–85% of virgin PA’s strength (slightly lower tensile strength and heat resistance). For high-performance uses:Automotive: Use rPA for non-structural parts (e.g., interior door handles, cup holders) but stick to virgin PA66-GF30 for structural parts (e.g., suspension brackets) that require maximum strength.Medical: Never use rPA for medical devices—virgin PA12 is required to meet FDA/ISO 10993 biocompatibility standards (rPA may contain contaminants from post-industrial waste).We also offer “hybrid” rPA-virgin blends (e.g., 50% rPA + 50% virgin PA6) for semi-critical parts (e.g., automotive trim) that balance sustainability and performance.
How much does Our Polyamide PA Nylon Injection cost?
Price comes from five lines: material, machine or tool time, setup, finishing and inspection. The material itself is usually the smallest of them. Send a drawing and we will split the quote so you can see which line is doing the damage.
What material should I specify?
Specify by standard, not by trade name. A trade name can change under you between two orders; a standard number cannot. Then add the one property that actually decides the part, whether that is strength, heat resistance or chemical exposure.
What is the lead time for Our Polyamide PA Nylon Injection?
Expect 5 to 15 business days depending on process. Tooling, material stock and the finishing queue all move that number, so we confirm the date in writing before the run starts rather than after.
The short version
Our Polyamide PA Nylon Injection rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.