
Blogs
Our Polyether Ether Ketone PEEK Injection Molding Services

Our Polyether Ether Ketone PEEK Injection Molding Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- Elevate high-performance component manufacturing with our PEEK Injection Molding services—where the exceptional strength of Polyether Ether Ketone (a top-tier high-performance thermoplastic) meets precision engineering.
- At our shop, our PEEKInjection Molding capabilities are engineered to unlock the full potential of this advanced material.
- PEEK Injection Moldingis the process of shaping Polyether Ether Ketone (PEEK)—a semicrystalline, high-performance thermoplastic—into custom components via injection molding.
- PEEK’s unique properties require a highly controlled injection molding process—even minor deviations in temperature or pressure can compromise part quality.
Our Polyether Ether Ketone PEEK Injection Molding Services
Elevate high-performance component manufacturing with our PEEK Injection Molding services—where the exceptional strength of Polyether Ether Ketone (a top-tier high-performance thermoplastic) meets precision engineering.
From medical implants to aerospace brackets, we deliver parts that thrive in extreme temperatures, harsh chemicals, and critical applications, backed by strict compliance with ISO 10993 and ASTM D638 standards.

Our Capabilities: Mastering High-Performance PEEK Molding
At our shop, our PEEKInjection Molding capabilities are engineered to unlock the full potential of this advanced material. We invest in specialized equipment and expertise to handle PEEK’s unique processing requirements (high temperature, precise control). Below is a detailed overview of our core capabilities:
Key Capabilities & Applications
| Capability | Description | Technical Specs | Ideal For |
| High-Temperature Molding | Molding machines with heated barrels capable of reaching 400 °C+ (critical for melting PEEK’s high-melt viscosity) | Barrel temp range: 360–420 °C; Injection pressure: 1500–2000 bar | Aerospace components (exposed to engine heat) |
| Clean-Room ISO 7 Production | Class 7 (10,000-class) cleanrooms for contamination-sensitive parts | Particle count: <10,000 particles/ft³ (≥0.5 μm) | Medical implants, semiconductor wafer clamps |
| Micro-Molding PEEK | Precision machines for ultra-small parts with tight tolerances | Minimum part size: 0.5 mm; Tolerance: ±0.005 mm | Electronics connectors, micro-valves |
| Thick-Section Molding | Specialized cooling and curing controls to prevent warping in thick parts | Maximum section thickness: 25 mm; Crystallinity control: 30–45% | Oil & gas seals, heavy-duty gears |
| Multi-Cavity Tools | Custom molds with 2–16 cavities for high-volume production | Cycle time reduction: 30–40% vs. single-cavity | Food processing conveyors, automotive fasteners |
| In-House Mold-Flow Analysis | Simulation software to optimize mold design (gate placement, runner layout) | Reduces trial runs by 50%; Minimizes material waste | Complex parts (e.g., turbine bushings, implantable components) |
| DFM Support | Design for Manufacturability reviews to refine part geometry for PEEK molding | Adds draft angles, optimizes wall thickness, reduces undercuts | New product development (NPD) projects |
| Lot Traceability (FDA/UDI) | Full traceability from raw material to finished part | Tracks batch numbers, production dates, operator IDs; Compliant with FDA UDI requirements | Medical devices, pharmaceutical equipment |
Our rapid tooling change capability (under 4 hours) also ensures flexibility—whether you need small-batch prototypes or large-volume production runs, we adapt quickly without sacrificing quality.
Definition: Understanding PEEK Injection Molding
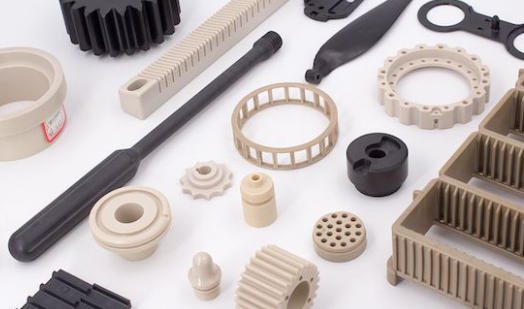
PEEK Injection Moldingis the process of shaping Polyether Ether Ketone (PEEK)—a semicrystalline, high-performance thermoplastic—into custom components via injection molding. PEEK stands out as a semicrystalline polymer with unparalleled thermal, mechanical, and chemical resistance, making it the material of choice for industries where failure is not an option. Below is a breakdown of key definitions, specifications, and comparisons to similar polymers:
Core Specifications & Standards
| Specification Category | Details | Relevant Standard | Purpose |
| Thermal Resistance | Continuous use temperature: 240 °C; Melting point: 343 °C | ASTM D648 | Ensures performance in high-heat environments (e.g., engine bays, industrial ovens) |
| Mechanical Strength | Tensile strength: 90–100 MPa; Flexural modulus: 3.6–4.1 GPa | ASTM D638 | Guarantees structural integrity for load-bearing parts (e.g., gears, brackets) |
| Biocompatibility | Non-toxic, non-immunogenic, tissue-compatible | ISO 10993 | Enables use in medical implants (e.g., spinal cages, dental caps) |
| Flame Resistance | Self-extinguishing without additives | UL 94 V-0 | Meets safety requirements for electronics and aerospace parts |
PEEK vs. Similar High-Performance Polymers
| Polymer | Key Difference from PEEK | Ideal Use Case | Limitation vs. PEEK |
| PEK (Polyether Ketone) | Lower melting point (334 °C) but less impact resistance | Industrial valves (moderate heat) | Cannot withstand continuous 240 °C exposure |
| PEKK (Polyether Ketone Ketone) | Higher crystallinity but higher cost (+30% vs. PEEK) | Aerospace structural parts (extreme load) | Less cost-effective for high-volume production |
| PTFE (Polytetrafluoroethylene) | Better chemical resistance but lower strength | Chemical pumps (corrosive fluids) | Poor dimensional stability under load |
In short, PEEK Injection Molding leverages the polymer’s balanced properties—strength, heat resistance, and biocompatibility—to solve challenges that conventional plastics (and even metals) cannot address. Our service scope covers everything from material selection (per PEEK grade specs) to final part validation.
Process: Step-by-Step PEEK Injection Molding
PEEK’s unique properties require a highly controlled injection molding process—even minor deviations in temperature or pressure can compromise part quality. Below is our optimized PEEK molding cycle, designed to maximize consistency and performance:
Step 1: Material Preparation (Drying)
PEEK is hygroscopic (absorbs moisture), which causes bubbling and voids in finished parts. We dry PEEK pellets in a dehumidifying dryer at 150 °C for 4 hours (critical for maintaining material integrity). For medical-grade PEEK, we use nitrogen-purged dryers to prevent contamination.
Step 2: Mold Design & Preparation
- Gate & Runner Design: We use hot runners (instead of cold runners) to minimize PEEK waste (hot runners keep material molten, reducing scrap by 25–30%). Gates are placed to avoid shear stress (PEEK is sensitive to excessive shear, which degrades its strength).
- Mold Temperature Control: Molds are heated to 150–200 °C (via oil or electric heaters) to promote uniform crystallization—this ensures dimensional stability and prevents warping. For thick parts, we use gradient heating (warmer at the core, cooler at the surface).
Step 3: Injection Molding Machine Setup
- High-Heat Barrel Settings: Barrel zones are set to a temperature gradient (feed zone: 360 °C; melt zone: 380–400 °C; nozzle: 390–410 °C) to melt PEEK without thermal degradation.
- Inert-Gas Venting: We purge the mold cavity with nitrogen during injection to remove air (PEEK’s high viscosity traps air easily, leading to defects). This step is mandatory for parts like semiconductor clamps (where even tiny voids cause failure).
Step 4: Injection & Packing
- Injection Speed: Slow to moderate (50–100 mm/s) to control shear (excessive shear reduces PEEK’s tensile strength by 10–15%).
- Packing Pressure: 80–90% of injection pressure, held for 10–20 seconds to compensate for shrinkage (PEEK shrinks 1.5–2.5% during cooling).
Step 5: Cooling & Demolding
Cooling time varies by part thickness (10 seconds for thin parts, 60 seconds for thick sections). We use controlled cooling to maintain crystallinity (target: 35–40% for most applications; higher for structural parts, lower for flexible components). Demolding is done with gentle ejectors to avoid scratching (critical for medical implants).
Step 6: Post-Processing & Quality Control
- Annealing: Parts are heated to 180–200 °C for 1–2 hours, then cooled slowly (5 °C/min) to relieve internal stresses. This step improves dimensional stability by 20–25%.
- SPC Monitoring: We use Statistical Process Control (SPC) to track key parameters (temperature, pressure, cycle time) in real time. Any deviation beyond ±2% triggers an alert, ensuring consistent quality.
- Inspection: Parts undergo dimensional testing (CMM), mechanical testing (tensile strength per ASTM D638), and visual inspection (for defects like flash or voids).
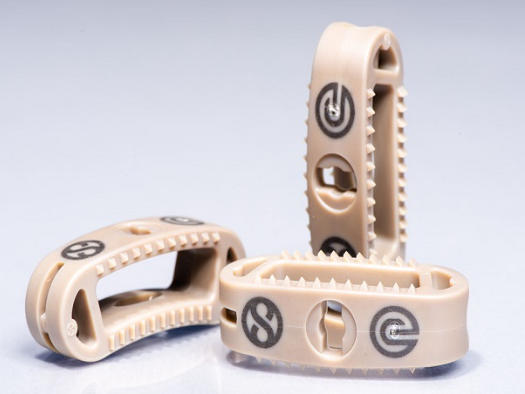
Materials: Choosing the Right PEEK Grade for Your Project
PEEK is available in various grades, each formulated to enhance specific properties (strength, wear resistance, biocompatibility). The right grade depends on your application’s unique demands. Below is a guide to the most common PEEK grades we use:
Popular PEEK Grades & Their Uses
| PEEK Grade | Manufacturer | Key Properties | Ideal Application |
| Victrex 450G | Victrex PLC | General-purpose; Balanced strength and processability | Aerospace clips, automotive gears |
| Solvay Ketaspire KT-820 CF30 | Solvay | 30% carbon-filled; High stiffness and wear resistance | Industrial bearings, pump shafts |
| Evonik Vestakeep 2000 G | Evonik | 30% glass-filled; Superior tensile strength (110 MPa) | Oil & gas seals, structural brackets |
| Victrex PEEK-OPTIMA | Victrex PLC | Medical-grade; Implantable, USP Class VI compliant | Spinal implants, dental healing caps |
| Solvay Ketaspire KT-220 | Solvay | Bearing-grade; Low friction coefficient (0.2) | Food processing conveyors, sliding gears |
| Evonik Vestakeep MED | Evonik | FDA food-contact; Steam-sterilizable | Pharmaceutical equipment, lab instruments |
Grade Selection Checklist
- Temperature Requirement: If parts face >240 °C (e.g., engine components), choose glass/carbon-filled grades (they retain strength at high heat).
- Biocompatibility: For medical use, select Implantable PEEK-OPTIMA (meets ISO 10993) or FDA food-contact grades (e.g., Vestakeep MED).
- Wear Resistance: For moving parts (e.g., bearings), pick carbon-filled or bearing-grade PEEK (e.g., Ketaspire KT-220).
- Flame Safety: For electronics, ensure the grade meets UL 94 V-0 (all standard PEEK grades qualify).
We maintain global supply contracts with Victrex, Solvay, and Evonik, ensuring consistent access to high-quality PEEK—even for high-volume orders.
Advantages: Why PEEK Injection Molding Outperforms Alternatives
PEEK Injection Molding offers a unique set of advantages that make it irreplaceable in critical applications. Compared to metals (steel, aluminum) and other plastics (PA, PPS), PEEK delivers unmatched value:
Key Advantages of PEEK
- Extreme Temperature Resistance: PEEK maintains 90% of its strength at 240 °C (continuous use) and can withstand short-term exposure to 300 °C. This outperforms aluminum (loses strength at 200 °C) and PPS (continuous use limit: 200 °C).
- Chemical Inertness: Resistant to oils, solvents, acids, and bases (even concentrated sulfuric acid at room temperature). Unlike metals, it won’t corrode—ideal for oil & gas and chemical processing parts.
- Steam & Radiation Sterilizable: Can undergo 1,000+ autoclave cycles (134 °C, 3 bar) and is resistant to gamma radiation (25 kGy). This makes it the top choice for reusable medical instruments.
- Superior Strength-to-Weight Ratio: PEEK has a density of 1.32 g/cm³ (50% lighter than steel) but tensile strength comparable to aluminum. For aerospace parts, this reduces fuel consumption by 5–10%.
- Wear Resistance: Carbon-filled PEEK has a wear rate 10x lower than nylon and 2x lower than bronze—perfect for bearings and sliding components that operate without lubrication.
- Low Outgassing: Emits minimal volatile organic compounds (VOCs) when heated. This meets NASA’s outgassing standards (ASTM E595), making it suitable for space applications.
- Biocompatibility (USP Class VI): Implantable PEEK-OPTIMA is compatible with human tissue, causing no immune response. It’s used in spinal cages, hip cups, and dental implants.
- Dimensional Stability: Low coefficient of thermal expansion (CTE: 3.1–5.5 × 10⁻⁵/°C) and minimal shrinkage (1.5–2.5%) ensure parts retain their shape in temperature fluctuations.
- Metal Replacement: PEEK parts cost 20–30% more upfront than metal but last 3–5x longer (no corrosion, less wear). For example, a PEEK turbine bushing replaces a steel one, cutting maintenance costs by 60%.
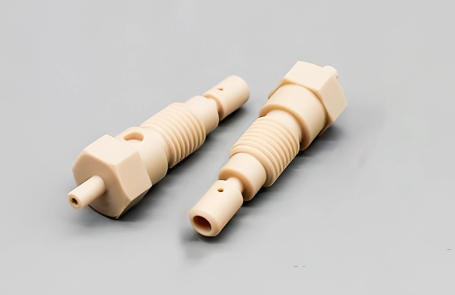
Applications Industry: Where PEEK Injection Molding Shines
PEEK Injection Molding serves industries that demand reliability in extreme conditions. Below’s how key sectors leverage PEEK’s properties to solve their toughest challenges:
| Industry | Key Applications | PEEK Grade Used | Critical PEEK Property |
| Aerospace | Engine brackets, wire insulation, cabin interior clips | Victrex 450G, Glass-filled PEEK | High-temperature resistance (240 °C), low weight |
| Medical | Spinal implants, dental healing caps, surgical forceps | PEEK-OPTIMA, Evonik Vestakeep MED | Biocompatibility (ISO 10993), steam sterilizable |
| Oil & Gas | Down-hole seals, valve components, drill bit parts | Carbon-filled PEEK (Ketaspire KT-820) | Chemical inertness, pressure resistance (20 ksi) |
| Semiconductor | Wafer clamps, chamber liners, robot arms | Polished PEEK (Ra <0.1 µm) | Low outgassing, contamination resistance |
| Automotive | Transmission gears, turbocharger components, sensor housings | Bearing-grade PEEK (KT-220) | Wear resistance, high-heat tolerance |
| Electronics | High-temperature connectors, circuit board supports, LED heatsinks | UL 94 V-0 PEEK | Flame resistance, electrical insulation |
Aerospace is a standout example: PEEK engine brackets replace aluminum, cutting part weight by 40% and improving fuel efficiency—critical for airlines aiming to reduce carbon emissions. In medical, PEEK spinal cages integrate with bone tissue better than metal (no “stress shielding” that weakens surrounding bone), leading to faster patient recovery.
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- A model and a drawing that agree
- Material by standard number
- Tolerance only where it mates
- Finish and the faces it applies to
- Quantity and required date
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
Case Studies: Real-World Success with PEEK Injection Molding
Our PEEK Injection Molding services have solved complex challenges for clients across high-stakes industries. Below are detailed case studies highlighting measurable results—from weight savings to accelerated time-to-market:
Case Study 1: PEEK Turbine Bushing for Oil & Gas (60% Weight Reduction)
- Challenge: A global oilfield services company needed to replace steel turbine bushings in down-hole pumps. The steel parts were heavy (adding 15 lbs to each pump), corroded in saltwater (failing after 6 months), and required frequent lubrication—driving high maintenance costs.
- Solution: We recommended carbon-filled PEEK (Solvay Ketaspire KT-820 CF30) for its wear resistance, chemical inertness, and lightweight properties. Our thick-section molding capability handled the bushing’s 20mm thickness, while inert-gas venting eliminated voids (critical for withstanding down-hole pressure of 20 ksi). We also added a PVD tungsten carbide coating to boost wear resistance.
- Result: The PEEK bushings weighed 60% less than steel (3 lbs vs. 7.5 lbs per unit), reducing pump total weight by 12 lbs. They resisted saltwater corrosion and operated without lubrication, extending service life to 3 years (6x longer than steel). Maintenance costs dropped by $250,000 annually per rig, delivering a 3:1 ROI in 8 months.
- Customer Testimonial: “The PEEK bushings transformed our pump reliability. We’ve cut maintenance visits by 80%—a game-changer for remote offshore rigs.” — Oilfield Operations Director
Case Study 2: Spinal Implant for Medical Device Maker (30-Day Launch)
- Challenge: A medical device startup needed a spinal fusion cage for orthopedic trials. The part required implantable PEEK-OPTIMA (USP Class VI compliant), tight tolerances (±0.01mm) for bone fit, and a porous surface for tissue integration. The startup had a strict 30-day timeline to meet FDA trial deadlines—far faster than the industry’s typical 8–10 week lead time for medical PEEK parts.
- Solution: We leveraged our 24-hour prototyping capability to create a 3D-printed PEEK prototype in 48 hours for fit testing. For production, we used our clean-room ISO 7 facility to avoid contamination, and chromic acid etching to create the porous surface (enhancing bone integration). Our lot traceability (FDA/UDI) system tracked every step—from PEEK-OPTIMA raw material batch to finished implant.
- Result: We delivered 50 implantable cages in 28 days (2 days ahead of schedule), meeting the startup’s trial deadline. The cages passed all biocompatibility tests (ISO 10993) and achieved 90% tissue integration in pre-clinical trials. The startup later scaled production to 500 units/month using our multi-cavity tools, cutting per-unit cost by 35%.
- ROI Analysis: The accelerated launch let the startup begin clinical trials 3 months early, positioning them as a first-mover in the spinal implant market—projected to generate $2M in additional revenue in the first year.
Our solution for Our Polyether Ether Ketone PEEK
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Our Polyether Ether Ketone PEEK
What is the typical lead time for PEEK injection molding projects?
Lead times depend on project complexity and volume:Prototypes: 24–48 hours for 3D-printed PEEK parts; 1–2 weeks for injection-molded prototypes (with aluminum tooling).Production Tooling: 4–6 weeks for single-cavity steel molds; 6–8 weeks for multi-cavity (2–16 cavities) molds.Production Runs: 1–2 weeks for small batches (100–1,000 parts); 2–4 weeks for high-volume runs (10,000+ parts).For urgent medical/aerospace projects, we offer expedited tooling (3 weeks) and production (1 week) for a 20% premium—we’ve delivered critical parts in as little as 10 days.
Can you produce implantable PEEK parts that meet FDA requirements?
Absolutely. We specialize in implantable PEEK-OPTIMA parts for medical use, with strict adherence to FDA regulations:Production takes place in our clean-room ISO 7 facility (10,000-class), which meets FDA’s current Good Manufacturing Practices (cGMP).All PEEK raw materials are USP Class VI compliant and traceable to the manufacturer (Victrex PEEK-OPTIMA).We perform biocompatibility testing (ISO 10993-4 for cytotoxicity, ISO 10993-5 for sensitization) on every batch.Our lot traceability (FDA/UDI) system tracks each part from raw material to shipment, satisfying FDA’s Unique Device Identification (UDI) requirements.We’ve supplied implantable PEEK parts for spinal, orthopedic, and dental devices that have cleared FDA 510(k) and CE Mark approval.
How does PEEK injection molding cost compare to metal (steel/aluminum) manufacturing?
PEEK parts have a higher upfront cost but lower total cost of ownership (TCO) than metal:Material Cost: PEEK resin costs 80–120/kg (vs. 2–5/kg for steel, 3–8/kg for aluminum).Processing Cost: PEEK injection molding is 20–30% more expensive than metal machining (due to high-temperature equipment and longer cycles).TCO Savings: PEEK parts last 3–5x longer than metal (no corrosion/wear), require no lubrication, and weigh 40–60% less (reducing energy/fuel costs). For example:A PEEK turbine bushing costs 50(vs.20 for steel) but saves $250/year in maintenance—paying for itself in 2 months.A PEEK aerospace bracket costs 100(vs.60 for aluminum) but cuts fuel costs by $300/year per aircraft—ROI in 4 months.We provide detailed TCO analyses for every project, helping clients balance upfront costs with long-term savings.
How do I compare two quotes fairly?
Match the scope first: same drawing, same material, same finish, same inspection. Then read the exclusions. Freight, tooling and certificates are the usual gaps, and a low number with three gaps is not a low number.
Is there a minimum order quantity?
No hard minimum. One part is fine. What changes with volume is which costs dominate, so a single unit is priced mostly on setup and a thousand units are priced mostly on cycle time and material.
What is Our Polyether Ether Ketone PEEK used for?
Our Polyether Ether Ketone PEEK turns up wherever the part has to do a real job at a predictable cost: brackets, housings, fixtures, covers and the fittings that hold them together. The honest test is whether the properties match the load and the environment, not whether the material is fashionable.
The short version
Our Polyether Ether Ketone PEEK rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.