
Blogs
Our Polyphenylene Oxide PPO Injection Molding Services

Our Polyphenylene Oxide PPO Injection Molding Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- Elevate your product reliability with our shop’s Polyphenylene Oxide (PPO) Injection Molding services—the premier choice for high-stability, high-performance thermoplastic components.
- our shop’s PPO injection molding capacity is engineered to handle projects of all sizes—from micro-scale medical components to high-volume automotive parts—while maintaining strict quality standards.
- PPOInjection Molding is a specialized manufacturing process that shapes Polyphenylene Oxide (PPO)—a high-performance thermoplastic—and its modified variant (modified PPO, or mPPE) into custom parts via high-pressure injection into precision molds.
- PPO’s high melt viscosity requires careful process control—rushing steps or ignoring temperature limits can lead to warping or incomplete filling.
Our Polyphenylene Oxide PPO Injection Molding Services
Elevate your product reliability with our shop’s Polyphenylene Oxide (PPO) Injection Molding services—the premier choice for high-stability, high-performance thermoplastic components.
From UL 94 V-0 electrical housings to autoclaveable medical trays, we combine micro-precision capabilities, clean-room production, and advanced modified PPO (mPPE) formulations to deliver parts that excel in harsh environments. Backed by ISO 13485/9001 certifications and 24/7 support, we turn your PPO molding challenges into cost-effective, industry-leading solutions.

Our PPO Injection Molding Capabilities: Precision at Every Scale
our shop’s PPO injection molding capacity is engineered to handle projects of all sizes—from micro-scale medical components to high-volume automotive parts—while maintaining strict quality standards. Our facility specializes in overcoming PPO’s unique processing challenges (like high melt viscosity) to deliver consistent, high-quality parts.
Core Capabilities Overview
| Capability | Specification | Ideal Applications |
| Tolerance Control | ±0.01 mm for micro parts; ±0.03 mm for standard components | Water-meter housings, micro-electrical connectors |
| Micro PPO Molding | Parts as small as 0.8 mm (length) with intricate features | Medical device components, telecom micro-pins |
| High-Volume Production | Up to 6 million parts/year (via multi-cavity tooling) | Automotive HVAC valves, consumer electronics frames |
| Clean-Room PPO Service | Class 7 (10,000) and Class 8 (100,000) certified rooms | Medical instrument trays, FDA-compliant fluid manifolds |
| Advanced Molding | 2-shot PPO molding, insert/over-molding (compatible with metals/plastics) | Over-molded connectors, multi-material pump bodies |
| Multi-Cavity PPO Tooling | Up to 32-cavity molds (for small parts like relay blocks) | High-volume electrical components |
What Is PPO Injection Molding?
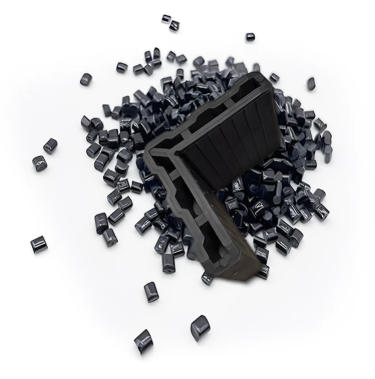
PPOInjection Molding is a specialized manufacturing process that shapes Polyphenylene Oxide (PPO)—a high-performance thermoplastic—and its modified variant (modified PPO, or mPPE) into custom parts via high-pressure injection into precision molds. Unlike many thermoplastics, PPO boasts inherent thermal stability and low moisture absorption, making PPO thermoplastic molding ideal for applications where dimensional consistency and reliability are non-negotiable.
At its core, PPO plastic molding leverages the material’s unique molecular structure: a rigid aromatic backbone that resists heat, chemicals, and warping. Modified PPO (mPPE) enhances these traits further—blending PPO with other polymers (like polystyrene) to improve processability without sacrificing performance. This versatility is why PPO injection molding is trusted across electrical, automotive, and medical industries.
Key Traits of PPO Molding
| Trait | Description | Relevance to Molding |
| Thermoplastic Behavior | Softens at high temps (250–300°C), hardens when cooled—reversible | Enables high-volume production and complex part geometries |
| Low Moisture Absorption | <0.1% water uptake (24hrs at 23°C) | Ensures dimensional stability in humid environments (e.g., HVAC valves) |
| Heat Resistance | Continuous use temp: 120–150°C (up to 200°C short-term) | Ideal for heat-exposed parts (e.g., EV battery insulators) |
| Electrical Insulation | Low dielectric constant (2.5–3.0) | Perfect for electrical housings and telecom components |
The PPO Injection Molding Process: Step-by-Step Excellence
PPO’s high melt viscosity requires careful process control—rushing steps or ignoring temperature limits can lead to warping or incomplete filling. Our optimized workflow ensures every PPO part meets your exact specifications.
Step 1: Resin Preparation
We start with dry PPO resin grades—moisture content must stay <0.05% (PPO absorbs minimal water, but even small amounts cause bubbles). For specialized parts, we blend additives: glass fibers (for strength), flame retardants, or pigments. Glass-filled PPO grades are mixed in a twin-screw extruder to ensure uniform fiber distribution.
Step 2: Screw & Barrel Setup
PPO’s high viscosity demands specialized PPO screw & barrel design:
- Deep feed zones (to avoid shear heating)
- Low compression ratios (2:1 to 2.5:1)
- Hardened barrel liners (to resist abrasion from glass-filled grades)
This setup ensures smooth resin flow without degradation.
Step 3: Injection & Temperature Control
Resin is heated to the PPO melt temperature window (260–300°C) and injected into the mold at 900–1,400 bar pressure. Injection speed is calibrated to part thickness—slower for thin walls (e.g., electrical housing walls) to prevent jetting. We use in-mold cooling for PPO—precision water channels keep mold temp at 60–90°C, reducing PPO molding cycle time to 20–60 seconds (varies by part size).
Step 4: Demolding & Degating
After cooling, parts are demolded gently (PPO is rigid but can crack if forced). We use automated PPO degating technique—laser cutting for small parts (e.g., micro-connectors) or punch tools for larger components—ensuring clean, burr-free edges.
Step 5: Quality Inspection
Every batch undergoes 100% inspection:
- Dimensional checks (via CMM machines)
- PPO mold shrinkage control verification (shrinkage rate: 0.2–0.8%, depending on grade)
Functional tests (e.g., heat resistance at 150°C for 24hrs, electrical insulation checks)
PPO Materials: Formulations for Every Industry Need
The right PPO formulation defines part performance. We offer a wide range of PPO resin grades tailored to industry-specific demands—from flame-retardant electrical parts to FDA-compliant medical devices.
Popular PPO Formulations We Supply
| Formulation Type | Key Properties | Target Applications |
| General-Purpose PPO | Good dimensional stability, cost-effective | Consumer electronics frames, telecom parts |
| FDA-Compliant PPO Compounds | Non-toxic, sterilizable (autoclave/ETO), FDA 21 CFR 177.2420 | Medical instrument trays, fluid handling manifolds |
| Glass-Filled PPO Grades | 40–60% higher tensile strength (80–100 MPa), improved stiffness | Pump bodies, automotive HVAC valves |
| Flame-Retardant PPO Resins | UL 94 V-0 rated (0.8mm thickness), low smoke emission | Electrical housings, EV battery insulators |
| Impact-Modified PPO | High Izod impact strength (20–50 J/m), shatter-resistant | Dishwasher valve bodies, outdoor electrical components |
| Conductive PPO Grades | Surface resistance <10⁶ Ω, anti-static | Electronics frames (ESD protection), sensor housings |
Advantages of PPO: Why It Outperforms Other Thermoplastics
PPO stands out among high-performance thermoplastics for its unbeatable balance of stability, durability, and versatility. Here’s why it’s the top choice for demanding applications:
- PPO Dimensional Stability Benefit: Shrinkage rate of 0.2–0.8% (vs. 1.5–2.5% for nylon), ensuring parts fit perfectly even in temperature-fluctuating environments (e.g., automotive engines).
- PPO Low Moisture Absorption: <0.1% water uptake (vs. 1.5% for ABS), making it ideal for humid settings (e.g., HVAC valves, outdoor telecom parts).
- PPO Electrical Insulation Value: Low dielectric constant (2.5–3.0) and high volume resistivity (10¹⁶ Ω·cm), outperforming PVC for high-voltage electrical housings.
- PPO Heat Resistance Advantage: Continuous use at 120–150°C (vs. 80–100°C for polycarbonate), suitable for EV battery insulators and heat-exposed automotive parts.
- PPO Flame Retardancy Edge: Easily formulated to UL 94 V-0 (0.8mm), critical for electrical components in enclosed spaces (e.g., server rooms).
- PPO Chemical Resistance Plus: Resists oils, greases, and most industrial solvents—perfect for pump bodies and fluid manifolds.
- PPO Colorability & Clarity: Available in clear grades (for sight glasses) or custom colors (via pigmented PPO pellets), with excellent UV stability.
PPO Injection Molding Applications: Across Key Industries
PPO’s versatility makes it indispensable in industries where reliability, stability, and performance are critical. Our clients trust our molding expertise to solve their toughest challenges.
Industry-by-Industry Applications & Solutions
| Industry | Key Applications | Our Molding Solution |
| Electrical | PPO molded electrical housings, relay blocks, EV battery insulators | Flame-retardant PPO (UL 94 V-0), tight tolerances (±0.02 mm) |
| Automotive | PPO automotive HVAC valves, pump bodies, sensor housings | Impact-modified/glass-filled PPO, IATF 16949 compliant |
| Medical | PPO medical device components, instrument trays, fluid manifolds | FDA-compliant PPO, clean-room molding (Class 7) |
| Consumer Electronics | PPO consumer electronics frames, antenna reflectors | Conductive/anti-static PPO, 2-shot molding (for multi-material parts) |
| Industrial | PPO fluid handling manifolds, filter bodies, meter housings | Chemical-resistant/glass-filled PPO, post-mold machining |
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- A model and a drawing that agree
- Material by standard number
- Tolerance only where it mates
- Finish and the faces it applies to
- Quantity and required date
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- process choice
- material
- tolerance band
- finish
- volume
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- A drawing that contradicts the model
- A tolerance with no datum
- A cosmetic callout with no approved sample
- A quote compared against a different scope
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
What to send with the first order
The first order sets the pattern for every order after it. Send a complete package once and the shop files it, and the second order takes a fraction of the time.
- A STEP or native model plus a PDF drawing carrying the same revision letter.
- The material callout by standard number, not by trade name.
- The finish and the exact faces it applies to.
- Any test the part must pass: fit, seal, drop, salt spray, dielectric.
- A contact who can answer a question inside one working day.
Then write down what was agreed. An email that confirms the material, the finish and the date is worth more than a longer purchase order that leaves them open.
When this is the wrong choice
A good supplier tells you when the process does not fit. These are the cases where we say so.
- The volume is so low that setup costs more than the parts are worth.
- The tolerance is tighter than the process can hold without a second operation.
- The geometry cannot be made without a tool feature that will not pay back.
- The material you need is not available in the form the process requires.
- The schedule is shorter than the tooling or setup time, and nobody has said so yet.
None of these are refusals. They are reasons to look at a different route, and the earlier that conversation happens the cheaper it is. The most expensive mistake in manufacturing is a process chosen before the question was understood.
Case Study: UL 94 V-0 PPO Relay Block for an Electrical Manufacturer
A leading electrical supplier needed a UL 94 V-0 PPO relay block that could withstand high voltage (1,000V), resist heat (150°C), and meet strict dimensional standards (±0.02 mm). Their previous part (made from PVC) failed flame tests and warped in high temps.
Our Solution:
- Material Selection: Chose flame-retardant PPO resin (UL 94 V-0 at 0.8mm) with high dielectric strength (25 kV/mm) and low moisture absorption.
- Mold Design: Used a 12-cavity mold with in-mold cooling for PPO—precision water channels ensured uniform cooling, minimizing warpage. Added ejector pins at stress points to prevent cracking.
- Process Optimization: Set melt temp to 280°C, mold temp to 80°C, and injection pressure to 1,100 bar. Used low-shear molding to avoid resin degradation and ensure consistent flame-retardant properties.
Results:
- The relay block passed UL 94 V-0 testing (0.8mm thickness) and 1,000V electrical insulation tests with no failures.
- Dimensional accuracy stayed within ±0.015 mm (exceeding the client’s ±0.02 mm requirement).
- Warpage was reduced by 70% vs. the PVC part—critical for relay fitment.
The client scaled up to 300,000 units/year with our high-volume lines, cutting costs by 18% vs. using PEEK.
Our solution for Our Polyphenylene Oxide PPO Injection
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Our Polyphenylene Oxide PPO Injection
What’s the typical lead time for PPO injection molding parts?
For standard parts (using existing tooling), lead time is 2–4 weeks. For custom parts needing new tooling, it’s 6–8 weeks (including tool design, prototyping, and production). We offer expedited prototyping (3–5 days) for urgent projects.
Can you produce PPO parts that meet both FDA and UL standards?
Yes. We offer FDA-compliant PPO compounds (for medical/ food-contact parts) that can also be formulated to meet UL standards—e.g., UL 94 V-0 for flame retardancy. For example, our PPO medical instrument trays are FDA 21 CFR 177.2420 compliant and UL 94 V-0 rated (for use in hospital electrical rooms).
How do you handle PPO’s high melt viscosity during molding?
We use three key strategies: (1) Specialized PPO screw & barrel design (deep feed zones, low compression ratios) to reduce shear heating and ensure smooth flow; (2) Low-shear molding (slower injection speeds for thin walls) to avoid resin degradation; (3) Optimized melt temperature control (260–300°C, adjusted by grade) to balance flow and part integrity. These steps ensure consistent filling even for complex, thin-walled PPO parts (e.g., micro-electrical connectors).
Does the process work for prototypes as well as production?
Yes, and that is usually the point. Running the prototype on the production process removes a whole class of surprises, because the part you test is made the same way as the part you sell.
Can Our Polyphenylene Oxide PPO Injection be made in small quantities?
Yes, and small quantities are where a good supplier earns the next order. Setup dominates the price at low volume, so the cheapest route is usually the one with the fewest operations, not the cheapest material.
What is the lead time for Our Polyphenylene Oxide PPO Injection?
Expect 5 to 15 business days depending on process. Tooling, material stock and the finishing queue all move that number, so we confirm the date in writing before the run starts rather than after.
The short version
Our Polyphenylene Oxide PPO Injection rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.