
Blogs
Our Polystyrene PS Injection Molding Services

Our Polystyrene PS Injection Molding Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- Elevate your production with our shop’s top-tier Polystyrene (PS) Injection Molding services—where precision meets versatility.
- At our shop, our PS injection molding expertise is built on advanced equipment, skilled engineering, and a focus on solving client challenges—from small-batch custom parts to large-scale production runs.
- Polystyrene (PS) is a widely used thermoplastic polymer made from styrene monomers, celebrated for its clarity, affordability, and ease of processing.
- PS’s unique melting and cooling properties require a optimized process to avoid defects like warping or cloudiness.
Our Polystyrene PS Injection Molding Services
Elevate your production with our shop’s top-tier Polystyrene (PS) Injection Molding services—where precision meets versatility.
Whether you need transparent packaging, lightweight consumer products, or high-volume electronic components, we leverage our injection molding expertise, custom tooling, and strict quality control to deliver cost-effective, customizable PS parts tailored to your industry needs.

Our Capabilities: Delivering Top-Tier PS Injection Molding Solutions
At our shop, our PS injection molding expertise is built on advanced equipment, skilled engineering, and a focus on solving client challenges—from small-batch custom parts to large-scale production runs. We prioritize precision and quality to ensure your PS components meet the highest standards.
Core Capabilities Breakdown
| Capability | Details | Benefits for You |
| Custom Tooling | In-house mold design and fabrication (aluminum for prototypes, hardened steel for long-run PS parts). | Molds tailored to your part’s geometry (e.g., intricate packaging or electronic casings); lead times as short as 2–3 weeks. |
| Precision Molding | CNC-controlled injection machines with ±0.003mm tolerance; in-line vision inspection for dimensional accuracy. | Ideal for small, detailed parts (e.g., medical device components, electronic connectors) that require tight specs. |
| High-Volume Production | 30+ injection molding machines (50–600 tons clamping force) with automated feeding and ejection systems. | Capacity to produce 800,000+ PS parts/month; lower unit costs for bulk orders (e.g., packaging, consumer goods). |
| Quality Control (QC) | In-line checks (for clarity, dimensional accuracy) and post-production testing (impact, heat resistance); ISO 9001 certified. | 99.7% defect-free rate; ensures PS parts meet your industry’s quality standards (e.g., FDA for food packaging). |
What Is Polystyrene (PS) Injection Molding?
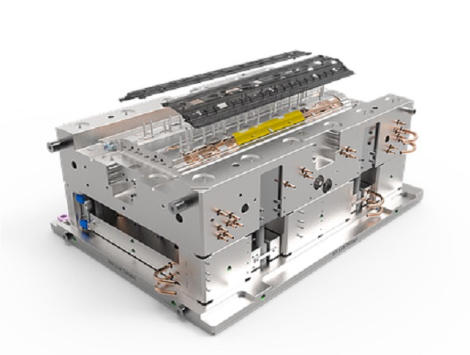
Polystyrene (PS) is a widely used thermoplastic polymer made from styrene monomers, celebrated for its clarity, affordability, and ease of processing. Injection molding is a manufacturing process that melts plastic pellets, injects the molten material into a custom mold cavity, cools it, and ejects the finished part. Combined, PS injection molding produces consistent, high-quality components for diverse sectors, leveraging PS’s unique traits to meet various application demands.
Key Definitions & Process Overview
| Term | Definition |
| Polystyrene (PS) | A thermoplastic with two main forms (rigid and foam); known for clarity, lightweight, and low cost. |
| Injection Molding | A cyclic mass-production process: PS pellets → melted → injected into mold → cooled → ejected (repeats for efficiency). |
| Mold Cavity | The hollow space in a mold that shapes the final PS part; can have 1–128 cavities for high-volume output. |
Material Properties of PS
PS’s distinct properties make it ideal for injection molding. Below are the most critical traits for manufacturers and buyers:
- Clarity and Transparency: Amorphous PS (general-purpose PS) has 90% light transmittance—comparable to glass, making it perfect for visible packaging.
- Density: 1.04–1.06 g/cm³ (lightweight, reducing shipping costs and part weight for consumer goods).
- Melting Point: 140–180°C (low melting temperature, lowering energy consumption during molding).
- Brittleness: Rigid PS is brittle (impact strength: 1.5–2.5 kJ/m²), but can be modified with rubber additives for toughness.
- Ease of Processing: Low viscosity when melted, filling complex mold details easily—ideal for intricate parts.
The PS Injection Molding Process: Step-by-Step Excellence
PS’s unique melting and cooling properties require a optimized process to avoid defects like warping or cloudiness. Our workflow ensures consistent quality while maximizing efficiency.
Step 1: Material Preparation
- Pellet Selection: Choose between general-purpose PS (GPPS, for clarity), high-impact PS (HIPS, for toughness), or foam PS (EPS, for insulation).
- Additive Blending: Mix PS pellets with additives (UV stabilizers for outdoor use, colorants for branded parts, rubber modifiers for impact resistance).
- Drying: PS absorbs minimal moisture, but we dry pellets at 60–70°C for 1–2 hours to prevent surface defects (e.g., bubbles in transparent parts).
Step 2: Mold Design
- Clarity Considerations: Molds for transparent PS parts have polished surfaces to maintain clarity (no scratches or texture that reduces light transmittance).
- Cooling Optimization: Molds include uniform cooling channels to prevent warping—critical for thin-walled PS parts (e.g., packaging).
- Prototype Testing: We 3D-print mold prototypes first to validate design (reduces costly revisions and ensures part functionality).
Step 3: Injection Parameters (Critical for PS)
PS’s low melting point and viscosity require precise parameter tuning. Below are our standard settings for GPPS (the most common PS grade):
| Parameter | Ideal Range for GPPS | Purpose |
| Barrel Temperature | 160–200°C | Melts PS evenly without degradation (higher temps cause yellowing). |
| Injection Pressure | 40–100 MPa | Fills mold cavities completely (critical for intricate details like packaging logos). |
| Cooling Time | 10–25 seconds | Prevents warping; balances speed and part stability (shorter for thin parts). |
Step 4: Post-Molding Operations
After demolding, PS parts may undergo:
- Trimming: Removing excess plastic (flash) with automated tools (critical for clear parts to maintain aesthetics).
- Assembly: Joining parts via adhesives or snap-fits (for complex components like consumer product enclosures).
Inspection: Final QC checks for clarity, dimensional accuracy, and surface quality (100% inspection for medical or food-contact parts).
Materials: Choosing the Right PS for Your Project
Not all PS is the same—selecting the right grade ensures your parts meet performance, cost, and aesthetic goals. We offer a full range of PS materials, plus recycled options.
Types of PS for Injection Molding
| PS Type | Key Traits | Common Applications |
| General-Purpose PS (GPPS) | Clear, rigid, low cost (≈1.20–1.80/kg). | Packaging (food containers, blister packs), electronic casings (remote controls), toys. |
| High-Impact PS (HIPS) | Tough, impact-resistant (impact strength: 10–20 kJ/m²), opaque. | Consumer goods (appliance parts, toy cars), automotive interior trim, medical device housings. |
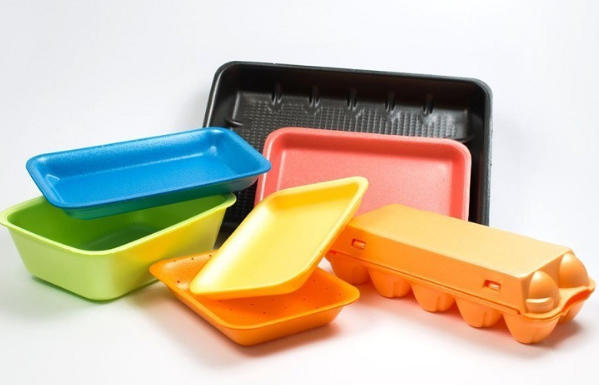
| Expandable PS (EPS) | Foam-like, lightweight (density: 0.015–0.04 g/cm³), excellent insulation. | Packaging (protective inserts for electronics), disposable food containers, construction insulation. |
| Styrene-Acrylonitrile (SAN) | Heat-resistant (up to 90°C), chemical-resistant, clear. | Food packaging (coffee cups), cosmetic containers, medical device components. |
Material Selection Tips
- Prioritize clarity: For visible packaging (e.g., blister packs), choose GPPS or SAN.
- Need toughness?: Opt for HIPS (ideal for parts prone to drops, like toy cars or appliance handles).
Embrace sustainability: Our recycled PS (rPS) is made from post-consumer waste (e.g., old packaging) and retains 85% of the performance of virgin PS—perfect for eco-friendly brands.
Advantages: Why Choose PS Injection Molding?
PS injection molding offers a unique blend of cost savings, aesthetics, and versatility—making it a top choice for manufacturers across industries.
Key Advantages of PS Injection Molding
- Cost-effectiveness: PS is one of the cheapest thermoplastics (GPPS costs 1.20–1.80/kg), and injection molding’s high volume drives unit costs down to 0.05–0.30 per part (ideal for high-volume items like packaging).
- Clarity and Transparency: GPPS has 90% light transmittance—cheaper than glass or acrylic, making it perfect for packaging where product visibility matters (e.g., candy, electronics).
- Customizability: Molds can create complex shapes (e.g., intricate toy parts, custom packaging), and PS accepts additives for color, UV resistance, or toughness.
- Lightweight: PS’s density (1.04–1.06 g/cm³) is 50% less than glass and 30% less than ABS—reducing shipping costs and improving user comfort (e.g., lightweight toy parts).
- Ease of processing: PS melts at low temperatures (saves energy) and has low viscosity (fills small mold details easily)—reducing production time and defects.
PS vs. Other Common Injection Molding Plastics (for Clarity-Critical Applications)
| Material | Cost (per kg) | Light Transmittance | Impact Strength (kJ/m²) | Best For |
| GPPS | 1.20–1.80 | 90% | 1.5–2.5 | Low-cost clear packaging, toys. |
| Acrylic (PMMA) | 2.50–3.50 | 92% | 2.0–3.0 | High-end clear parts (e.g., display cases). |
| PET | 1.80–2.50 | 88% | 5.0–7.0 | Durable clear packaging (e.g., water bottles). |
Applications Industry: Where PS Injection Molding Shines
PS’s versatility—from clarity to toughness—makes it indispensable in five key industries. Below are real-world use cases and our tailored solutions:
| Industry | Common PS Parts | Our Solutions |
| Packaging | Blister packs, food containers, protective inserts (EPS), cosmetic jars. | GPPS for clear packaging; EPS for shock-absorbent inserts; FDA-compliant grades for food contact. |
| Consumer Products | Toy parts, appliance handles (HIPS), remote controls, disposable cutlery. | HIPS for impact-resistant parts; GPPS for colorful, clear toy components; custom tooling for unique shapes. |
| Medical Devices | Disposable syringes (SAN), test tubes, device housings (HIPS). | Sterilizable PS grades; ISO 13485-certified processes; precision molding for small, accurate parts. |
| Automotive | Interior trim (HIPS), cup holders, door panels, speaker grilles. | HIPS for impact resistance; UV-stabilized additives for long-term durability; custom colors to match car interiors. |
| Electronics | Remote control casings (GPPS), laptop bezels (HIPS), LED diffusers. | Precision molding for tight-fitting parts; flame-retardant additives (meets UL94 standards); textured finishes to hide fingerprints. |
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- A model and a drawing that agree
- Material by standard number
- Tolerance only where it mates
- Finish and the faces it applies to
- Quantity and required date
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- process choice
- material
- tolerance band
- finish
- volume
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- A drawing that contradicts the model
- A tolerance with no datum
- A cosmetic callout with no approved sample
- A quote compared against a different scope
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
Case Studies: Our PS Injection Molding Success Stories
We’ve helped clients across industries overcome challenges with our PS injection molding services. Below are three standout projects:
Case Study 1: Clear GPPS Blister Packs for a Cosmetics Brand
- Challenge: A cosmetics brand needed 500,000 blister packs that were clear (to showcase products), low-cost, and durable enough to withstand shipping.
- Solution: We used GPPS (90% clarity) with a scratch-resistant coating and custom tooling to match the brand’s logo and product shapes. Molds had 32 cavities for high-volume production.
- Results: Blister packs reduced packaging costs by 20% vs. acrylic alternatives; 99.8% on-time delivery; customer feedback praised the clear visibility of products.
Case Study 2: Impact-Resistant HIPS Toy Parts for a Toy Manufacturer
- Challenge: A toy company needed 300,000 toy car bodies that were tough (to withstand drops), colorful, and lightweight.
- Solution: We used HIPS (impact strength: 15 kJ/m²) with color additives and custom tooling for intricate designs (e.g., wheel wells, logos). In-line QC checked for cracks and color consistency.
- Results: Toy parts had 0 breakage in drop tests (from 1.5m); production time reduced by 15% vs. their previous supplier; cost per part lowered by 12%.
Our solution for Our Polystyrene PS Injection Molding
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Our Polystyrene PS Injection Molding
How long does it take to produce PS injection molded parts?
Lead times depend on order size and complexity: prototypes take 3–5 days (with 3D-printed molds); small batches (1,000–10,000 parts) take 1–2 weeks; high-volume runs (100,000+ parts) take 3–4 weeks (including tooling for new designs).
Is PS safe for food or medical contact?
Yes—we offer food-grade PS (GPPS/SAN) that meets FDA standards (21 CFR 177.1640) for food contact (e.g., containers, cutlery). For medical use, our sterilizable SAN/ HIPS grades meet ISO 13485 and are safe for disposable devices (e.g., syringes, test tubes).
Can recycled PS (rPS) be used for clear applications?
Our high-clarity rPS retains 88% light transmittance—ideal for semi-clear applications (e.g., opaque packaging, toy parts). For fully clear uses (e.g., blister packs), we recommend blending rPS with 30–40%
How do I compare two quotes fairly?
Match the scope first: same drawing, same material, same finish, same inspection. Then read the exclusions. Freight, tooling and certificates are the usual gaps, and a low number with three gaps is not a low number.
What material should I specify?
Specify by standard, not by trade name. A trade name can change under you between two orders; a standard number cannot. Then add the one property that actually decides the part, whether that is strength, heat resistance or chemical exposure.
How long does a first article take?
Usually a few business days once the drawing is frozen, and longer if tooling is involved. The date we give you is the date we confirm in writing, not the date we hope for.
The short version
Our Polystyrene PS Injection Molding rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.