
Blogs
Our Thermoplastic Injection Molding Services

Our Thermoplastic Injection Molding Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- Unlock precision, efficiency, and versatility with Thermoplastic Injection Molding—the go-to solution for high-volume production of consistent, custom plastic parts.
- At our shop we combine advanced equipment with decades of expertise to offer end-to-end thermoplastic injection molding capabilities.
- The injection molding process is a well-orchestrated sequence of stages, each critical to part quality and efficiency.
- Choosing the right thermoplastic material is critical to part performance.
Our Thermoplastic Injection Molding Services
Unlock precision, efficiency, and versatility with Thermoplastic Injection Molding—the go-to solution for high-volume production of consistent, custom plastic parts.
From automotive components to medical devices, our expertise in custom molding, precision tooling design, and high-performance polymers delivers cost-effective results that meet tight tolerances and accelerate time-to-market.

Our Capabilities: Delivering Precision and Scalability
At our shop we combine advanced equipment with decades of expertise to offer end-to-end thermoplastic injection molding capabilities. Our services are tailored to meet diverse project needs, from prototyping to high-volume production.
| Capability | Key Features | Typical Applications |
| Custom Molding | Tailored to unique part designs; supports complex geometries | Medical device housings, electronics enclosures |
| Precision Molding | Meets tight tolerances (±0.001–±0.005 inches); advanced quality control | Automotive sensors, aerospace components |
| High Volume Production | Automated lines with cycle times as low as 10 seconds; capacity for 1M+ parts/year | Consumer goods (toys, packaging), household appliances |
| Prototyping | Rapid tooling (3–5 days lead time); low-cost small-batch production | Product development, design validation |
| Tooling Design | In-house CAD/CAM engineering; durable steel/aluminum molds (50k–1M cycles) | All production scales |
| Quality Control | ISO 9001 & IATF 16949 certified; 100% dimensional inspection (CMM testing) | Medical devices, automotive safety parts |
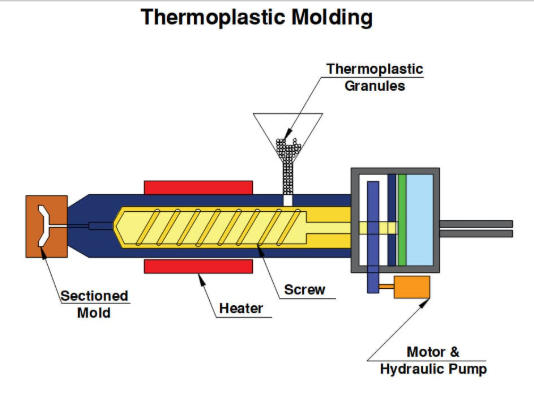
The Thermoplastic Injection Molding Process: Step-by-Step Breakdown
The injection molding process is a well-orchestrated sequence of stages, each critical to part quality and efficiency. Below is a detailed breakdown, including key metrics and optimization tips.
| Process Phase | Description | Key Metrics | Optimization Strategies |
| Material Selection | Choose the right thermoplastic material based on part function (e.g., heat resistance, flexibility). | Material density, melt flow rate (MFR) | Match MFR to mold complexity; prioritize recyclable plastics for sustainability. |
| Mold Design | Create a cavity that mirrors the part’s shape; includes gates, runners, and cooling channels. | Mold temperature (40–80°C), cavity pressure | Use simulation software to reduce material shrinkage; design for easy ejection. |
| Injection Phase | Push molten polymer into the mold at controlled speed and pressure. | Injection speed (10–100 mm/s), pressure (5k–30k psi) | Adjust speed to avoid air bubbles; optimize pressure for full cavity filling. |
| Cooling Phase | Cool the mold to solidify the plastic; cooling time impacts part warpage. | Cooling time (20–60 seconds), part temperature at ejection (below Tg) | Add cooling channels near thick sections; use water cooling for faster cycles. |
| Ejection Phase | Use pins or plates to remove the finished part from the mold. | Ejection force, part damage rate | Apply mold release agents; design ejection points on non-critical surfaces. |
| Post-Processing | Trim runners, clean parts, or add surface treatments (see Section 5). | Trim time, scrap rate (<5%) | Automate trimming to reduce labor costs; recycle scrap into new pellets. |
Automation plays a key role in streamlining this process—robotic arms can handle part ejection and inspection, cutting cycle time by 15–30% and reducing human error.
Thermoplastic Materials: Types, Properties, and Applications
Choosing the right thermoplastic material is critical to part performance. Below is a comparison of common materials, their properties, and typical uses.
| Material | Key Properties | Typical Applications | Cost Range (USD/lb) |
| ABS (Acrylonitrile Butadiene Styrene) | Impact-resistant, rigid, good surface finish | Electronics housings, toy parts | 1.50–3.00 |
| Polypropylene (PP) | Lightweight, chemical-resistant, recyclable | Packaging, automotive bumpers, containers | 0.80–1.80 |
| Polyethylene (PE) | Flexible, moisture-resistant, low cost | Plastic bags, bottles, medical tubing | 0.70–1.50 |
| Nylon (PA) | High strength, wear-resistant, heat-resistant (up to 220°C) | Gears, bearings, automotive fasteners | 2.00–4.50 |
| Polycarbonate (PC) | Transparent, shatter-resistant, high heat resistance (up to 135°C) | Safety glasses, LED light covers, medical devices | 2.50–5.00 |
| Acrylic (PMMA) | Optically clear, scratch-resistant, weatherproof | Displays, lenses, automotive lights | 2.00–4.00 |
| TPE (Thermoplastic Elastomer) | Rubber-like flexibility, recyclable, soft touch | Handle grips, seals, medical gaskets | 2.50–5.50 |
| Engineering Plastics (e.g., PEEK, PPS) | Ultra-high heat resistance (>250°C), chemical stability | Aerospace components, oil & gas parts | 15.00–50.00 |
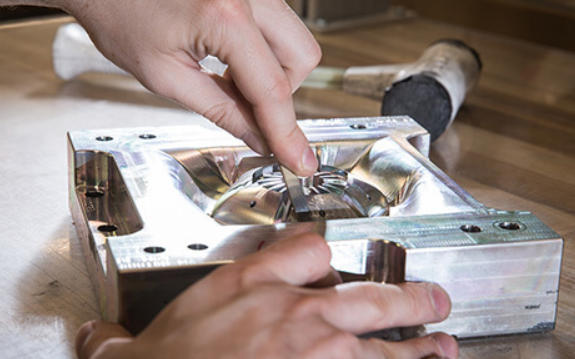
We also prioritize recyclable plastics (e.g., PP, PE, PET) to reduce environmental impact—our process recycles up to 95% of production scrap into new parts.
Tolerances: Ensuring Dimensional Accuracy
Injection molding tolerances refer to the allowable variation in part dimensions—critical for parts that need to fit with other components (e.g., automotive gears, medical syringes).
Key factors affecting tolerances:
- Material Shrinkage: All thermoplastics shrink as they cool (typically 0.5–5%). For example, PP shrinks 1.5–2.5%, while PC shrinks 0.5–1%. We account for shrinkage in mold design.
- Mold Design: Poorly placed gates or uneven cooling can cause warpage. Our molds include uniform cooling channels to minimize distortion.
- Process Parameters: Injection pressure, temperature, and cooling time must be tightly controlled. We use real-time monitoring to adjust parameters mid-production.
| Tolerance Level | Dimensional Variation (Inches) | Typical Applications | Measurement Techniques |
| Standard Tolerances | ±0.005–±0.010 | Household appliances, toys | Calipers, micrometers |
| Tight Tolerances | ±0.001–±0.005 | Automotive sensors, medical devices | Coordinate Measuring Machines (CMM), laser scanners |
| Precision Tolerances | ±0.0005–±0.001 | Aerospace components, microelectronics | Optical comparators, 3D scanning |
Our quality control team performs 100% inspection on critical parts, ensuring compliance with ISO 8062 (international tolerance standards).
Advantages of Thermoplastic Injection Molding
Injection molding advantages make it a preferred choice for high-volume, high-quality plastic production. Below are its key benefits, backed by data.
| Advantage | Description | Data/Example |
| High Production Efficiency | Automated lines enable fast cycle times (10–60 seconds per part) and 24/7 operation. | A single machine can produce 10,000+ parts/day. |
| Cost-Effective | Low per-unit cost for high volumes; scrap rates as low as 2–5% (recyclable). | For 1M parts, per-unit cost drops by 40% vs. 3D printing. |
| Design Flexibility | Supports complex geometries (e.g., undercuts, thin walls) and custom colors. | Can produce parts with wall thicknesses as low as 0.005 inches. |
| Consistency | Minimal part-to-part variation; repeatability rate >99.5%. | Critical for medical devices (e.g., syringe plungers) where uniformity is life-saving. |
| Material Variety | Compatible with 50+ thermoplastics, including engineering and high-performance polymers. | Switching materials takes <1 hour for our equipment. |
| Short Lead Times | Standard tooling takes 2–4 weeks; prototyping tooling takes 3–5 days. | Faster than CNC machining (4–6 weeks for similar parts). |
| Waste Reduction | 95% of scrap (runners, defective parts) is recycled into new pellets. | Reduces landfill waste by 80% vs. traditional manufacturing. |
Applications Industry: Where Thermoplastic Injection Molding Shines
Thermoplastic injection molding applications span nearly every industry, thanks to its versatility and scalability. Below are the top sectors and their key part types.
| Industry | Key Parts Produced | Materials Used | Volume Range |
| Automotive | Sensors, bumpers, interior panels, wire harnesses | PP, ABS, Nylon, TPE | 100k–10M parts/year |
| Consumer Electronics | Phone cases, laptop hinges, charger housings | PC, ABS, TPE | 500k–5M parts/year |
| Medical Devices | Syringe barrels, inhaler components, surgical instrument handles | PP, PE, medical-grade PC | 10k–1M parts/year (strict FDA compliance) |
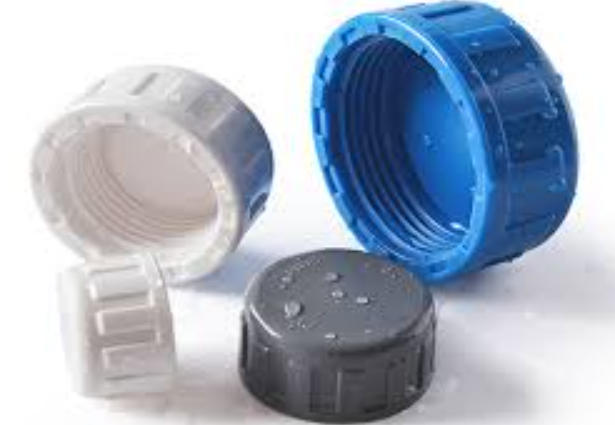
| Packaging | Bottle caps, food containers, cosmetic jars | PP, PE, PET | 1M–100M parts/year |
| Toys | Action figures, building blocks, doll parts | ABS, PP, PE | 500k–10M parts/year |
| Industrial Components | Gears, bearings, pump housings, filters | Nylon, PEEK, engineering plastics | 10k–500k parts/year |
| Aerospace | Interior panels, cable ties, sensor housings | High-performance polymers (PEEK, PPS) | 1k–10k parts/year (strict quality checks) |
| Household Appliances | Refrigerator shelves, washing machine knobs, blender blades | PP, ABS, PC | 100k–5M parts/year |
Case Studies: Real-World Success Stories
Our thermoplastic injection molding case studies demonstrate how we solve industry-specific challenges.
Case Study 1: Automotive Sensor Housing (High Volume)
- Challenge: A leading automaker needed 500k sensor housings/month with tight tolerances (±0.003 inches) and heat resistance (up to 120°C).
- Solution: Used Polycarbonate (PC) for heat resistance; designed a 4-cavity mold with automated ejection. Implemented real-time CMM inspection.
- Results: Cycle time reduced to 25 seconds; scrap rate <1%; met all IATF 16949 standards. Cost per part dropped by 22% vs. the client’s previous supplier.
Case Study 2: Medical Inhaler Component (Precision)
- Challenge: A medical device company required 100k inhaler valves/quarter with FDA compliance, chemical resistance, and ultra-tight tolerances (±0.001 inches).
- Solution: Used medical-grade PP; employed micro molding techniques and 100% laser scanning inspection. Recycled 98% of scrap.
- Results: Parts passed FDA audit; dimensional accuracy rate 99.9%; lead time cut from 8 to 4 weeks.
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- A model and a drawing that agree
- Material by standard number
- Tolerance only where it mates
- Finish and the faces it applies to
- Quantity and required date
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- process choice
- material
- tolerance band
- finish
- volume
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- A drawing that contradicts the model
- A tolerance with no datum
- A cosmetic callout with no approved sample
- A quote compared against a different scope
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
What to send with the first order
The first order sets the pattern for every order after it. Send a complete package once and the shop files it, and the second order takes a fraction of the time.
- A STEP or native model plus a PDF drawing carrying the same revision letter.
- The material callout by standard number, not by trade name.
- The finish and the exact faces it applies to.
- Any test the part must pass: fit, seal, drop, salt spray, dielectric.
- A contact who can answer a question inside one working day.
Then write down what was agreed. An email that confirms the material, the finish and the date is worth more than a longer purchase order that leaves them open.
When this is the wrong choice
A good supplier tells you when the process does not fit. These are the cases where we say so.
- The volume is so low that setup costs more than the parts are worth.
- The tolerance is tighter than the process can hold without a second operation.
- The geometry cannot be made without a tool feature that will not pay back.
- The material you need is not available in the form the process requires.
- The schedule is shorter than the tooling or setup time, and nobody has said so yet.
None of these are refusals. They are reasons to look at a different route, and the earlier that conversation happens the cheaper it is. The most expensive mistake in manufacturing is a process chosen before the question was understood.
FAQ for Thermoplastic Injection Molding
Our solution for Our Thermoplastic Injection Molding Services
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Our Thermoplastic Injection Molding Services
How do I choose the right thermoplastic material for my project?
Start by defining your part’s key requirements: temperature resistance (e.g., will it be used in a car engine bay?), chemical exposure (e.g., contact with medical fluids?), and mechanical needs (e.g., strength, flexibility). Our material experts will then recommend options—for example, if you need a lightweight, recyclable part for packaging, we’ll suggest PP; if you need a heat-resistant part for aerospace, we’ll propose PEEK. We also offer material samples for testing before full production.
What’s the minimum order quantity (MOQ) for your injection molding services?
We don’t have a strict MOQ—we cater to both small and large projects. For prototyping or small-batch production, we can handle orders as low as 50 parts (using rapid tooling). For high-volume production, our sweet spot is 10k–10M parts, where we can offer the best per-unit pricing. If you’re unsure about volume, our team can help you forecast based on your market needs.
How long does it take to go from design to finished parts?
The timeline depends on project complexity and volume:Prototyping: 3–5 days (rapid tooling + small-batch production)Standard production: 2–4 weeks (tooling design + manufacturing + full production)Complex projects (e.g., multi-shot molding, micro molding): 4–6 weeks (extra time for specialized tooling)We’ll provide a detailed timeline upfront, and our project managers will update you weekly on progress to ensure on-time delivery.
What tolerance can you hold on Our Thermoplastic Injection Molding Services?
The working default is ±0.1 mm as a working default. Tighter than that the process changes and so does the price, because every step tighter adds inspection time. Call out only the faces that mate with something else and leave the rest on the general tolerance.
What is Our Thermoplastic Injection Molding Services used for?
Our Thermoplastic Injection Molding Services turns up wherever the part has to do a real job at a predictable cost: brackets, housings, fixtures, covers and the fittings that hold them together. The honest test is whether the properties match the load and the environment, not whether the material is fashionable.
Does the process work for prototypes as well as production?
Yes, and that is usually the point. Running the prototype on the production process removes a whole class of surprises, because the part you test is made the same way as the part you sell.
The short version
Our Thermoplastic Injection Molding Services rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.