
Die Casting
What Is Integrated Die Casting and Why Does It Matter?
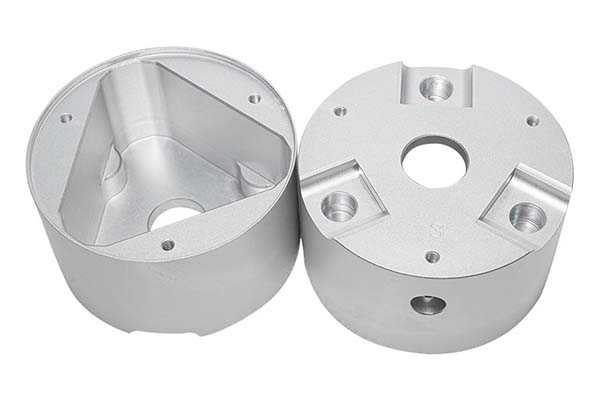
Imagine taking a car’s rear floor—normally made from 70+ stamped steel parts welded together—and producing it as one single piece in under three minutes. That is integrated die casting. It uses massive machines (6,000–12,000 tons of clamping force) to inject molten aluminum into oversized molds, creating complex structural components in a single step.
Key takeaways
- 10,000-ton+ machines: Mercedes-Benz and Chinese manufacturers are testing 12,000-ton machines to produce entire all-aluminum vehicle frames—replacing 1,000+ traditional parts.
- Is integrated die casting only suitable for large-scale production (100,000+ parts/year)?
- Integrated die casting matters because it fundamentally changes how large, complex structures are made:
How Does Integrated Die Casting Differ from Traditional Processes?
| Key Metric | Integrated Die Casting | Traditional Welding |
|---|---|---|
| Number of parts | 1–2 integrated components | 50–100+ separate stamped parts |
| Production cycle | ≤3 minutes per part (including cooling) | Hours per structure (welding + inspection + polishing) |
| Quality stability | No welds; uniform material structure | High risk of welding deformation/gaps; inconsistent strength |
| Mechanical performance | Body strength increased 30–50% | Weld joints are weak points (prone to fatigue failure) |
| Material waste | Low (5–8%); minimal scrap | High (15–20%); scrap from stamping and welding |
What Four Technological Breakthroughs Make It Possible?
Oversized Mold and Machine Design
Mold scale: Single molds weigh 50–100 tons (Tesla’s rear floor mold) with complex internal channels for cooling and fluid flow.
Machine capacity: Die-casting machines with clamping forces of 6,000–12,000 tons (vs. 2,000–3,000 tons for standard parts) generate enough pressure to fill oversized cavities uniformly.
High-Performance Heat-Free Aluminum Alloys
Material traits: Alloys like Lizhong Group’s heat-free grade eliminate post-casting heat treatment. They maintain tensile strength of 300–350 MPa and elongation of 10–15% without additional processing.
Benefit: Cuts production time 20–30% and reduces energy consumption by eliminating heat treatment ovens.
Precision Process Control
Temperature regulation: Molten metal temperature controlled within ±5°C (e.g., 680–685°C for aluminum) to avoid premature solidification or defects.
Injection speed: High-speed injection (≥5 m/s) ensures the mold fills completely before metal cools—critical for complex, thin-walled sections.
Advanced Defect Detection
Real-time monitoring: AI vision systems track filling at 1,000+ frames per second, identifying flow anomalies that cause pores or voids.
Non-destructive testing: X-ray scanning checks internal porosity—requiring <1% pore volume to meet safety standards (automotive crash requirements).
What Are the Six Core Advantages?
Lightweight Revolution (Critical for NEVs)
Weight reduction: Aluminum structures are 40–50% lighter than steel equivalents. For an EV, this translates to a 14% increase in range (500 km → 570 km).
Topology optimization: Enables bionic designs (honeycomb, grille structures) that reduce material use 10–15% while maintaining strength.
Production Efficiency Leap
Output: A single integrated line produces 80–120 parts per shift —equivalent to 20 traditional welding lines (which produce ~5 parts per shift).
Simplified workflow: Parts move directly from casting to painting—no stamping, welding, or polishing. Cuts production steps 70%.
Cost Refactoring
| Cost Category | Traditional Welding | Integrated Die Casting | Impact |
|---|---|---|---|
| Raw materials | Multi-material (steel + aluminum) | Single aluminum alloy | ↓ 10–15% material cost |
| Labor | 50–100 welders/fitters | 5–10 operators | ↓ 80% labor cost |
| Equipment | Multiple small presses + welding robots | 1 oversized die-casting island | ↑ 300% upfront; ↓ 50% long-term maintenance |
| Plant space | 1,000–1,500 m² per line | 400–600 m² per line | ↓ 60% space requirement |
Performance Jump
Stiffness: Torsional stiffness increases 50%+ (NIO’s ET7 measures 48,000 N·m/deg—far higher than traditional steel bodies).
NVH (Noise, Vibration, Harshness): Eliminating welds removes vibration points, reducing road noise by 3–5 dB (budget car → luxury car).
Thermal management: Integrated water-cooled pipelines (cast directly into the part) improve heat dissipation 20% —critical for EV battery packs.
Design Freedom
Complex structures: Bionic designs (honeycomb cores) and hidden features (storage bins, wiring channels) are now possible.
Rapid iteration: Modifying a mold is faster than retooling a welding line—cutting new product development time 30–40%.
Supply Chain Simplification
Tier reduction: Parts move directly from Tier 1 suppliers to automakers (bypassing Tier 3 stamping suppliers).
Inventory efficiency: Inventory turnover increases 3× —critical for just-in-time manufacturing.
Where Is Integrated Die Casting Used?
| Industry | Applications | Examples |
|---|---|---|
| New Energy Vehicles | Rear floors, front subframes, battery pack housings; entire vehicle frames (future) | Tesla Model Y (6,000-ton rear floor); NIO ET5/ES7 (front/rear bottom panels); Xpeng G9 (CIB battery pack) |
| Aerospace | Landing gear beams, satellite brackets, lightweight drone components | Airbus (testing for next-gen wings); SpaceX (rocket engine components) |
| Consumer Electronics | High-end notebook bodies, tablet frames | Razer Blade (integrated aluminum laptop body, 25% lighter); Apple (rumored for future iPads) |
What Technical Challenges Exist and How Are They Solved?
| Challenge | Details | Solution |
|---|---|---|
| High mold cost | Single molds cost $2–3 million (vs. $50,000 for standard); lifespan ~150,000 shots | Modular molds with replaceable inserts (cuts cost 30%); long-term contracts to spread cost |
| Narrow process window | Requires ±5°C temperature control, ≥5 m/s injection; small deviations cause defects | AI process control (adjusts parameters real-time, cuts defects 40%); vacuum die casting (eliminates 90% porosity) |
| Repair difficulty | Integrated parts can’t be disassembled; one defect scraps entire component | Strategic solder joints (retain 2–3 small welds for repairs); local extrusion pins (push out pores during casting, scrap <2%) |
What Are the Future Trends?
10,000-ton+ machines: Mercedes-Benz and Chinese manufacturers are testing 12,000-ton machines to produce entire all-aluminum vehicle frames—replacing 1,000+ traditional parts.
Closed-loop recycling: Honeycomb aluminum structures enable 95% material regeneration (current recycling rates for stamped parts are 70–80%).
Digital twin simulation: CAE tools predict microstructure and defect risks before mold production, boosting yield rates to >95% (vs. 85–90% today).
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- 3D model with the parting line marked
- Alloy grade and the standard it meets
- Wall thickness and draft on every face
- Machining allowance on the faces that will be cut
- Pressure tightness or porosity class
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- die steel and cavity count
- part weight and wall section
- draft and slide count
- porosity requirement
- machining allowance
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- Cold shuts where two flow fronts meet
- Porosity that shows up only after machining
- Soldering on a hot spot in the die
- Shrinkage voids in a heavy section
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
What to send with the first order
The first order sets the pattern for every order after it. Send a complete package once and the shop files it, and the second order takes a fraction of the time.
- A STEP or native model plus a PDF drawing carrying the same revision letter.
- The material callout by standard number, not by trade name.
- The finish and the exact faces it applies to.
- Any test the part must pass: fit, seal, drop, salt spray, dielectric.
- A contact who can answer a question inside one working day.
Then write down what was agreed. An email that confirms the material, the finish and the date is worth more than a longer purchase order that leaves them open.
When this is the wrong choice
A good supplier tells you when the process does not fit. These are the cases where we say so.
- The volume is so low that setup costs more than the parts are worth.
- The tolerance is tighter than the process can hold without a second operation.
- The geometry cannot be made without a tool feature that will not pay back.
- The material you need is not available in the form the process requires.
- The schedule is shorter than the tooling or setup time, and nobody has said so yet.
None of these are refusals. They are reasons to look at a different route, and the earlier that conversation happens the cheaper it is. The most expensive mistake in manufacturing is a process chosen before the question was understood.
Planning the ramp from prototype to production
The gap between one good part and a thousand identical ones is a plan, not a machine. Three decisions close it.
First, freeze the design. Every change after tooling starts is a re-cut, and re-cuts are where schedules go. Second, decide the inspection level. A prototype is checked by eye; a production part is checked against a report. Third, agree the change process in writing, including who pays for it.
Write the ramp down as dates and owners, not as intentions. A ramp plan with three names and three dates is worth more than a page of good intentions.
What documentation to expect
Paperwork is not bureaucracy when a part fails at the customer. It is the only record of what was agreed. A normal shipment should carry four documents.
- A dimensional report covering every callout on the drawing.
- A material certificate traceable to the heat or lot number.
- A finish or coating certificate where the specification requires one.
- A packing list that matches the carton labels.
If a supplier cannot produce these on request, they are not running a controlled process. Ask for one sample set before you place the first order and you will know exactly what you are buying.
FAQ About Integrated Die Casting
Is integrated die casting only suitable for large-scale production (100,000+ parts/year)?
Yes—due to high mold costs ($2–3 million), it is most economical for large volumes. For small batches (10,000–50,000 parts), consider hybrid solutions: integrated casting for core structures, traditional welding for non-critical components.
Can integrated die casting use materials other than aluminum?
Currently, aluminum is primary (low density, good fluidity). But magnesium alloys (even lighter) and high-strength aluminum-copper alloys (aerospace) are being tested—though they require higher pressure (8,000+ tons) and tighter temperature control.
How does integrated die casting impact crash safety for EVs?
It improves safety significantly. The uniform aluminum structure absorbs 30–40% more crash energy than welded steel parts. Tesla’s Model Y rear floor (integrated casting) passed NHTSA crash tests with 20% better occupant protection than its predecessor.
What is the minimum wall thickness possible?
With proper process control, walls as thin as 1.5–2 mm are achievable—essential for lightweighting. For comparison, stamped steel assemblies typically need 2.5–3 mm for similar strength.
How long do integrated casting molds last?
High-quality H13 steel molds with proper maintenance last 150,000–200,000 shots. After that, they can be refurbished (re-coating, surface repair) for another 50,000–100,000 shots at 30–40% of new mold cost.
Integrated die casting matters because it fundamentally changes how large, complex structures are made:
- One part replaces dozens or hundreds—eliminating assembly
- Weight drops 40–50%—extending EV range
- Strength increases 30–50%—improving safety
- Production time falls from hours to minutes—boosting efficiency
- Supply chains simplify—reducing inventory and lead times
The technology is already transforming automotive manufacturing (Tesla, NIO, Xpeng) and expanding into aerospace and electronics. With 10,000-ton machines, closed-loop recycling, and digital twin simulation on the horizon, integrated die casting will only become more capable and accessible.
For manufacturers making complex, high-volume structural parts, it is not just an option. It is the future.
Our solution for Integrated Die Casting
YiguProto runs die casting in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our die casting. You can also talk to an engineer before you commit to a drawing.
FAQ about Integrated Die Casting
What files do you need in order to quote?
A STEP file plus a PDF drawing that carries the same revision letter. The model carries the geometry and the drawing carries the intent. When the two disagree, the shop picks one, and it is never the one you meant.
What material should I specify?
Specify by standard, not by trade name. A trade name can change under you between two orders; a standard number cannot. Then add the one property that actually decides the part, whether that is strength, heat resistance or chemical exposure.
What tolerance can you hold on Integrated Die Casting?
The working default is ±0.1 mm on cast features, ±0.05 mm after machining. Tighter than that the process changes and so does the price, because every step tighter adds inspection time. Call out only the faces that mate with something else and leave the rest on the general tolerance.
How do I compare two quotes fairly?
Match the scope first: same drawing, same material, same finish, same inspection. Then read the exclusions. Freight, tooling and certificates are the usual gaps, and a low number with three gaps is not a low number.
Can Integrated Die Casting be made in small quantities?
Yes, and small quantities are where a good supplier earns the next order. Setup dominates the price at low volume, so the cheapest route is usually the one with the fewest operations, not the cheapest material.
What is the lead time for Integrated Die Casting?
Expect 20 to 30 business days including die build. Tooling, material stock and the finishing queue all move that number, so we confirm the date in writing before the run starts rather than after.
The short version
Integrated Die Casting rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.