
Blogs
Our Perfluoroalkoxy PFA Injection Molding Services

Our Perfluoroalkoxy PFA Injection Molding Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- Unlock exceptional performance with our premium Perfluoroalkoxy PFA Injection Molding services—where PFA’s unmatched high-temperature stability, chemical inertness, and biocompatibility meet micro-precision and scalable production.
- At our shop, our PFAinjection molding capacityis built to handle projects of all sizes—from low-volume prototypes to high-volume production runs.
- PFAinjection molding is a manufacturing process that shapes PFA (Perfluoroalkoxy), a melt-processable fluoropolymer, into custom parts using injection molding technology.
- PFA’s unique properties (high melting point, low viscosity when molten) require specialized process control.
Our Perfluoroalkoxy PFA Injection Molding Services
Unlock exceptional performance with our premium Perfluoroalkoxy PFA Injection Molding services—where PFA’s unmatched high-temperature stability, chemical inertness, and biocompatibility meet micro-precision and scalable production.
From medical devices to semiconductor parts, we deliver PFA-molded solutions that excel in the world’s harshest environments.

Our PFA Injection Molding Capabilities: Precision for Every Need
At our shop, our PFAinjection molding capacityis built to handle projects of all sizes—from low-volume prototypes to high-volume production runs. We specialize in tight PFA molding tolerances and offer niche services that address unique industry demands.
Below is a detailed look at our core capabilities:
| Capability | Specification | Application Fit |
| PFA molding tolerances we hold | ±0.0015” (0.038mm) for micro parts; ±0.006” (0.152mm) for standard parts | High-precision items like PFA microfluidic manifolds or semiconductor wafer carriers. |
| Micro PFA molding capability | Molding parts as small as 0.3mm (0.012”) with intricate features (e.g., 0.1mm channels) | Medical microcatheters, lab-on-a-chip devices, and miniaturized sensors. |
| High-volume PFA production | 150,000+ parts/month per production line | Automotive wire insulation, PFA food-contact molded parts (e.g., filling machine components). |
| Clean-room PFA molding service | Class 7 (10,000) cleanrooms (ISO 14644-1 compliant) | PFA medical device components (e.g., syringe tips) and pharmaceutical labware. |
| Multi-cavity PFA tooling | Up to 48-cavity molds for cost-effective high-volume runs | Small, uniform parts like PFA quick-connect couplings or valve cores. |
| Insert & over-molding PFA | Bonding PFA to metals (e.g., titanium, stainless steel) or ceramics | PFA over-molded RF connectors and sensor housings needing insulation. |
| PFA biocompatible molding | Molding with USP Class VI-certified PFA resins | Implantable medical parts and sterile disposable devices. |
What Is PFA Injection Molding?
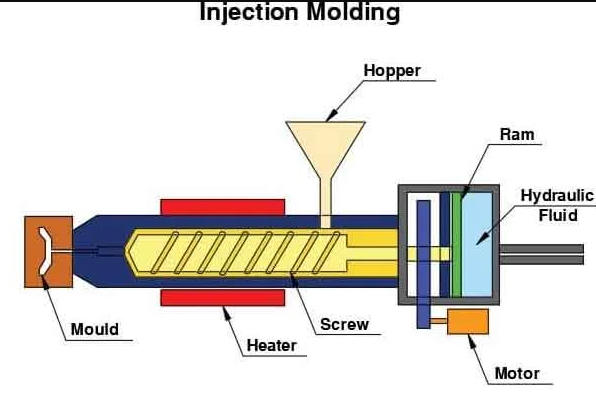
PFAinjection molding is a manufacturing process that shapes PFA (Perfluoroalkoxy), a melt-processable fluoropolymer, into custom parts using injection molding technology. As a PFA melt-processable fluoropolymer, it combines PTFE’s (Teflon) extreme chemical resistance with the moldability of thermoplastics—filling a critical gap for applications needing both durability and design flexibility.
To clarify key terms, here’s a simple breakdown:
| Term | Explanation |
| PFA thermoplastic molding | Melting PFA resin (a thermoplastic) and injecting it into molds to create functional parts. |
| Perfluoroalkoxy molding meaning | Producing components from PFA, a material valued for heat resistance, non-stick properties, and biocompatibility. |
| PFA plastic molding overview | A versatile method for making everything from tiny microfluidic parts to large industrial fittings—all with consistent quality. |
In short, PFA injection molding turns raw PFA resin into tailored components that outperform most plastics in extreme conditions.
The PFA Injection Molding Process: Step-by-Step Control
PFA’s unique properties (high melting point, low viscosity when molten) require specialized process control. Our step-by-step approach ensures consistent, high-quality parts every time.
Key Process Steps & Critical Parameters
| Step | Description | Critical Parameter | Target Value |
| 1. Resin Preparation | Dry PFA resin grades for molding to eliminate moisture (moisture causes bubbles/voids). | Drying Time/Temperature | 6 hours at 150°C |
| 2. Melting | Heat resin in the injection unit—PFA’s high melting point demands precise temperature control. | PFA melt temperature window | 350°C – 420°C (662°F – 788°F) |
| 3. Injection | Force molten PFA into the mold—low viscosity requires slow, steady pressure to avoid flash. | Injection Pressure | 600 – 1,000 bar |
| 4. Holding & Cooling | Maintain pressure to fill mold cavities fully, then cool to solidify PFA. | In-mold cooling for PFA | 15 – 25 seconds (varies by part thickness) |
| 5. Venting | Release trapped air to prevent defects—critical for PFA’s low gas permeability. | PFA venting & decompression | 0.02mm vent gaps; 50 bar decompression pressure |
| 6. Demolding & Finishing | Remove parts and trim excess material (gates/runners). | PFA degating technique | Laser degating (for micro parts); automated cold degating (standard parts) |
| 7. Quality Check | Verify dimensions and surface finish. | PFA mold shrinkage control | 3.0% – 4.0% (adjusted via mold design) |
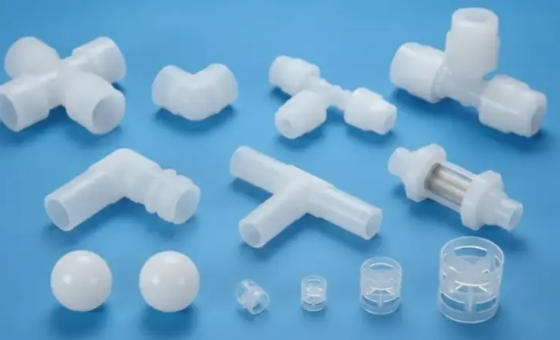
Other vital details:
- PFA screw & barrel design: Hardened steel barrels with chrome plating (resists PFA’s abrasive nature) and low-compression screws (prevents resin degradation).
- PFA molding cycle time: 45 – 90 seconds for small parts; 3 – 7 minutes for large, thick-walled components (e.g., PFA chemical processing fittings).
PFA Materials: Choosing the Right Resin for Your Project
The performance of your PFA part depends on selecting the correct resin. We offer a full range of PFA resin grades for molding, each engineered for specific industry needs.
PFA Resin Options: Features & Applications
| Resin Type | Key Feature | Compliance | Ideal Application |
| FDA-compliant PFA compounds | Non-toxic, food-safe, and resistant to hot oils/chemicals | FDA 21 CFR 177.1550; EU 10/2011 | PFA food-contact molded parts (e.g., beverage dispense nozzles) |
| Pigmented PFA pellets | Custom colors (white, black, green) with no loss of core properties | RoHS; REACH | Consumer electronics (e.g., PFA wire & cable insulation for visible components) |
| Anti-static PFA formulations | Surface resistance: 10⁷ – 10¹⁰ Ω (prevents electrostatic discharge) | SEMI F47 | PFA molded semiconductor parts (wafer carriers, chamber liners) |
| High-purity PFA resin | < 5 ppm metal impurities (ultra-low extractables) | ISO 10993; USP Class VI | PFA labware & analytical cells; medical devices (e.g., dialysis components) |
| Bondable PFA modifiers | Improved adhesion to metals/plastics (no primer needed) | ASTM D3359 (adhesion test) | Insert & over-molding PFA (e.g., sensor housings bonded to aluminum) |
| PFA conductive grades | Volume resistivity: 10⁴ – 10⁶ Ω·cm (dissipates static) | UL 94 V0 (flame retardant) | Explosion-proof applications (e.g., chemical processing valves in hazardous areas) |
Advantages of PFA Injection Molding: Why PFA Stands Out
PFA offers unique benefits that make it the top choice for demanding applications. Its combination of heat resistance, chemical inertness, and moldability outperforms most fluoropolymers and standard plastics.
PFA’s Key Advantages: Technical Specs & Real-World Benefits
| Advantage | Technical Specification | Benefit for Your Project |
| PFA chemical resistance benefit | Resists 99% of industrial chemicals (acids, bases, solvents) at 260°C | PFA chemical processing fittings last 3x longer than stainless steel alternatives. |
| PFA optical clarity advantage | Transmittance: 96% (400 – 700 nm wavelength) | Ideal for PFA optical windows in sensors and analytical equipment. |
| Low-friction PFA molding | Coefficient of friction: 0.12 (dry); 0.08 (lubricated) | Parts like PFA impellers run smoother with less energy loss and wear. |
| PFA high-temperature stability | Continuous use temperature: -200°C to 260°C; short-term use up to 300°C | Perfect for PFA aerospace injection molding (engine components, wire insulation). |
| PFA non-stick properties | Surface tension: 16 mN/m (lower than FEP) | PFA food-contact parts (e.g., baking molds) release easily with no residue. |
| PFA electrical insulation value | Volume resistivity: >10¹⁸ Ω·cm; dielectric strength: 25 kV/mm | PFA wire & cable insulation performs reliably in high-voltage applications (e.g., power grids). |
| PFA stress-crack resistance | No cracking after 10,000 hours in aggressive environments (e.g., hot water + chlorine) | PFA water treatment components (valves, pipes) avoid premature failure. |
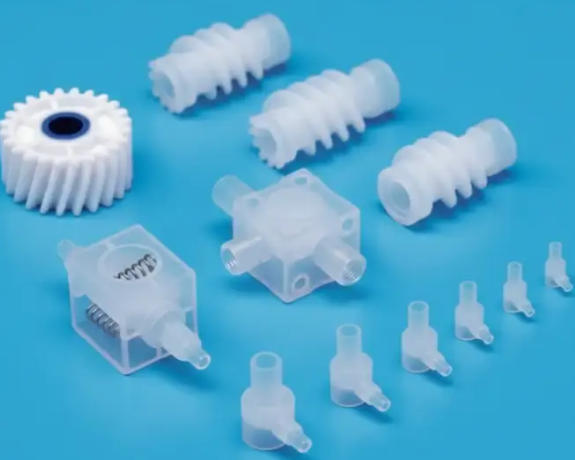
PFA Injection Molding Applications by Industry
PFA’s versatility makes it indispensable across industries. Below are key use cases where our services deliver maximum value:
Industry-Specific Applications & Our Service Fit
| Industry | Key Applications | Our Tailored Service |
| Semiconductor | PFA molded semiconductor parts (wafer carriers, electrostatic chucks, chamber liners) | Anti-static PFA formulations; Class 7 cleanroom molding |
| Medical | PFA medical device components (catheters, syringe tips, implantable parts) | Biocompatible PFA resins; ISO 13485 compliance |
| Aerospace | PFA aerospace injection molding (wire insulation, hydraulic fittings, engine sensors) | High-temperature PFA grades; PPAP documentation |
| Chemical Processing | PFA chemical processing fittings (valve bodies, pumps, pipes) | Chemical-resistant PFA; stress-crack-resistant formulations |
| Food & Beverage | PFA food-contact molded parts (filling machine nozzles, conveyor belts, baking molds) | FDA-compliant PFA; non-stick surface treatment |
| Electronics | PFA wire & cable insulation, connectors, and circuit board components | Conductive/anti-static PFA; pigmented pellets |
| Renewable Energy | PFA photovoltaic connectors, solar panel junction boxes | UV-resistant PFA; high-temperature stability |
| Laboratory & Analytical | PFA labware & analytical cells (beakers, test tubes, flow cells) | High-purity PFA resin; low-extractable formulations |
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- A model and a drawing that agree
- Material by standard number
- Tolerance only where it mates
- Finish and the faces it applies to
- Quantity and required date
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- process choice
- material
- tolerance band
- finish
- volume
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- A drawing that contradicts the model
- A tolerance with no datum
- A cosmetic callout with no approved sample
- A quote compared against a different scope
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
What to send with the first order
The first order sets the pattern for every order after it. Send a complete package once and the shop files it, and the second order takes a fraction of the time.
- A STEP or native model plus a PDF drawing carrying the same revision letter.
- The material callout by standard number, not by trade name.
- The finish and the exact faces it applies to.
- Any test the part must pass: fit, seal, drop, salt spray, dielectric.
- A contact who can answer a question inside one working day.
Then write down what was agreed. An email that confirms the material, the finish and the date is worth more than a longer purchase order that leaves them open.
Case Studies: Real-World PFA Molding Success
Our expertise isn’t just theoretical—here are three projects where we solved complex challenges with PFA injection molding:
Case 1: PFA High-Purity Valve Body for Semiconductor Manufacturing
- Challenge: A semiconductor client needed valve bodies that could handle ultra-pure chemicals (e.g., hydrofluoric acid) without contaminating wafers. The parts required ±0.002” tolerance and low metal impurities.
- Solution: Used high-purity PFA resin (< 5 ppm metals) and micro PFA molding capability with a 16-cavity mold. We added anti-static treatment to prevent electrostatic discharge.
- Result: 99.8% yield; parts passed SEMI F47 testing; client reduced wafer contamination rates by 70%.
Case 2: PFA 300°C Sensor Housing for Aerospace
- Challenge: An aerospace manufacturer needed sensor housings that could withstand 300°C (short-term) in engine bays while insulating electrical components. The housing also required bonding to a titanium bracket.
- Solution: Molded with high-temperature PFA resin (continuous use up to 260°C) and used chemical etching PFA parts to improve adhesion to titanium. We optimized in-mold cooling for PFA to reduce cycle time.
- Result: Housings passed 1,000 hours of thermal testing; bond strength exceeded 20 N/cm; production time cut by 25%.
Our solution for Our Perfluoroalkoxy PFA Injection Molding
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Our Perfluoroalkoxy PFA Injection Molding
How does PFA injection molding compare to FEP injection molding?
PFA and FEP are both fluoropolymers, but PFA has a higher continuous use temperature (260°C vs. FEP’s 200°C) and better stress-crack resistance. FEP offers slightly better optical clarity (95% vs. PFA’s 96%) and lower cost. PFA is ideal for high-temperature applications (e.g., aerospace engine parts), while FEP works well for mid-temperature uses (e.g., food-contact fittings).
Can PFA parts be sterilized, and if so, how?
Yes! PFA is highly sterilizable—compatible with all common sterilization methods used in medical and pharmaceutical industries. These include autoclaving (steam sterilization at 134°C/273°F for 15–20 minutes), ethylene oxide (EO) gas sterilization, gamma radiation (up to 50 kGy), and plasma sterilization. PFA’s high-temperature stability and chemical inertness mean it retains all its properties (e.g., biocompatibility, dimensional stability) after repeated sterilization cycles—critical for reusable PFA medical device components like surgical tools or diagnostic equipment.
What factors affect the cost of PFA injection molding, and how can we optimize it?
The main cost drivers for PFA injection molding include: (1) PFA resin grades (high-purity or biocompatible grades cost 20–30% more than standard grades); (2) tooling (multi-cavity molds have higher upfront costs but lower per-part costs for high-volume runs); (3) part complexity (micro parts or those requiring surface treatment add 15–25% to costs); (4) production volume (low-volume prototypes cost more per unit than high-volume orders). To optimize costs, we recommend: using standard PFA resin grades if your application doesn’t require specialty formulations; designing parts for multi-cavity tooling (e.g., for 100,000+ units); and combining small-volume orders into larger runs when possible. Our team also offers free design-for-manufacturability (DFM) reviews to identify cost-saving opportunities without compromising quality.
How long does a first article take?
Usually a few business days once the drawing is frozen, and longer if tooling is involved. The date we give you is the date we confirm in writing, not the date we hope for.
What should I check before approving the parts?
Datums first, then the features that mate, then the cosmetic faces. Ask for a dimensional report, a material certificate and a finish sample. A part can be inside every tolerance and still not fit, so assemble one before you sign.
What is Our Perfluoroalkoxy PFA Injection Molding used for?
Our Perfluoroalkoxy PFA Injection Molding turns up wherever the part has to do a real job at a predictable cost: brackets, housings, fixtures, covers and the fittings that hold them together. The honest test is whether the properties match the load and the environment, not whether the material is fashionable.
The short version
Our Perfluoroalkoxy PFA Injection Molding rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.