
Die Casting
What Is Hot Chamber Die Casting and How Does It Work?
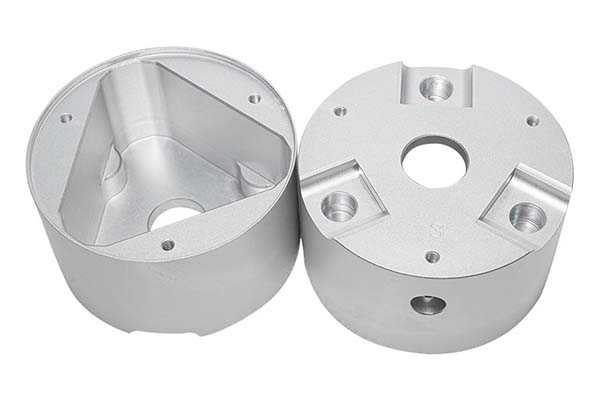
If you need to produce thousands of small metal parts—phone connectors, faucet handles, toy cars—quickly and economically, hot chamber die casting is likely the process you need. It is fast, efficient, and designed specifically for low-melting-point alloys like zinc and magnesium.
Key takeaways
- Hot chamber die casting’s unique performance comes from its specialized structure and closed-loop workflow.
- Hot chamber die casting is optimized for specific materials and part types.
- Can hot chamber die casting produce parts with complex shapes like undercuts?
- Hot chamber die casting is the go-to process for high-volume production of small, thin-walled metal parts. Its immersed injection system delivers:
What Are the Core Principles and Structural Design?
Hot chamber die casting’s unique performance comes from its specialized structure and closed-loop workflow.
Key Structural Components
Five interconnected parts enable seamless molten metal handling:
Crucible: Heat-resistant container holding molten alloy at constant temperature (e.g., 380–450°C for zinc alloys).
Injection chamber: Cylindrical tube immersed in the crucible’s molten metal. Its volume matches the part’s required metal quantity.
Injection punch: Piston that moves downward to push molten metal from the injection chamber into the mold.
Gooseneck tube: Curved channel connecting injection chamber to mold gate—ensures molten metal flows in a closed path (no air exposure).
Mold assembly: Two-part mold (fixed + movable) with cavities shaped like the final part. Includes cooling channels to speed solidification.
Step-by-Step Working Mechanism
The process follows a linear, automated cycle:
1. Mold closing: Movable mold half clamps tightly against fixed half. Clamping force: 50–200 tons, depending on part size.
2. Metal injection: Punch moves downward, applying pressure (5–30 MPa) to push molten metal from injection chamber through gooseneck tube and into mold cavity. Closed channel prevents oxidation.
3. Solidification: Coolant flows through mold’s cooling channels, rapidly solidifying metal (5–10 seconds for thin-walled parts).
4. Mold opening: Movable mold half retracts; ejector pins push finished part out.
5. Reset: Punch retracts, drawing fresh molten metal into injection chamber—ready for next cycle.
Total cycle time: 15–30 seconds per part.
What Materials and Applications Work Best?
Hot chamber die casting is optimized for specific materials and part types.
Ideal Materials: Low-Melting-Point Alloys
The process only works with alloys melting below the injection chamber’s heat resistance (typically <500°C).
| Alloy Type | Melting Point (°C) | Tensile Strength (MPa) | Key Advantages | Typical Applications |
|---|---|---|---|---|
| Zinc alloys (Zamak 3, Zamak 5) | 380–420 | 280–320 | High fluidity; low cost; easy to plate | 3C parts (phone buttons, connector housings); bathroom hardware (faucet handles) |
| Magnesium alloys (AZ91D) | 595–610 | 230–280 | Lightweight (1.8 g/cm³); good strength-to-weight | Laptop hinges; small automotive sensors |
| Lead-tin alloys | 183–327 | 100–150 | High ductility; corrosion resistance | Soldering components; battery terminals |
Critical note: Cannot process aluminum (660°C) or brass (900°C)—these would damage the immersed injection chamber.
Perfect Part Characteristics
Parts suited for hot chamber die casting share three traits:
Small size: Typically under 500 g (10–200 g common). Larger parts need higher pressure, exceeding process limits.
Thin walls: Ideal thickness 0.5–3 mm. Fast cooling and good fluidity ensure uniform filling of thin sections.
High volume: Best for 100,000+ parts/year. Automated cycles and low scrap (5–8%) make it cost-effective for mass production.
Industry Applications
| Industry | Part Examples | Process Benefits |
|---|---|---|
| 3C Electronics | Phone charger housings, USB shells, LED bases | 20 parts/minute; surface finish Ra 3.2–6.3 μm |
| Home & Hardware | Faucet knobs, cabinet handles, door hinges | $0.10–0.50/part; easy to polish/plate |
| Automotive | Small sensors (temp/pressure), window regulators | ±0.1 mm tolerance; dimensional stability |
| Toys & Gifts | Die-cast toy cars, decorative figurines | Complex shapes with minimal defects |
What Are the Advantages and Limitations?
| Category | Details | Quantitative Data |
|---|---|---|
| Advantages | • High efficiency: No separate pouring; integrated metal storage/injection• Low defect rate: Closed channel reduces oxidation (defect rate <3%)• Compact equipment: No external furnace—saves 40–60% floor space• Low energy use: Constant temperature maintenance uses 20–30% less energy | Cycle time: 15–30 s/part (2–4× faster than cold chamber)Scrap rate: 5–8% (vs. 10–15% cold chamber)Floor space: 10–20 m² per line (vs. 30–50 m²) |
| Limitations | • Equipment wear: Molten metal erodes injection chamber—lifespan 10,000–30,000 shots• Pressure limits: 5–30 MPa cannot fill thick-walled or large parts• Material restriction: Only low-melting alloys—no aluminum, brass, steel• Iron content risk: Molten metal picks up iron over time (>1.2% degrades performance) | Replacement cost: $5,000–15,000/yearMax part weight: <500 gIron buildup: ~0.01% per 1,000 shots |
Hot Chamber vs. Cold Chamber: Key Differences
| Factor | Hot Chamber | Cold Chamber |
|---|---|---|
| Injection chamber | Immersed in molten metal (closed system) | Separate from furnace (open system) |
| Suitable materials | Zinc, magnesium, lead-tin | Aluminum, brass, copper (high-melting) |
| Part size/weight | Small (<500 g), thin-walled | Large (>500 g), thick-walled (engine blocks) |
| Cycle time | Fast (15–30 s/part) | Slow (30–60 s/part) |
| Injection pressure | Low (5–30 MPa) | High (30–150 MPa) |
| Equipment cost | Low ($50,000–200,000 per line) | High ($200,000–1M+ per line) |
| Scrap rate | 5–8% | 10–15% |
Best Practices for Optimal Performance
Equipment Maintenance
Injection chamber/punch: Inspect every 5,000 shots. Replace when inner diameter increases >0.1 mm (prevents metal leakage).
Gooseneck tube: Clean weekly to remove oxide buildup (wire brush + solvent). Blockages cause incomplete filling.
Temperature control: Use digital thermostat to maintain molten metal within ±5°C (e.g., 400±5°C for Zamak 5). Fluctuations increase defects.
Process Parameter Optimization (Zinc Alloys)
| Parameter | Ideal Range | Impact of Wrong Settings |
|---|---|---|
| Injection pressure | 10–20 MPa | Too low: incomplete fill; Too high: mold damage |
| Injection speed | 0.5–1.5 m/s | Too fast: turbulence (air traps); Too slow: premature solidification |
| Cooling time | 5–10 seconds | Too short: part deformation; Too long: reduced efficiency |
Quality Control
Alloy testing: Check iron content every 1,000 shots (keep <1.2% for zinc). Add iron neutralizers (nickel) if levels exceed limits.
Part inspection: Use CMM to verify dimensions (±0.1 mm tolerance) for critical parts like electronic connectors.
Defect tracking: Log defects (porosity, cold shuts) and link to parameters to identify trends.
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- 3D model with the parting line marked
- Alloy grade and the standard it meets
- Wall thickness and draft on every face
- Machining allowance on the faces that will be cut
- Pressure tightness or porosity class
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- die steel and cavity count
- part weight and wall section
- draft and slide count
- porosity requirement
- machining allowance
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- Cold shuts where two flow fronts meet
- Porosity that shows up only after machining
- Soldering on a hot spot in the die
- Shrinkage voids in a heavy section
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
What to send with the first order
The first order sets the pattern for every order after it. Send a complete package once and the shop files it, and the second order takes a fraction of the time.
- A STEP or native model plus a PDF drawing carrying the same revision letter.
- The material callout by standard number, not by trade name.
- The finish and the exact faces it applies to.
- Any test the part must pass: fit, seal, drop, salt spray, dielectric.
- A contact who can answer a question inside one working day.
Then write down what was agreed. An email that confirms the material, the finish and the date is worth more than a longer purchase order that leaves them open.
When this is the wrong choice
A good supplier tells you when the process does not fit. These are the cases where we say so.
- The volume is so low that setup costs more than the parts are worth.
- The tolerance is tighter than the process can hold without a second operation.
- The geometry cannot be made without a tool feature that will not pay back.
- The material you need is not available in the form the process requires.
- The schedule is shorter than the tooling or setup time, and nobody has said so yet.
None of these are refusals. They are reasons to look at a different route, and the earlier that conversation happens the cheaper it is. The most expensive mistake in manufacturing is a process chosen before the question was understood.
Planning the ramp from prototype to production
The gap between one good part and a thousand identical ones is a plan, not a machine. Three decisions close it.
First, freeze the design. Every change after tooling starts is a re-cut, and re-cuts are where schedules go. Second, decide the inspection level. A prototype is checked by eye; a production part is checked against a report. Third, agree the change process in writing, including who pays for it.
Write the ramp down as dates and owners, not as intentions. A ramp plan with three names and three dates is worth more than a page of good intentions.
FAQ About Hot Chamber Die Casting
Can hot chamber die casting produce parts with complex shapes like undercuts?
Yes—with slider molds. Phone connector housings with undercut grooves use 1–2 sliders that retract after solidification. However, slider count is limited (max 3) due to low pressure—too many increase incomplete filling risk.
How does it compare to plastic injection molding for small parts?
Hot chamber die casting is better for metal parts requiring strength (zinc phone buttons)—tensile strength 280–320 MPa vs. 50–100 MPa for plastics. Plastic injection is cheaper for non-load parts (toy casings) but cannot match metal’s durability.
What is typical lead time for a hot chamber die casting project?
Mold development: 4–6 weeks (simple: 4 weeks; complex with sliders: 6 weeks). After mold approval, production starts within 1 week. For 100,000+ part batches, delivery lead time is 2–4 weeks (depending on volume).
How do I prevent iron contamination in zinc alloys?
Three steps:
- Test iron content every 1,000 shots
- Keep iron <1.2% (if exceeded, add 0.1–0.3% nickel as neutralizer)
- Replace injection chamber when inner diameter wear >0.1 mm (worn chambers release more iron)
What surface finish can I expect as-cast?
Ra 3.2–6.3 μm is standard. For cosmetic parts, specify:
- Polishing: Ra ≤0.8 μm
- Plating (chrome/nickel): Bright, reflective finish
- Powder coating: Smooth, colored finish
Hot chamber die casting is the go-to process for high-volume production of small, thin-walled metal parts. Its immersed injection system delivers:
- Speed: 15–30 second cycles—2–4× faster than cold chamber
- Efficiency: 5–8% scrap rate; 20–30% less energy
- Quality: Closed system prevents oxidation; consistent surface finish
- Economy: Low equipment cost ($50,000–200,000); per-part costs as low as $0.10–0.50
It works best for:
- Zinc alloys (most common)—Zamak 3, Zamak 5
- Magnesium alloys—AZ91D for lightweight parts
- Small parts—under 500 g, 0.5–3 mm walls
- High volume—100,000+ parts/year
The limitations are clear: low pressure restricts part size, equipment wears faster than cold chamber, and aluminum is off-limits. But for the right applications, nothing beats its combination of speed, cost, and quality.
Our solution for Hot Chamber Die Casting
YiguProto runs die casting in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our die casting. You can also talk to an engineer before you commit to a drawing.
FAQ about Hot Chamber Die Casting
How do I compare two quotes fairly?
Match the scope first: same drawing, same material, same finish, same inspection. Then read the exclusions. Freight, tooling and certificates are the usual gaps, and a low number with three gaps is not a low number.
Is there a minimum order quantity?
No hard minimum. One part is fine. What changes with volume is which costs dominate, so a single unit is priced mostly on setup and a thousand units are priced mostly on cycle time and material.
What material should I specify?
Specify by standard, not by trade name. A trade name can change under you between two orders; a standard number cannot. Then add the one property that actually decides the part, whether that is strength, heat resistance or chemical exposure.
How much does Hot Chamber Die Casting cost?
Price comes from five lines: material, machine or tool time, setup, finishing and inspection. The material itself is usually the smallest of them. Send a drawing and we will split the quote so you can see which line is doing the damage.
What is Hot Chamber Die Casting used for?
Hot Chamber Die Casting turns up wherever the part has to do a real job at a predictable cost: brackets, housings, fixtures, covers and the fittings that hold them together. The honest test is whether the properties match the load and the environment, not whether the material is fashionable.
Can Hot Chamber Die Casting be made in small quantities?
Yes, and small quantities are where a good supplier earns the next order. Setup dominates the price at low volume, so the cheapest route is usually the one with the fewest operations, not the cheapest material.
The short version
Hot Chamber Die Casting rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.