
Blogs
Aerospace 3D Printing Services

Aerospace 3D Printing Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- Elevate your aerospace projects with our shop’s cutting-edge Aerospace 3D Printing solutions.
- Aerospace 3D Printing—a specialized branch of Additive Manufacturing—is a game-changing technology that builds complex aerospace parts layer by layer using digital designs.
- Aerospace 3D Printing excels at creating parts that balance performance, weight, and durability—critical for aerospace applications where every gram and every millimeter matters.
- The success of Aerospace 3D Printing depends on choosing materials that can withstand the harsh conditions of flight and space—extreme temperatures, high pressure, and constant vibration.
Aerospace 3D Printing Services
Elevate your aerospace projects with our shop’s cutting-edge Aerospace 3D Printing solutions. We leverage advanced Additive Manufacturing technologies, certified engineers, and high-performance materials like titanium alloys and carbon fiber composites to craft custom engine components, satellite parts, and lightweight airframe structures—delivering unmatched precision, 30% weight reduction, and faster production timelines.
Whether you need rapid prototyping for drone development or complex geometries for military applications, our shop is your trusted partner for meeting strict Industry Standards in aerospace innovation.

What is Aerospace 3D Printing?
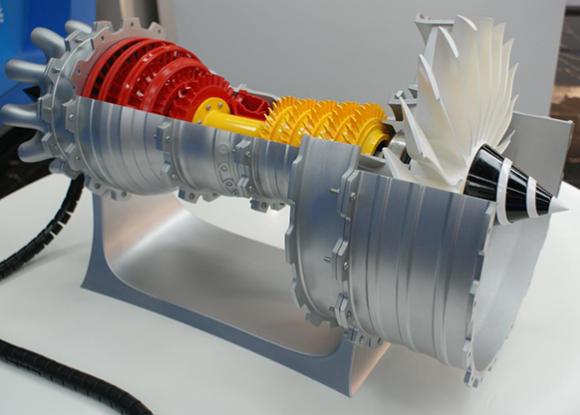
Aerospace 3D Printing—a specialized branch of Additive Manufacturing—is a game-changing technology that builds complex aerospace parts layer by layer using digital designs. Unlike traditional manufacturing (which often struggles with intricate shapes and generates excess waste), this process enables precise control over material placement, making it ideal for the high-stakes, high-precision demands of the aerospace industry.
At its core, Aerospace 3D Printing is driven by Precision Engineering—parts are produced with tolerances as tight as 0.005mm, critical for components that must withstand extreme temperatures, pressure, and vibration. It’s also a cornerstone of modern aerospace workflows, aligning with strict Industry Standards (such as AS9100 for aerospace quality management and ASTM F3301 for additive manufacturing of metal parts).
Common Aerospace Parts Produced with 3D Printing
Aerospace 3D Printing excels at creating parts that balance performance, weight, and durability—critical for aerospace applications where every gram and every millimeter matters. Below are the most common parts we produce, along with their key benefits:
| Aerospace Part | Key 3D Printing Benefit | Typical Material |
| Engine Components (e.g., turbine blades, fuel nozzles) | Withstands high temperatures (up to 1,200°C); complex internal cooling channels | Titanium alloys, super alloys (Inconel) |
| Airframe Parts (e.g., wing brackets, fuselage components) | 30–40% weight reduction vs. traditional parts; improved structural integrity | Aluminum alloys, carbon fiber composites |
| Avionics Housings | Lightweight, shock-resistant; custom fit for electronics | High-temperature polymers (PEKK), carbon fiber composites |
| Ducting Systems (e.g., cooling ducts) | Complex shapes to optimize airflow; corrosion-resistant | Titanium alloys, aluminum alloys |
| Satellite Components (e.g., antenna brackets, structural frames) | Low weight (critical for launch costs); high strength-to-weight ratio | Titanium alloys, carbon fiber composites |
| Lightweight Structures (e.g., lattice panels) | Reduces overall aircraft/satellite weight; maintains strength | Aluminum alloys, carbon fiber composites |
For example, a traditional aluminum airframe bracket weighs 500g and takes 2 weeks to produce. A 3D-printed version (using aluminum alloy) weighs just 300g (40% lighter) and is ready in 3 days—cutting both weight (which lowers fuel costs) and production time.
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- A model and a drawing that agree
- Material by standard number
- Tolerance only where it mates
- Finish and the faces it applies to
- Quantity and required date
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- process choice
- material
- tolerance band
- finish
- volume
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- A drawing that contradicts the model
- A tolerance with no datum
- A cosmetic callout with no approved sample
- A quote compared against a different scope
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
What to send with the first order
The first order sets the pattern for every order after it. Send a complete package once and the shop files it, and the second order takes a fraction of the time.
- A STEP or native model plus a PDF drawing carrying the same revision letter.
- The material callout by standard number, not by trade name.
- The finish and the exact faces it applies to.
- Any test the part must pass: fit, seal, drop, salt spray, dielectric.
- A contact who can answer a question inside one working day.
Then write down what was agreed. An email that confirms the material, the finish and the date is worth more than a longer purchase order that leaves them open.
When this is the wrong choice
A good supplier tells you when the process does not fit. These are the cases where we say so.
- The volume is so low that setup costs more than the parts are worth.
- The tolerance is tighter than the process can hold without a second operation.
- The geometry cannot be made without a tool feature that will not pay back.
- The material you need is not available in the form the process requires.
- The schedule is shorter than the tooling or setup time, and nobody has said so yet.
None of these are refusals. They are reasons to look at a different route, and the earlier that conversation happens the cheaper it is. The most expensive mistake in manufacturing is a process chosen before the question was understood.
Planning the ramp from prototype to production
The gap between one good part and a thousand identical ones is a plan, not a machine. Three decisions close it.
First, freeze the design. Every change after tooling starts is a re-cut, and re-cuts are where schedules go. Second, decide the inspection level. A prototype is checked by eye; a production part is checked against a report. Third, agree the change process in writing, including who pays for it.
Write the ramp down as dates and owners, not as intentions. A ramp plan with three names and three dates is worth more than a page of good intentions.
What documentation to expect
Paperwork is not bureaucracy when a part fails at the customer. It is the only record of what was agreed. A normal shipment should carry four documents.
- A dimensional report covering every callout on the drawing.
- A material certificate traceable to the heat or lot number.
- A finish or coating certificate where the specification requires one.
- A packing list that matches the carton labels.
If a supplier cannot produce these on request, they are not running a controlled process. Ask for one sample set before you place the first order and you will know exactly what you are buying.
How to handle a change after the order
Changes happen. What matters is whether the change is priced, scheduled and recorded, or absorbed quietly and discovered later.
Send the change as a new revision, not as a note in an email. Ask for three answers in writing: what it costs, what it does to the date, and what happens to material or tooling already committed. Then decide.
A change without a revision number is a rumour. The shop will build what it has on file, and both sides will be right and unhappy at the same time.
How the work actually runs, step by step
Most buyers see two numbers: a price and a date. Between them sits a sequence that decides both. On manufacturing work it looks like this.
- File review. The model and the drawing are checked against each other. Where they disagree, the shop stops and asks, because guessing is how scrap gets made.
- DFM feedback. The features that add cost and the features that will not hold tolerance are listed. This is the cheapest hour in the whole project.
- Setup or tooling. Fixtures, programs or a tool are built. Everything downstream inherits the quality of this step.
- First article. One part is made and measured against the drawing before anything else runs. Nothing is signed until it passes.
- Production. The run goes ahead with the parameters that produced the approved first article, not with new ones.
- Inspection and packing. The callouts are measured, the certificate is matched, and the parts are packed so they arrive in the condition they left in.
Ask any supplier to walk you through these six steps on your part. The answers tell you more about the shop than the price does.
How it compares with the alternatives
No process wins everywhere. The honest comparison is against the two routes you would otherwise take, and the answer usually turns on volume, tolerance and how much the tooling costs.
- Low volume, simple geometry: a faster process usually wins, because setup dominates the price and there is no tool to amortise.
- High volume, stable design: the dedicated process wins, because cycle time replaces labour and the tool cost spreads thin.
- Tight tolerance on a few faces: add a finishing operation rather than paying for a tighter process everywhere.
- One-off repair or legacy part: a digital route is often the only one that makes economic sense.
Decide with the crossover volume, not with a preference. Ask each supplier where their process stops being competitive, and you will usually get a straight answer.
What a good finished part looks like
Quality is not a certificate on the wall. It is a set of things you can see and measure on the part in your hand, and they are the same on the first unit and the five-hundredth.
- Clean edges. No burr that will cut the person packing the box, no dross left on a cut face.
- Even finish. The same colour and texture across the whole surface, with no drift between batches.
- Straight geometry. A part that sits flat on a surface plate without rocking, and that measures the same on two different days.
- Correct fit. It assembles against its mating part with hand pressure, not with a press and not with a file.
- Traceable paperwork. A report that matches the parts in the box, with the heat or lot number on both.
None of these require a laboratory. They require a shop that checks the first part properly and then keeps the process still. If the fifth part looks different from the first, the process moved and nobody noticed.
Materials Used in Aerospace 3D Printing: Strong, Light, and Resilient
The success of Aerospace 3D Printing depends on choosing materials that can withstand the harsh conditions of flight and space—extreme temperatures, high pressure, and constant vibration. At our shop, our procurement team (as Purchase Managers) sources only high-quality, aerospace-grade materials from certified suppliers, ensuring consistency and compliance with Industry Standards. Below is a breakdown of our key materials:
| Material Type | Key Properties | Common Aerospace Applications |
| Titanium Alloys | High strength-to-weight ratio, corrosion-resistant, withstands temperatures up to 600°C | Engine components, satellite structures, airframe brackets |
| Aluminum Alloys | Lightweight (1/3 the weight of steel), good thermal conductivity, cost-effective | Airframe parts, ducting systems, avionics housings |
| High-Temperature Polymers (PEKK, PEEK) | Resists temperatures up to 300°C, lightweight, chemical-resistant | Avionics housings, interior components, drone parts |
| Carbon Fiber Composites | Ultra-lightweight, high strength (stronger than steel), rigid | Airframe parts, satellite panels, drone wings |
| Super Alloys (Inconel, Hastelloy) | Withstands extreme temperatures (up to 1,200°C), corrosion-resistant | Engine turbine blades, fuel nozzles, heat exchangers |
| Biocompatible Materials (for crewed spacecraft) | Non-toxic, hypoallergenic, meets medical standards | Crew cabin components, tool handles |
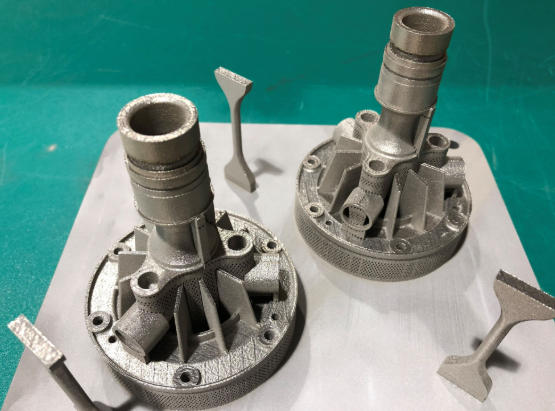
Our materials undergo rigorous testing: for example, our titanium alloys have a tensile strength of 900MPa (exceeding aerospace requirements of 800MPa) and are certified to ASTM F2924 (standard for 3D-printed titanium parts in aerospace).
Our solution for Aerospace 3D Printing Services
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Aerospace 3D Printing Services
Do 3D-printed aerospace parts meet the strict safety standards of the industry?
Absolutely. Every 3D-printed aerospace part we produce adheres to the most rigorous Industry Standards, including AS9100 (for aerospace quality management), ASTM F3301 (for metal additive manufacturing), and NASA’s RP-1621 (for spaceflight hardware). Our quality control process—including X-ray CT scanning, tensile testing, and dimensional verification with CMMs—ensures parts are free of defects and perform reliably under extreme aerospace conditions. For example, our 3D-printed turbine blades have passed 10,000+ hours of fatigue testing (exceeding the 8,000-hour requirement for commercial aircraft engines), confirming their safety and durability.
How does the cost of 3D-printed aerospace parts compare to traditionally manufactured parts for large-scale production?
While Aerospace 3D Printing has higher upfront costs (e.g., equipment, certified materials), it becomes cost-competitive—even for large-scale production—by reducing long-term expenses. For runs of 100+ parts:Material Savings: Additive manufacturing uses 90% of raw material (vs. 50% for machining), cutting material costs by 40%. For example, producing 500 aluminum airframe brackets via 3D printing saves $20,000 in material costs vs. traditional methods.Tooling Elimination: No need for expensive molds or dies (which can cost 50,000–200,000 for complex parts). This is a major advantage for parts with short production runs (e.g., military drone components).Labor Efficiency: Automated 3D printing workflows reduce labor time by 60%, lowering labor costs for large batches. Over 1 year of producing 1,000 satellite brackets, 3D printing cuts total costs by 25–30% compared to traditional manufacturing.
Can Yigu Technology handle custom aerospace projects that require unique materials or complex geometries?
Yes—customization is one of our core strengths. Our team of Certified Engineers and procurement specialists works closely with clients to address even the most unique project needs:Unique Materials: If your project requires a specialized material (e.g., a heat-resistant super alloy for rocket components or a biocompatible polymer for crewed spacecraft), our procurement team sources it from certified aerospace suppliers and tests it to ensure compliance. We recently worked with a defense client to 3D print parts using a custom titanium-aluminum alloy that withstands 800°C—critical for their hypersonic vehicle project.Complex Geometries: We specialize in printing parts with intricate designs, such as lattice structures (for weight reduction), internal cooling channels (for engine parts), and organic shapes (for aerodynamic efficiency). For a satellite client, we 3D printed an antenna bracket with a 60% hollow lattice structure—achieving a 45% weight reduction while maintaining structural strength—something traditional machining could not produce.Our end-to-end process—from design optimization to post-processing—ensures custom parts meet your performance requirements and Industry Standards, on time and on budget.
Is there a minimum order quantity?
No hard minimum. One part is fine. What changes with volume is which costs dominate, so a single unit is priced mostly on setup and a thousand units are priced mostly on cycle time and material.
Does the process work for prototypes as well as production?
Yes, and that is usually the point. Running the prototype on the production process removes a whole class of surprises, because the part you test is made the same way as the part you sell.
What happens if a part is out of specification?
We measure it against the same drawing you approved and, if it misses, we make it again. What matters is that the report exists, because a disagreement without data is just an opinion.
The short version
Aerospace 3D Printing Services rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.