
Blogs
Our Liquid Crystal Polymer LCP Injection Molding Services

Our Liquid Crystal Polymer LCP Injection Molding Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- Elevate precision manufacturing for high-tech applications with our LCP Injection Molding services—where the ultra-low viscosity and thermal stability of Liquid-crystal polymer (LCP) meet micro-scale engineering excellence.
- At our shop, our LCP Injection Molding capabilities are engineered to unlock LCP’s unique potential for ultra-precise, high-performance parts.
- LCPInjection Molding is the process of shaping Liquid-crystal polymer (LCP)—a unique engineering plastic with thermotropic mesomorphic behavior (forms ordered liquid-crystal structures when melted)—into high-precision components via injection molding.
- LCP’s unique thermotropic mesomorphic behavior and ultra-low viscosity require a highly controlled injection molding process.
Our Liquid Crystal Polymer LCP Injection Molding Services
Elevate precision manufacturing for high-tech applications with our LCP Injection Molding services—where the ultra-low viscosity and thermal stability of Liquid-crystal polymer (LCP) meet micro-scale engineering excellence.
From 5G mmWave connectors to surgical micro-catheters, we deliver parts with unmatched thin-wall capabilities and high-frequency performance, backed by expertise in optimizing thermotropic mesomorphic behavior for critical industries.

Our Capabilities: Mastering Micro-Scale LCP Molding
At our shop, our LCP Injection Molding capabilities are engineered to unlock LCP’s unique potential for ultra-precise, high-performance parts. We invest in specialized equipment and expertise to handle LCP’s high-flow, high-temperature requirements, even for the most demanding micro-components. Below is a detailed overview of our core capabilities:
Core Capabilities Overview
| Capability | Description | Technical Specs | Ideal For |
| 0.05 mm Thin-Wall Molding | Specialized processes to mold LCP into ultra-thin sections without short shots | Minimum wall thickness: 0.05 mm; Aspect ratio (depth:wall): 20:1 | 5G mmWave connectors, surgical micro-catheter tips |
| 0.08 g Micro-Shot | Precision dosing for ultra-small LCP parts with minimal material waste | Minimum shot weight: 0.08 g; Feature size: 0.1 mm | Hearing-aid shells, micro-gears (insulin pumps) |
| ±5 µm True-Position | CNC-controlled machines with sub-micron accuracy for tight tolerances | Position tolerance: ±5 µm; Dimensional repeatability: ±2 µm | Fiber-optic ferrules, DDR5 memory socket pins |
| Multi-Cavity Hot-Runner | Custom hot-runner molds with up to 128 cavities for high-volume micro-parts | High-cavitation up to 128-fold; Cycle time reduction: 60–70% vs. single-cavity | Smartphone camera holders, IoT antenna modules |
| 400 °C Electric Presses | High-temperature electric injection molding machines optimized for LCP’s melt requirements | Barrel temp range: 320–360 °C; Injection speed: Up to 1,000 mm/s | High-heat parts (e.g., automotive sensors, aerospace coax filters) |
| Clean-Room ISO 7 | Class 7 (10,000-class) cleanroom for contamination-sensitive LCP parts | Particle count: <10,000 particles/ft³ (≥0.5 μm) | Medical devices (surgical catheters), semiconductor components |
| Vision 100% Inspection | Automated optical inspection (AOI) systems to check 100% of parts for defects | Detection accuracy: 0.005 mm; Inspection speed: 1,200 parts/hour | High-volume electronics (5G connectors, DDR5 sockets) |
| In-House CT Scanning | 3D CT scanning to inspect internal and external geometry of complex LCP parts | Resolution: 5 µm; Scan time: <5 minutes/part | RF filters (internal cavities), micro-assemblies |
| Rapid-Tool Change | Quick-change tooling systems to switch molds in under 2 hours | Tool change time: <120 minutes; Compatible with all cavity counts | Low-volume runs, multi-SKU production |
Our in-house DfM + mold-flow (Design for Manufacturability) support also ensures your LCP part designs are optimized for molding—reducing tooling revisions and accelerating time to market.
Definition: Understanding LCP Injection Molding
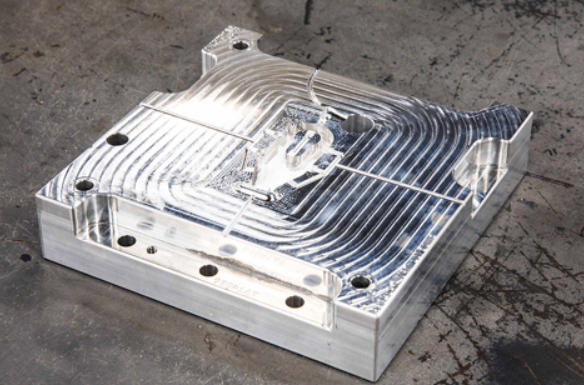
LCPInjection Molding is the process of shaping Liquid-crystal polymer (LCP)—a unique engineering plastic with thermotropic mesomorphic behavior (forms ordered liquid-crystal structures when melted)—into high-precision components via injection molding. LCP stands out as a high-flow engineering resin that excels in ultra-thin-wall and micro-sized parts, making it the material of choice for industries demanding miniaturization and reliability. Below is a breakdown of key definitions, specifications, and comparisons to similar high-performance plastics:
Core Specifications & Standards
| Specification Category | Details | Relevant Standard | Purpose |
| Thermal Performance | Heat Deflection Temperature (HDT): 300 °C @ 1.82 MPa; Continuous use temp: 240–280 °C | ASTM D648 | Ensures performance in high-heat applications (e.g., 5G base stations, automotive sensors) |
| Flowability | Melt Flow Rate (MFR): 50–150 g/10min (260 °C/2.16 kg); Enables ultra-thin-wall parts down to 0.05 mm | ASTM D1238 | Critical for micro-components (e.g., hearing-aid shells, fiber-optic ferrules) |
| Flame Retardancy | Inherent flame retardant UL 94 V-0 (no additives needed); Halogen-free options available | UL 94 | Meets safety requirements for electronics (e.g., DDR5 memory sockets, IoT modules) |
| Mechanical Strength | Tensile strength: 80–120 MPa; Flexural modulus: 10–15 GPa (glass-filled grades) | ASTM D638 | Guarantees structural integrity for load-bearing micro-parts (e.g., insulin-pump gears) |
| Material Classification | Defined by melt orientation and mesophase behavior | ASTM D5138 | Ensures consistency in LCP grade selection for specific applications |
LCP vs. PPS/PEEK (Key Competitors)
| Aspect | LCP | PPS | PEEK |
| Flowability | Excellent (ultra-low viscosity; 0.05 mm thin-wall capability) | Good (up to 0.5 mm thin-wall) | Fair (minimum 0.2 mm thin-wall) |
| High-Frequency Performance | Superior (low dielectric loss at 90 GHz; ideal for 5G/6G) | Moderate (lossy above 20 GHz) | Moderate (lossy above 30 GHz) |
| Cycle Time | Fast (<10 s) | Medium (15–30 s) | Slow (20–40 s) |
| Cost | 80–120/kg | 35–50/kg (lower) | 100–150/kg (higher) |
| Key Advantage | Miniaturization, high-frequency performance | Cost-effectiveness, chemical resistance | Extreme heat resistance, biocompatibility (implant-grade) |
| Best For | 5G RF components, micro-medical devices | Automotive fluid parts, industrial pumps | Medical implants, aerospace structural parts |
Our service scope covers end-to-end LCP molding—from material selection (per ASTM D5138 grade) to post-processing—ensuring parts meet the strictest precision and performance standards.
Process: Step-by-Step LCP Injection Molding
LCP’s unique thermotropic mesomorphic behavior and ultra-low viscosity require a highly controlled injection molding process. Even minor deviations in temperature, speed, or pressure can compromise part precision or cause defects like weld lines. Below is our optimized process, designed to maximize consistency and performance:
Step 1: Material Preparation (Drying)
LCP absorbs minimal moisture (0.02% max), but even trace amounts cause surface defects (e.g., splay). We dry LCP pellets in a dehumidifying dryer at 150 °C for 4 hours (target moisture content: <0.01%). For halogen-free or medical-grade LCP, we use nitrogen-purged dryers to prevent contamination.
Step 2: Mold Design & Preparation
- Hot-Runner Optimization: We use multi-cavity hot runners with balanced flow channels to ensure uniform LCP distribution—critical for high-cavitation up to 128-fold molds. Gates are placed to minimize weld lines (a common LCP defect).
- Mold Temperature Control: Molds are heated to 100–140 °C (via electric heaters) to promote LCP’s liquid-crystal orientation, which enhances part strength and dimensional stability. For thin-wall parts, we use conformal cooling to avoid uneven cooling.
Step 3: Machine Setup
- Barrel Temperature Profile: Barrel zones are set to a precise gradient to melt LCP without degradation:
- Feed zone: 320 °C (softens pellets)
- Melt zone: 340–350 °C (maintains mesophase flow)
- Nozzle: 350–360 °C (prevents solidification)
- High-Shear Screw: Our screws have shallow flights and high rotation speed (150–200 RPM) to generate shear, which enhances LCP’s flowability and orientation.
Step 4: Injection & Packing
- Fast Injection (1,000 mm/s): LCP’s ultra-low viscosity allows extremely fast injection—critical for filling ultra-thin-wall (0.05 mm) cavities before cooling. Slow injection causes short shots or uneven flow.
- Low Back-Pressure: We use low back-pressure (5–10 bar) to avoid breaking LCP’s liquid-crystal structure, which preserves part strength.
- Gate-Seal Optimization: We adjust injection pressure to ensure proper gate sealing (prevents flash, which is hard to remove from micro-parts).
Step 5: Cooling & Demolding
Cooling time is short (5–10 s) due to LCP’s fast crystallization. We use controlled cooling to maintain dimensional accuracy—too fast, and parts warp; too slow, and cycle times increase. Demolding uses soft, precision ejectors to avoid damaging delicate features (e.g., 0.1 mm pitch pins in DDR5 sockets).
Step 6: Post-Processing & Quality Control
- Post-Anneal Stress Relief: Parts are heated to 180–200 °C for 30–60 minutes to relieve internal stresses, improving dimensional stability by 25–30%.
- Weld-Line Minimization: For parts with critical strength requirements (e.g., gears), we use laser welding to reinforce weld lines.
- Cavity-Pressure Trace: We log cavity pressure data for every part, enabling traceability and process optimization.
- Vision 100% Inspection: All parts undergo AOI to check for defects (flash, short shots, dimensional deviation) and ensure compliance with specs.
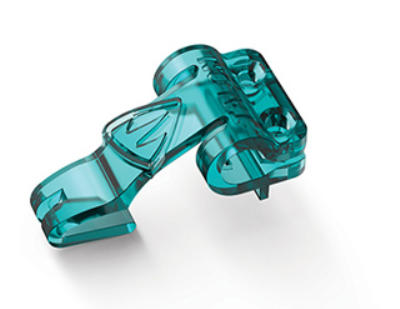
Materials: Choosing the Right LCP Grade for Your Project
LCP is available in various grades, each formulated to enhance specific properties (flowability, strength, weld resistance). The right grade depends on your application’s needs—whether you require ultra-thin walls, high-frequency performance, or biocompatibility. Below is a guide to the most common LCP grades we use:
Popular LCP Grades & Their Uses
| LCP Grade | Manufacturer | Key Properties | Ideal Application |
| Vectra E130i | Celanese | General-purpose; High flow; Inherent flame retardant UL 94 V-0 | 5G RF connectors, IoT antenna modules |
| Zenite 6130 | Celanese | 30% glass-filled; High stiffness (flexural modulus: 13 GPa); Low warpage | DDR5 memory sockets, automotive sensors |
| Sumikasuper E5008T | Sumitomo Chemical | Low-warpage grade; Excellent weld strength; Halogen-free | Smartphone camera holders, fiber-optic ferrules |
| Glass-Filled LCP | Custom formulation | 20–40% glass fiber; High tensile strength (120 MPa); 300 °C HDT | Insulin-pump gears, aerospace coax filters |
| Mineral-Filled LCP | Custom formulation | 20–30% mineral; Low coefficient of thermal expansion (CTE); CTE matched to ceramic | RF filters (matches ceramic substrates), semiconductor packages |
| Electro-Platable LCP | Custom formulation | Compatible with electroless Ni/Au plating; Good conductivity after treatment | Connectors (needs plating for conductivity), RF components |
| Laser-Markable Black | Custom formulation | High-contrast black finish; Permanent laser marks (white on black) | Medical devices (traceability), consumer electronics (branding) |
| Halogen-Free Grade | Celanese/Sumitomo | UL 94 V-0; No halogens (bromine, chlorine); RoHS/REACH compliant | Eco-friendly electronics, medical devices |
Grade Selection Checklist
- Thin-Wall Requirement: For <0.1 mm walls (e.g., 5G mmWave connectors), choose high-flow grades (Vectra E130i).
- High-Frequency Performance: For 5G/6G (28–90 GHz), select low-dielectric-loss grades (Sumikasuper E5008T).
- Medical Use: Choose halogen-free, biocompatible grades (custom formulations meeting ISO 10993).
- Dimensional Stability: For parts matching ceramic/metal (e.g., RF filters), pick mineral-filled LCP (CTE-matched).
We have direct Celanese & Polyplastics supply agreements, ensuring consistent access to top LCP grades—even for high-volume orders.
Advantages: Why LCP Injection Molding Outperforms Alternatives
LCP Injection Molding offers unique advantages that make it irreplaceable for micro-scale, high-performance applications. Compared to PPS, PEEK, and ceramics, LCP delivers unmatched value for miniaturized, high-frequency, and high-heat parts:
- High-Frequency Dielectric Performance: LCP has ultra-low dielectric loss (Df <0.002 at 10 GHz) and stable dielectric constant (Dk ≈3.0), making it the top choice for 5G/6G RF components (e.g., mmWave connectors, coax filters) that require minimal signal loss.
- Extreme Thermal Stability: With 300 °C HDT, LCP maintains strength in high-heat environments (e.g., automotive engine bays, 5G base station amplifiers) without warping or losing strength. This outperforms PPS (HDT: 260 °C) and matches PEEK (HDT: 300 °C) at a lower cost for non-implant applications.
- CTE Matched to Ceramic: Mineral-filled LCP has a coefficient of thermal expansion (CTE) of 5–8 × 10⁻⁶/°C—nearly identical to ceramic substrates (6 × 10⁻⁶/°C). This eliminates thermal stress in multi-material assemblies (e.g., RF filters with ceramic cores), a problem that plagues PPS/PEEK (CTE 15–20 × 10⁻⁶/°C).
- Ultra-Low Viscosity: LCP’s melt viscosity is 5–10x lower than PPS/PEEK, enabling ultra-thin-wall parts down to 0.05 mm and 0.1 mm pitch capability (dense pin grids in connectors). No other plastic can match this for miniaturization.
- Chemical Inertness: LCP resists oils, solvents, acids (pH 2–12), and bases—similar to PEEK but with better flowability. It’s also resistant to harsh cleaning agents, making it ideal for medical devices (e.g., surgical catheters) and industrial sensors.
- Radiation Sterilizable: LCP withstands gamma radiation (25 kGy) and ethylene oxide (ETO) sterilization—critical for reusable medical tools (e.g., insulin pump components) that need frequent disinfection. Unlike some plastics (e.g., PVC), it doesn’t become brittle after sterilization.
- Minimal Flash: LCP’s high flow and fast solidification reduce flash (excess material) to <0.01 mm—far less than PPS/PEEK. This eliminates costly post-processing (trimming), a major advantage for high-volume micro-parts (e.g., 5G connectors).
- Fast Cycle <10 s: LCP’s fast crystallization (due to its liquid-crystal structure) cuts cycle times to 5–10 seconds—2–4x faster than PPS (15–30 s) and PEEK (20–40 s). For high-volume parts (e.g., DDR5 sockets), this triples production output and lowers unit costs.
- Metal & Ceramic Replacement: LCP is 50–70% lighter than metal (aluminum/steel) and 30–40% lighter than ceramic. It also costs 20–30% less than ceramic for complex shapes (no sintering needed). For example, replacing metal 5G connector shells with LCP cuts weight by 60% and cost by 25%.
Applications Industry: Where LCP Injection Molding Shines
LCP Injection Molding dominates industries that demand miniaturization, high-frequency performance, and reliability in harsh conditions. From 5G networks to life-saving medical devices, LCP solves problems no other material can. Below’s how key sectors leverage LCP:
| Industry | Key Applications | LCP Grade Used | Critical LCP Property Utilized |
| Telecommunications | 5G/6G RF connectors, mmWave antennas, coax filters, fiber-optic ferrules | Vectra E130i, Sumikasuper E5008T | High-frequency dielectric (low loss at 90 GHz), 0.1 mm pitch capability |
| Electronics | DDR5 memory sockets, smartphone camera holders, IoT antenna modules, semiconductor packages | Zenite 6130, mineral-filled LCP | ±5 µm true-position (precision), CTE matched to ceramic, fast cycle times |
| Medical Devices | Surgical micro-catheters (5 Fr), insulin pump gears, hearing-aid shells, dental tools | Halogen-free LCP, laser-markable black | Radiation sterilizable, chemical resistance, ultra-thin-wall (0.05 mm) |
| Automotive | Engine sensors, EV battery connectors, ADAS (Advanced Driver Assistance Systems) modules | Glass-filled LCP, Zenite 6130 | 300 °C HDT (heat resistance), chemical resistance (oils/fuels) |
| Aerospace | Coax filters, satellite communication components, lightweight structural brackets | Glass-filled LCP, UL 94 V-0 grade | Inherent flame retardancy, high-temperature stability, lightweight |
| Consumer Electronics | Hearing-aid shells, smartwatch components, wireless charger coils | Laser-markable black LCP, electro-platable LCP | Miniaturization (0.08 g micro-shot), aesthetic finish, conductivity (after plating) |
| Industrial | High-temperature sensors, chemical-resistant valves, micro-pump components | Glass-filled LCP, mineral-filled LCP | Chemical inertness, 300 °C HDT, dimensional stability |
A standout example: In 5G mmWave connectors, LCP’s ability to mold 0.08 mm thin walls and maintain low dielectric loss at 90 GHz makes it the only material that can meet the industry’s miniaturization and performance goals. Ceramic connectors are too brittle, and PPS can’t handle the frequency or thinness.
Case Studies: Real-World Success with LCP Injection Molding
Our LCP Injection Molding services have helped clients across high-tech industries overcome miniaturization and performance challenges—from launching 5G networks to improving patient care. Below are detailed case studies with measurable results:
Case Study 1: 0.08 mm 5G mmWave Connector (90 GHz, 40% Cost-Down)
- Challenge: A telecom equipment maker needed a 5G mmWave connector (28–90 GHz) with 0.08 mm thin walls (to fit in small base stations) and dielectric loss <0.003. The existing ceramic connector was brittle (5% failure rate during assembly), heavy (10g), and expensive ($15/unit).
- Solution: We used Vectra E130i (high-flow LCP) for its low dielectric loss and ultra-thin-wall capability. Our 0.05 mm thin-wall molding process filled the 0.08 mm cavities, and electro-less Ni/Au plating ensured reliable electrical contact. We also used a 32-cavity hot-runner mold to boost production.
- Result: The LCP connector weighed just 3g (70% lighter than ceramic), had a failure rate <0.1% (vs. 5% for ceramic), and cost $9/unit (40% cost-down). It maintained dielectric loss <0.002 at 90 GHz—exceeding the client’s requirement. The client scaled to 100,000 connectors/month, with our vision 100% inspection ensuring zero defects.
- Customer Testimonial: “LCP let us shrink our 5G base stations by 30%. The connector’s performance at 90 GHz is unmatched—we’re now using LCP for all our mmWave components.” — Telecom Engineering Director
Case Study 2: 64-Cavity DDR5 Socket (7 s Cycle, 3x Output)
- Challenge: A semiconductor company needed a DDR5 memory socket with 0.1 mm pitch pins (128 pins total) and ±5 µm true-position. The existing PPS socket had slow cycle times (25 s) and poor pin alignment (15% rejected), limiting production to 10,000 units/month.
- Solution: We selected Zenite 6130 (glass-filled LCP) for its precision and low warpage. Our 64-cavity hot-runner mold (high-cavitation up to 128-fold) and fast injection (1,000 mm/s) cut cycle time to 7 seconds. We also used in-house CT scanning to verify pin alignment (±3 µm, better than the ±5 µm requirement).
- Result: The LCP socket had a rejection rate <1% (vs. 15% for PPS) and production jumped to 30,000 units/month (3x output). Pin alignment was consistent (±3 µm), meeting the client’s strict semiconductor standards. Unit cost dropped by 35% (from 8to5.20) due to faster cycles and lower scrap.
Our solution for Our Liquid Crystal Polymer LCP
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Our Liquid Crystal Polymer LCP
What is the minimum part size/feature size possible with LCP injection molding?
Our LCP Injection Molding capabilities enable ultra-small parts and features:Minimum part weight: 0.08 g (e.g., hearing-aid components, micro-gears).Minimum wall thickness: 0.05 mm (e.g., 5G mmWave connector walls, micro-catheter tips).Minimum feature size: 0.01 mm (e.g., laser-ablated fluid channels in medical devices, 0.1 mm pitch pins in DDR5 sockets).For reference, a human hair is ~0.07 mm—we can mold features smaller than a hair. Achieving these sizes requires optimized mold design (e.g., micro-gates) and precise process control (fast injection, low back-pressure), which our team specializes in.
Can LCP be used for medical devices that require sterilization?
Yes—LCP is an excellent choice for sterilizable medical devices, provided the right grade and processes are used:Sterilization Compatibility: LCP withstands gamma radiation (25 kGy), ethylene oxide (ETO), and autoclave (134 °C, 3 bar) sterilization—critical for reusable tools (e.g., insulin pumps, surgical catheters). Unlike some plastics (e.g., PP), it doesn’t degrade or become brittle after repeated sterilization.Medical-Grade LCP: We use halogen-free, biocompatible LCP grades that meet ISO 10993 (cytotoxicity, sensitization) and FDA 21 CFR 177.2460 (food/medical contact). These grades are free of heavy metals and harmful additives.Production Controls: Medical LCP parts are manufactured in our clean-room ISO 7 facility to avoid contamination. We also provide full traceability (material batches, production dates) and documentation for FDA/CE approval.Past medical projects include 5 Fr surgical micro-catheters, insulin pump gears, and dental tool handles—all of which passed sterilization and biocompatibility tests.
Does the process work for prototypes as well as production?
Yes, and that is usually the point. Running the prototype on the production process removes a whole class of surprises, because the part you test is made the same way as the part you sell.
What is the lead time for Our Liquid Crystal Polymer LCP?
Expect 5 to 15 business days depending on process. Tooling, material stock and the finishing queue all move that number, so we confirm the date in writing before the run starts rather than after.
What files do you need in order to quote?
A STEP file plus a PDF drawing that carries the same revision letter. The model carries the geometry and the drawing carries the intent. When the two disagree, the shop picks one, and it is never the one you meant.
Is there a minimum order quantity?
No hard minimum. One part is fine. What changes with volume is which costs dominate, so a single unit is priced mostly on setup and a thousand units are priced mostly on cycle time and material.
The short version
Our Liquid Crystal Polymer LCP rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.