
Blogs
Our POM Vacuum Casting Services
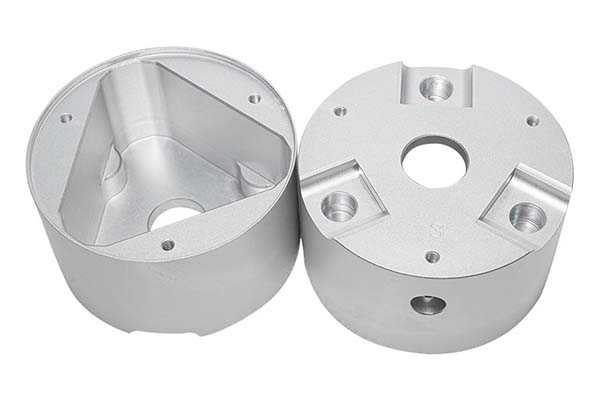
Our POM Vacuum Casting Services, explained the way we would explain it across a table: what it is good at, what it costs you, and the details that keep the part out of the scrap bin.
Key takeaways
- POM Vacuum Castingcombines precision and efficiency to deliver high-quality, durable components for diverse industries.
- At our shop, our capabilities in POM Vacuum Casting are backed by years of experience and a team of skilled engineers.
- POM Vacuum Casting, also known as Polyoxymethylene Vacuum Casting, is a specialized manufacturing process designed to produce high-precision parts using POM (a thermoplastic polymer with excellent mechanical properties).
- The POM Vacuum Casting process follows a structured procedure with clear steps, a defined workflow, and a logical sequence of operations to ensure consistency.
Our POM Vacuum Casting Services
POM Vacuum Castingcombines precision and efficiency to deliver high-quality, durable components for diverse industries.
Whether you need tight-tolerance parts, custom surface finishes, or cost-effective prototyping, our expertise in POM Vacuum Castingensures your projects meet the highest standards—turning your ideas into reliable, production-ready products with speed and accuracy.

Our Capabilities in POM Vacuum Casting
At our shop, our capabilities in POM Vacuum Casting are backed by years of experience and a team of skilled engineers. We bring unmatched expertise, skills, competence, and proficiency to every project, ensuring we meet and exceed client expectations. Our abilities extend across various stages, from design optimization to final production.
Table 2 highlights our key capabilities and how they benefit your projects:
| Capability | Description | Client Benefit |
| Design for Manufacturability (DFM) | Optimize part designs to fit POM Vacuum Casting processes | Reduces production time and costs; improves part performance |
| Material Selection | Advise on POM grades (e.g., homopolymer vs. copolymer) for specific needs | Ensures parts match required mechanical properties (strength, flexibility) |
| Quality Control | In-line inspections using advanced measurement tools (e.g., CMM) | Guarantees parts meet tight tolerances and industry standards |
| Customization | Adapt processes for unique part geometries or surface finishes | Delivers tailor-made solutions for niche applications |
What is POM Vacuum Casting?
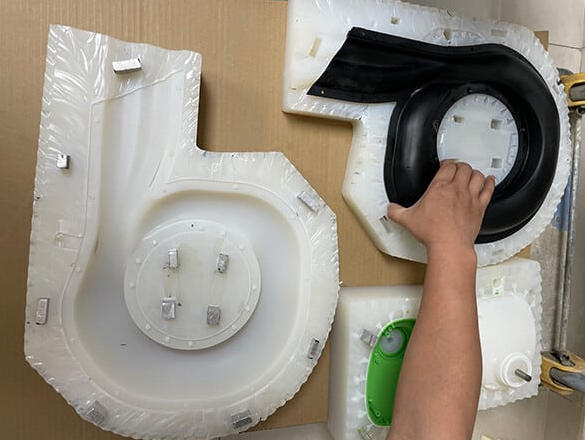
POM Vacuum Casting, also known as Polyoxymethylene Vacuum Casting, is a specialized manufacturing process designed to produce high-precision parts using POM (a thermoplastic polymer with excellent mechanical properties). This section breaks down its definition, meaning, concept, and provides a clear overview and introduction to how it works.
At its core, the process uses a vacuum to eliminate air bubbles from the molten POM material, ensuring uniform density and minimal defects in the final part. Unlike traditional casting methods, the vacuum environment allows for tighter control over the material flow, making it ideal for parts requiring consistent performance.
Table 1 below summarizes key details of POM Vacuum Casting.
| Aspect | Details |
| Core Concept | Use of vacuum to remove air from molten POM, ensuring high part quality |
| Key Material | POM (Polyoxymethylene) – rigid, low-friction, chemical-resistant polymer |
| Primary Goal | Produce precision parts with tight tolerances and minimal defects |
| Common Use Cases | Prototyping, small-batch production, complex geometric parts |
The POM Vacuum Casting Process
The POM Vacuum Casting process follows a structured procedure with clear steps, a defined workflow, and a logical sequence of operations to ensure consistency. Below is a step-by-step breakdown of the process, along with a workflow diagram description.
Step 1: Mold Preparation
First, a mold (typically made of silicone or metal for durability) is cleaned and prepped. The mold cavity is designed to match the final part’s geometry, with vents to allow air escape during the vacuum phase.
Step 2: Material Melting
POM pellets are heated to their melting point (160–175°C for most grades) in an extruder. The molten POM is then transferred to a holding chamber, where its temperature is maintained for optimal flow.
Step 3: Vacuum Application
The mold is placed in a vacuum chamber, and air is removed (vacuum level: 0.02–0.05 MPa). This step is critical to prevent air bubbles from forming in the molten POM, which would weaken the final part.
Step 4: Casting and Cooling
Molten POM is injected into the vacuum-sealed mold under low pressure. The mold is then cooled (using water or air) to solidify the POM. Cooling time varies by part thickness (typically 5–15 minutes).
Step 5: Demolding and Post-Processing
Once cooled, the mold is opened, and the part is removed. Post-processing steps (e.g., trimming excess material, surface treatment) are performed to meet final specifications.
Table 3 summarizes the process timeline for a standard POM part (50mm x 30mm x 5mm):
| Process Step | Time Required |
| Mold Preparation | 10–15 minutes |
| Material Melting | 5–8 minutes |
| Vacuum Application & Casting | 3–5 minutes |
| Cooling | 8–12 minutes |
| Demolding & Post-Processing | 10–15 minutes |
| Total Cycle Time | 36–55 minutes |
Materials Used in POM Vacuum Casting
POM Vacuum Casting relies on high-quality materials, including POM polymers and additional substances or components to enhance part properties. Understanding the raw materials (such as POM grades) and how they interact with other polymers, composites, or alloys is key to achieving desired part performance.
Primary Material: POM
POM (Polyoxymethylene) is a thermoplastic known for its high stiffness, low friction, and excellent dimensional stability. Two common grades used in vacuum casting are:
- POM Homopolymer: Higher tensile strength and heat resistance (suitable for high-stress parts).
- POM Copolymer: Better impact resistance and chemical stability (ideal for parts exposed to oils or solvents).
Secondary Materials
To improve specific properties, we may add:
- Reinforcements: Glass fibers or carbon fibers (increase strength and rigidity).
- Additives: UV stabilizers (prevent degradation from sunlight) or lubricants (reduce friction).
- Composites/Alloys: Blends with other polymers (e.g., nylon) for enhanced flexibility.
Table 4 compares the properties of common POM grades used in our processes:
| POM Grade | Tensile Strength (MPa) | Impact Strength (kJ/m²) | Heat Resistance (°C) | Ideal Application |
| POM Homopolymer (Delrin 100) | 60–65 | 5–7 | 100–110 | Gear components, fasteners |
| POM Copolymer (Celcon M90) | 50–55 | 8–10 | 90–100 | Medical devices, automotive parts |
| Glass-Filled POM (30% glass) | 85–90 | 4–6 | 110–120 | Structural brackets |
Advantages of POM Vacuum Casting
POM Vacuum Casting offers numerous advantages and benefits over other manufacturing methods. Its pros and merits make it a top choice for many industries, with positive aspects that add significant value to your projects.
Key Advantages:
- High Precision: The vacuum environment eliminates air bubbles, resulting in parts with tight tolerances and consistent dimensions.
- Cost-Effective for Small Batches: Unlike injection molding (which requires expensive tooling), vacuum casting uses low-cost molds, making it ideal for prototyping or small-batch production (10–1,000 parts).
- Material Versatility: Works with various POM grades and additives, allowing customization of part properties (strength, flexibility, heat resistance).
- Fast Turnaround: Shorter cycle times (as shown in Table 3) compared to traditional casting, enabling quick iteration and faster time-to-market.
- Complex Geometries: Can produce parts with undercuts, thin walls, or intricate details that are difficult to achieve with machining.
Table 7 compares POM Vacuum Casting to other manufacturing methods:
| Method | Cost (Small Batch) | Precision | Lead Time | Ideal for Complex Geometries? |
| POM Vacuum Casting | Low | High | Short | Yes |
| Injection Molding | High (tooling) | High | Long | Yes |
| Machining | Medium | High | Medium | No (limited by tool access) |
| 3D Printing | Medium | Medium | Short | Yes |
Applications of POM Vacuum Casting by Industry
POM Vacuum Casting has wide-ranging applications across various industries, sectors, markets, and fields. Its versatility and precision make it suitable for diverse uses and segments, from automotive to medical.
Table 8 highlights key industries and their common POM Vacuum Casting applications:
| Industry | Common Applications | Required Properties |
| Automotive | Gearshift components, sensor housings, interior trim parts | Wear resistance, chemical stability (oils/solvents) |
| Medical | Surgical instrument handles, diagnostic device parts | Biocompatibility, easy cleaning |
| Electronics | Connector housings, switch components, cable management parts | Dimensional stability, electrical insulation |
| Consumer Goods | Toy parts, appliance knobs, zipper components | Durability, low friction, aesthetic finish |
| Aerospace | Small structural parts, valve components (non-critical systems) | High strength, heat resistance |
For example, in the automotive industry, we produced 500 POM sensor housings for a leading manufacturer, achieving a tolerance of ±0.03mm and reducing production time by 30% compared to their previous supplier.
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- A model and a drawing that agree
- Material by standard number
- Tolerance only where it mates
- Finish and the faces it applies to
- Quantity and required date
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- process choice
- material
- tolerance band
- finish
- volume
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- A drawing that contradicts the model
- A tolerance with no datum
- A cosmetic callout with no approved sample
- A quote compared against a different scope
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
What to send with the first order
The first order sets the pattern for every order after it. Send a complete package once and the shop files it, and the second order takes a fraction of the time.
- A STEP or native model plus a PDF drawing carrying the same revision letter.
- The material callout by standard number, not by trade name.
- The finish and the exact faces it applies to.
- Any test the part must pass: fit, seal, drop, salt spray, dielectric.
- A contact who can answer a question inside one working day.
Then write down what was agreed. An email that confirms the material, the finish and the date is worth more than a longer purchase order that leaves them open.
Case Studies: Success with POM Vacuum Casting
Our case studies and examples showcase how we’ve used POM Vacuum Casting to solve complex challenges for clients across industries. These projects and success stories (or case histories) highlight real-world applications and implementations of our process.
Case Study 1: Medical Device Handle Production
- Client: A leading medical equipment manufacturer.
- Challenge: Need 200 biocompatible POM handles for surgical instruments, with a matte texture and ±0.04mm tolerance.
- Solution: Used POM copolymer (Celcon M90) for biocompatibility, applied matte texturing via mold patterns, and verified tolerances with CMM.
- Result: Delivered parts in 2 weeks (30% faster than client’s target), with 100% passing biocompatibility tests. The client later expanded the order to 1,000 parts.
Case Study 2: Automotive Sensor Housing
- Client: A global automotive supplier.
- Challenge: Replace 3D-printed sensor housings with production-ready parts that can withstand engine heat (up to 100°C) and oil exposure.
- Solution: Used glass-filled POM (30% glass) for heat resistance, nickel-plated surfaces for corrosion protection, and vacuum casting to ensure no air bubbles (critical for sensor performance).
- Result: Housings met all performance requirements, with a 50% reduction in cost per part compared to 3D printing. The client now uses our process for all their sensor housing production.
Our solution for Our POM Vacuum Casting Services
YiguProto runs custom manufacturing in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our custom manufacturing. You can also talk to an engineer before you commit to a drawing.
FAQ about Our POM Vacuum Casting Services
What is the maximum part size that can be produced with POM Vacuum Casting?
The maximum part size depends on the capacity of our vacuum chambers and mold dimensions. Currently, we can produce parts up to 600mm x 400mm x 200mm (length x width x height) for small-batch orders. For larger parts, we offer modular casting solutions—where parts are cast in sections and assembled post-production. If you have a specific part size in mind, our engineering team can assess feasibility and recommend adjustments to ensure quality.
Is POM Vacuum Casting suitable for high-temperature applications?
Yes, but it depends on the POM grade and any additional reinforcements used. Standard POM homopolymer can withstand continuous temperatures up to 100–110°C, while glass-filled POM (30% glass) can handle up to 110–120°C. For applications requiring higher heat resistance (e.g., up to 150°C), we can incorporate heat-stabilizing additives or blend POM with high-temperature polymers (e.g., PPS). It’s important to share your application’s temperature requirements during the design phase, so we can select the optimal material combination.
How does the cost of POM Vacuum Casting compare to injection molding for small-batch production?
For small-batch production (typically 10–1,000 parts), POM Vacuum Casting is significantly more cost-effective than injection molding. Injection molding requires expensive metal tooling (costing 5,000–20,000 or more), which is only economical for large volumes (10,000+ parts). In contrast, POM Vacuum Casting uses low-cost silicone molds (costing 500–2,000) that can be produced in 3–5 days. For example, producing 500 POM sensor housings via vacuum casting would cost approximately 15–25 per part, while injection molding would cost 5–10 per part—but with an upfront tooling cost of $8,000, making it impractical for small batches.
What tolerance can you hold on Our POM Vacuum Casting Services?
The working default is ±0.1 mm as a working default. Tighter than that the process changes and so does the price, because every step tighter adds inspection time. Call out only the faces that mate with something else and leave the rest on the general tolerance.
What happens if a part is out of specification?
We measure it against the same drawing you approved and, if it misses, we make it again. What matters is that the report exists, because a disagreement without data is just an opinion.
How long does a first article take?
Usually a few business days once the drawing is frozen, and longer if tooling is involved. The date we give you is the date we confirm in writing, not the date we hope for.
The short version
Our POM Vacuum Casting Services rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.