
Die Casting
What Are the Key Stages of a High-Quality Die Casting Process?
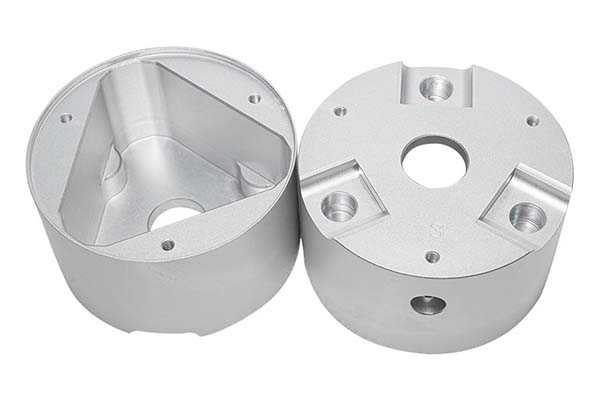
If you want consistent, high-quality die cast parts, you need more than just good equipment. You need a process—a sequence of controlled stages that turns molten metal into precision components. Skip a step, rush a parameter, or ignore a quality check, and defects appear. Porosity. Cold shuts. Shrinkage. Scrap.
Key takeaways
- The die casting process follows a linear workflow with five interconnected stages. Each builds on the last.
- Even with good controls, problems happen. Here is how to identify and fix them.
- The part: Aluminum A380 engine mounting bracket. Requirements: tensile ≥240 MPa, no porosity at mounting holes, 100,000 parts/year.
- What is the difference between high-pressure and low-pressure die casting?
What Are the Core Stages of the Die Casting Process?
The die casting process follows a linear workflow with five interconnected stages. Each builds on the last.
Stage 1: Mold Preparation
The mold is the blueprint. Get this stage wrong, and nothing else matters.
Mold design:
- Parting surface alignment: offset under 0.02mm
- Main sprue diameter: 8–15mm (based on part size)
- Overflow groove volume: 5–10% of cavity volume
- Exhaust groove depth: 0.05–0.1mm
- Draft angle: 1–3° for easy demolding
- Flow simulation: ensure filling in 0.05–0.2 seconds
Mold material: H13 hot-work mold steel, quenched to HRC 48–52, tempered at 550–600°C. This withstands 100,000+ cycles and resists heat fatigue.
Installation and debugging:
- Mount mold with parallelism error under 0.05mm/m
- Test ejection mechanism: push rod stroke accuracy ±0.1mm
- Preheat mold: 150–250°C for aluminum, 100–180°C for zinc
Why it matters: Proper preheating reduces metal temperature loss during filling. Good alignment prevents flash and part distortion.
Stage 2: Molten Metal Preparation
Poor metal quality ruins even the best mold. This stage controls purity and fluidity.
Melting:
- Aluminum alloys: 670–720°C
- Zinc alloys: 400–450°C
- Magnesium alloys: 650–700°C (with inert gas protection)
Refining and degassing:
- Add refining agent (e.g., hexachloroethane for aluminum)
- Stir with argon gas: 10–15 minutes at 5–10 L/min
- Target: impurities under 0.1%; gas content under 0.15 mL/100g metal
Quality monitoring:
- Real-time temperature tracking (accuracy ±2°C)
- Spectrometer analysis for composition (e.g., Si content 7.5–9.5% for A380 aluminum)
Why it matters: Overheating burns alloying elements. Underheating reduces fluidity. Gas in the metal becomes porosity in the part.
Stage 3: Injection Filling
This is the heart of die casting. High pressure and speed force metal into the mold.
Two-stage injection (industry standard):
| Stage | Purpose | Parameters | Risks if Wrong |
|---|---|---|---|
| Low-speed | Fill pressure chamber, avoid splashing | 0.1–0.5 m/s; 5–15 MPa | Too fast → air entrapment; Too slow → early solidification |
| High-speed | Fill cavity quickly, form complex features | Aluminum: 2–8 m/s; Zinc: 1–3 m/s; Pressure: 30–70 MPa | Too slow → incomplete fill; Too fast → turbulence, porosity |
Boost and holding:
- After cavity fill, apply boost pressure: 50–100 MPa (higher for thick walls)
- Hold time: 2–10 seconds (add 1 second per 2mm thickness)
- Result: eliminates shrinkage, achieves density ≥98%
Why it matters: The injection profile determines whether metal reaches every corner of the cavity before freezing. Boost pressure compensates for shrinkage as metal solidifies.
Stage 4: Mold Opening and Part Removal
Gentle handling prevents damage to parts that have just solidified.
Mold opening: Start slow (50–100 mm/s) to break initial adhesion, then faster.
Part ejection: Use multiple push rods for large parts to distribute force evenly.
Initial cleaning: Remove gate and runners. For mass production, robotic trimming ensures consistency.
Why it matters: Uneven ejection bends parts. Rough handling scratches surfaces that should be ready for use.
Stage 5: Post-Processing
Raw castings become finished products through these steps.
Trimming: Remove flash and excess material. Robotic deburring achieves ±0.1mm accuracy.
Surface finishing: Sanding, polishing, or blasting as required.
Machining: Drill holes, tap threads, mill mating surfaces if needed.
Surface treatment: Anodizing, painting, or plating for protection and appearance.
Inspection: Final quality check before shipping.
How Do You Control Quality in Each Stage?
Quality is not a final inspection—it is built stage by stage.
| Stage | What to Check | How to Check | Acceptance Criteria |
|---|---|---|---|
| Mold preparation | Mold precision | CMM (coordinate measuring machine) | Cavity tolerance: IT8–IT10 |
| Molten metal | Gas content | Reduced pressure test (RPT) | ≤0.15 mL/100g (aluminum) |
| Injection filling | Process stability | Pressure sensors, data acquisition | Pressure fluctuation <±5%; Speed <±10% |
| Mold opening | Surface quality | Visual + 10× magnifier | No cracks, cold shuts, severe burrs |
| Post-processing | Dimensions, internals, properties | CMM, X-ray, tensile test, hardness | Tolerance ±0.05mm (key features); No porosity (ISO 17636-1 Level 2); Tensile ≥200MPa (A380); Hardness HB 80–100 |
What Common Defects Occur and How Do You Fix Them?
Even with good controls, problems happen. Here is how to identify and fix them.
Porosity (Gas Holes)
What it looks like: Tiny bubbles visible on X-ray or as surface pinholes.
Causes:
- Trapped cavity gas
- High gas content in metal
- Filling speed too fast
Fixes:
- Enlarge exhaust grooves to 0.1–0.15mm depth
- Extend degassing time to 15–20 minutes
- Reduce high-speed filling speed by 10–20%
Shrinkage
What it looks like: Depressions on surface or dark areas on X-ray.
Causes:
- Insufficient boost pressure
- Local cooling too fast
- Holding time too short
Fixes:
- Increase boost pressure to 60–80 MPa
- Add cooling inserts in hot spots
- Extend holding time by 2–3 seconds
Cold Shuts
What it looks like: Linear seams on surface—unfused metal layers.
Causes:
- Metal temperature too low
- Filling speed too slow
- Mold surface cold
Fixes:
- Raise metal temperature 10–20°C
- Increase high-speed filling speed 0.5–1 m/s
- Check mold preheat—eliminate cold spots
Mold Strain (Sticking)
What it looks like: Scratches or material adhesion on part surface.
Causes:
- Rough mold cavity (Ra >0.8μm)
- Failed release agent
- Mold too hot
Fixes:
- Polish cavity to Ra ≤0.4μm
- Switch release agent (water-based for aluminum)
- Lower mold temperature 20–30°C
Cracks
What it looks like: Fine lines on part, especially at fillets.
Causes:
- Fillet radius too small (<1mm)
- Uneven cooling
- Residual stress
Fixes:
- Redesign with fillet radius ≥2mm
- Balance cooling channels (flow difference <10%)
- Add stress relief anneal: 120–180°C for 2–4 hours
Real-World Example: Automotive Bracket
The part: Aluminum A380 engine mounting bracket. Requirements: tensile ≥240 MPa, no porosity at mounting holes, 100,000 parts/year.
Initial problems: 12% scrap from porosity near holes. Cold shuts on thin sections.
The fixes:
Mold:
- Added overflow grooves (8% of volume) at hole locations
- Polished cavity to Ra 0.4μm
- Balanced cooling channels
Process:
- Reduced injection speed: 8 m/s → 4.5 m/s
- Increased mold temperature: 180°C → 210°C
- Extended holding time: 6s → 9s
Quality:
- X-ray sampling every 2 hours
- Spectrometer check every shift
Results:
- Scrap: 12% → 1.5%
- Cycle time unchanged (65 seconds)
- Tensile strength: 265 MPa (exceeds requirement)
- Annual savings: $180,000
How to write a spec that gets priced correctly
A drawing is a contract. If it leaves a number open, the shop fills that number in with its own default. The default is rarely the one you had in mind. Put these five lines on every RFQ and most of the back-and-forth disappears before it starts.
- 3D model with the parting line marked
- Alloy grade and the standard it meets
- Wall thickness and draft on every face
- Machining allowance on the faces that will be cut
- Pressure tightness or porosity class
The point is not paperwork. Each line removes a decision the shop would otherwise make for you. A complete RFQ comes back priced. An incomplete one comes back guessed.
What actually drives the price
Buyers usually push on material because it is the line they can see. In practice the material is rarely the biggest number on a quote. These five lines decide most of it:
- die steel and cavity count
- part weight and wall section
- draft and slide count
- porosity requirement
- machining allowance
Ask for the quote split by line. A supplier who cannot break it down is guessing, and you will pay for the guess. The line you can usually renegotiate is the tolerance band, not the raw material.
Problems you will meet, and the fix
Every process has a failure mode it prefers. The same four show up again and again on this kind of work, and none of them are mysteries once you know what to look for.
- Cold shuts where two flow fronts meet
- Porosity that shows up only after machining
- Soldering on a hot spot in the die
- Shrinkage voids in a heavy section
Catch the fault on the first part, not the hundredth. A first-article check costs an hour. A bad batch costs the whole order. Write the check into the purchase order so nobody has to remember it.
What to check on the first article
The first article is the cheapest inspection you will ever buy. Use it properly and the rest of the run becomes boring, which is exactly what you want.
- Every dimension on the drawing, with the measured value written beside it.
- The material certificate, matched to the heat or lot number on the parts.
- The finish against the sample you approved, under the same light.
- Fit against the mating part, assembled rather than measured.
- Packaging, because parts that arrive damaged were never in tolerance.
Check in this order: datums, then mating features, then cosmetic faces. If the datums are wrong, every number after them is noise. Keep the report on file. When a problem shows up in month six, that document is the only thing that tells you what changed.
How to compare two quotes fairly
Two numbers are not comparable unless the scope matches. Line them up before you decide, because a low number with three gaps is not a low number.
Same drawing, same material, same finish, same inspection. Anything else is a different job wearing the same part number. Then look at what each quote leaves out. Freight, packaging, certificates and tooling are the usual gaps.
Ask each supplier to state their assumptions in writing. The one who does is usually the one who has run the process before.
Scaling from one part to a batch
The first part teaches you the process. The hundredth teaches you the process cost.
Watch three things as volume grows: setup amortisation, tool wear, and how much hand work the finish still needs. If the unit price barely moves between ten and a hundred, the cost sits in material or in hand work, not in setup. Ask which, because only one of them is negotiable.
Lead time behaves the same way. A one-off is scheduled around other jobs. A repeat order is scheduled around your forecast. Give the shop a forecast and the lead time gets shorter, not longer.
How to read a supplier's quote
A quote is a short document with a long shadow. Four things in it decide whether the job runs smoothly, and only one of them is the price.
- The scope line. It should name the process, the material and the finish, not just the part.
- The tolerance basis. General tolerance or the drawing, and which standard it follows.
- The exclusions. Tooling, freight, certificates and inspection are the usual omissions.
- The validity date. Material prices move, and an open-ended quote is a promise nobody can keep.
Read the exclusions before you read the total. A quote that leaves out tooling is not cheaper. It is a quote for a different job.
What to send with the first order
The first order sets the pattern for every order after it. Send a complete package once and the shop files it, and the second order takes a fraction of the time.
- A STEP or native model plus a PDF drawing carrying the same revision letter.
- The material callout by standard number, not by trade name.
- The finish and the exact faces it applies to.
- Any test the part must pass: fit, seal, drop, salt spray, dielectric.
- A contact who can answer a question inside one working day.
Then write down what was agreed. An email that confirms the material, the finish and the date is worth more than a longer purchase order that leaves them open.
FAQ About the Die Casting Process
What is the difference between high-pressure and low-pressure die casting?
High-pressure (30–100 MPa, 2–8 m/s) fills fast—ideal for thin-walled complex parts like phone casings. Low-pressure (0.05–0.2 MPa, gravity-assisted) fills slowly—better for thick-walled high-strength parts like engine cylinder heads, with less porosity.
How long does a die casting mold last?
H13 steel molds typically last 100,000–200,000 cycles. To extend life:
- Clean cavity every 500 cycles
- Monitor mold temperature—avoid overheating
- Apply maintenance oil during downtime
- Repair small scratches promptly (laser cladding)
Can die casting work for steel parts?
No. Steel melts at 1450–1510°C—far above H13 steel’s maximum working temperature (~600°C). Molds would degrade rapidly. Die casting is for non-ferrous alloys (aluminum, zinc, magnesium) with melting points under 800°C. For steel, use forging or sand casting.
How do you check for internal defects?
Three main methods:
- X-ray inspection: Detects internal pores >0.1mm
- Hydrostatic testing: Applies 1.5× working pressure to check for leaks
- Ultrasonic testing: Finds near-surface defects (cold shuts, cracks) with ±0.02mm accuracy
What causes surface blisters?
Trapped gas expands during post-processing heating (painting, welding) or if parts get too hot in service. Causes:
- Excessive injection speed (traps air)
- Poor venting (air can’t escape)
- Moisture in release agent (vaporizes during fill)
Fixes: reduce speed, improve vents, dry release agent.
A high-quality die casting process is a sequence of controlled stages, each with specific parameters and quality checks:
- Mold preparation: Design with proper draft, exhaust, and overflow. Preheat to 150–250°C. Install with <0.05mm/m parallelism.
- Molten metal preparation: Melt at correct temperature (670–720°C for aluminum). Degas to <0.15 mL/100g gas content. Verify composition.
- Injection filling: Two-stage profile—slow (0.1–0.5 m/s) then fast (2–8 m/s). Apply boost pressure (50–100 MPa). Hold for proper solidification.
- Mold opening and removal: Open slowly, eject evenly, remove gently.
- Post-processing: Trim, finish, machine, treat, inspect.
Quality checks at every stage catch problems before they become scrap. Real-time monitoring—pressure sensors, temperature tracking, X-ray sampling—keeps the process in control.
The numbers prove it: one manufacturer cut scrap from 12% to 1.5% and saved $180,000/year by fixing their process, not just their parts.
Master the stages, control the parameters, and the process will deliver consistent, high-quality castings.
Our solution for Key Stages
YiguProto runs die casting in house, from a single prototype to a production batch. We quote the process, the material and the finish as separate lines, so you can see where the money goes instead of arguing with one number.
Send a STEP file or a drawing and you get a DFM report in one to two business days. It flags the features that add cost and the features that will not hold tolerance on the process you picked.
Every order ships with an inspection report on the features you call out. If a part misses, we make it again. Ready to price a part? Start with a free quote and DFM review, or read more about our die casting. You can also talk to an engineer before you commit to a drawing.
FAQ about Key Stages
What material should I specify?
Specify by standard, not by trade name. A trade name can change under you between two orders; a standard number cannot. Then add the one property that actually decides the part, whether that is strength, heat resistance or chemical exposure.
Can Key Stages be made in small quantities?
Yes, and small quantities are where a good supplier earns the next order. Setup dominates the price at low volume, so the cheapest route is usually the one with the fewest operations, not the cheapest material.
How long does a first article take?
Usually a few business days once the drawing is frozen, and longer if tooling is involved. The date we give you is the date we confirm in writing, not the date we hope for.
What tolerance can you hold on Key Stages?
The working default is ±0.1 mm on cast features, ±0.05 mm after machining. Tighter than that the process changes and so does the price, because every step tighter adds inspection time. Call out only the faces that mate with something else and leave the rest on the general tolerance.
What is Key Stages used for?
Key Stages turns up wherever the part has to do a real job at a predictable cost: brackets, housings, fixtures, covers and the fittings that hold them together. The honest test is whether the properties match the load and the environment, not whether the material is fashionable.
What should I check before approving the parts?
Datums first, then the features that mate, then the cosmetic faces. Ask for a dimensional report, a material certificate and a finish sample. A part can be inside every tolerance and still not fit, so assemble one before you sign.
The short version
Key Stages rewards the buyer who reads the data sheet and the drawing together. Pick the option for the property that matters, not for the price per kilo.
Tighten only what mates. Test a sample before the run. Then let the process do the rest.